
治具は剛性が高く再現性があっても、誤った基準からワークを位置決めしてしまうことがあります。CNC治具設計における中心的な問いは「しっかりクランプできるか?」ではなく、「ワークを歪ませたり、切削を妨げたり、検査を妨げたりすることなく、意図した基準を確立できるか?」です。有用な治具計画は、図面の機能基準を位置決め点、クランプ方向、工具アクセス、そして完成した形状をどのように検査するかに結び付けます。.
図面の基準を位置決めロジックに変換する
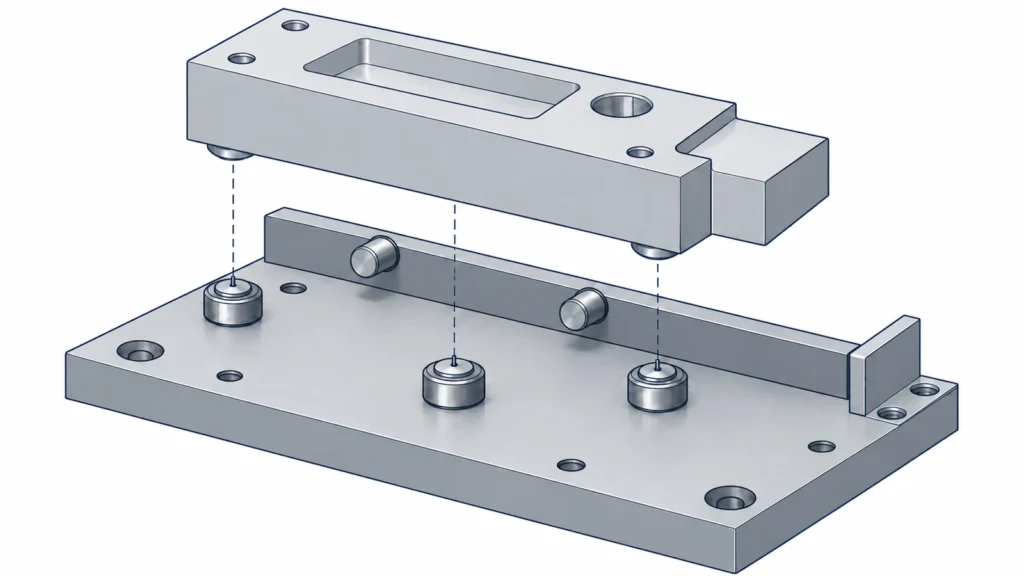
Begin with the surfaces and features that define how the component functions in assembly. A fixture should locate from those references where practical—not from a convenient but unrelated edge that merely makes the part easy to load. If a datum face is unfinished, flexible, or interrupted, determine what alternate locating scheme preserves the required relationship and how that choice will be verified.
For a prismatic part, a 3-2-1 locating concept can help organize contacts: three points establish a primary plane, two constrain a secondary direction, and one completes the location. This is a planning principle, not a universal fixture prescription. Actual contact locations must account for stiffness, surface condition, cutting forces, and the geometry of the specific workpiece.
Round or irregular parts may need a chuck, collet, V-block, profile nest, or a combination of contacts. The important outcome is controlled location with no unintended rocking. If several surfaces compete as references, identify the functional datum hierarchy on the drawing and confirm the sequence with manufacturing before finalizing the fixture.
工程順序を考慮して設計する
治具は工程ルートの一部です。荒加工中は素材を確実に保持し、材料が除去されるにつれて部品を支持し、仕上げパスを干渉なく行えるようにする必要があります。最初の面には優れた段取りでも、クロス穴、サイドポケット、最終検査には不適切な場合があります。部品がどのように旋回または再方向付けされるか、また工程間で共通基準を維持できるかどうかを検討します。.
工具、ホルダ、スピンドルノーズ、プローブのクリアランスを計画します。カッタのクリアランスだけでは不十分です。カッタが壁に届いても、ホルダがクランプや治具本体に衝突する場合があります。該当する場合は切りくず排出とクーラントのためのスペースを確保します。ロケータと部品の間に挟まった切りくずは、位置をずらしたり、仕上げ面を傷つけたりする可能性があります。.
複数の段取りが避けられない場合は、基準移行の方法を定義します。加工基準面、既知のボア、プロービング、または専用ネストを使用できます。順序では、どの形状を最初に確立し、どの後続形状がそれに依存するかを明記する必要があります。工程の概要は次で確認できます: CNC加工プロセスガイド.
ワークを変形させずにクランプする
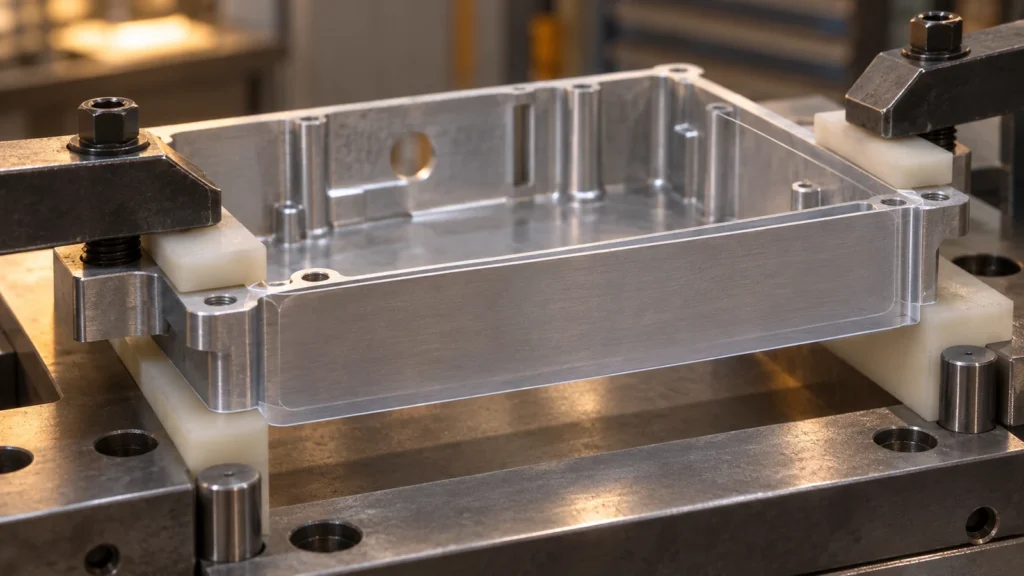
Clamping force must resist cutting loads without bending or crushing the workpiece. Thin walls, long spans, cast or stress-relieved stock, and soft materials are particularly sensitive to load location. If the part is restrained in a deflected condition and then released, the measured geometry can change. Place support near the cutting zone when possible, and distinguish support contacts from locating contacts so that the fixture does not overconstrain the part.
Use broad, stable contact where the surface allows it, but do not assume more contact is always better. A high point, burr, or chip can create a false seat. Clamp sequence matters too: tightening one point fully before the others can pull a part away from its intended datum. Consider controlled stops, equalized clamping, or a sequence that seats the workpiece before applying full force.
For parts with delicate or finished surfaces, specify pads or protective interfaces only when their behavior is understood. A compliant pad can protect a surface but may introduce movement or repeatability variation. The fixture should also make loading orientation obvious; an asymmetric nest or clear orientation feature can prevent an operator from placing the part in a plausible but wrong position.
検証を治具コンセプトに組み込む
段取りを設計している段階で、最初の部品をどのように検査するかを確認します。重要な形状を治具内でプロービングできるか、それとも部品を取り外してCMM上で再確立する必要があるか?治具は検査に必要な基準面を妨げていないか?インプロセス測定を計画している場合は、機械座標系が図面基準とどのように関係するか、またオフセットがどのように制御されるかを定義します。.
治具が自身の位置を再現しても、部品が図面に対して正しく位置決めされていることは証明されません。検証は、治具の位置決め方式を測定可能な部品形状に結び付ける必要があります。生産作業では、計画に初品承認、定期チェック、最終検査報告書を含める場合があります。必要な方法は図面と購入者の受入要件によって異なります。.
設計に厳しい位置またはプロファイルの管理が含まれる場合は、検査方法が実用的で合意されていることを確認します。関連する CNC品質管理の概要 プロセスチェックと最終承認がどのように連携するかについて説明します。.
治具レビューのチェック項目
- 各ロケータはどの図面データムを確立し、何が揺れを防ぎますか?
- 切削力はどこに作用し、その荷重付近で部品はどのように支持されますか?
- カッター、ホルダー、プローブ、切りくずは、すべての必要な領域に到達または通過できますか?
- クランプは薄肉形状を変形させたり、仕上げ面に跡を付けたりしませんか?
- 後続の各セットアップは、以前のデータム関係をどのように回復しますか?
- 基準状態を変えずに主要寸法を検査できますか?
すべての部品に対して複雑な専用治具が必要なわけではありません。同じ要件を満たすのであれば、バイス、チャック、コレット、または標準的な位置決め要素が適切な場合もあります。位置決めの論理が追跡可能であり、計画された工程を通じて部品が安定し、得られた形状を図面に対して検証できるときに、治具設計は成功です。.
よくある質問
より剛性の高い治具は常に精度を向上させますか?
剛性は切削荷重に抵抗するのに役立ちますが、精度は位置決め基準、クランプによる変形、データム転送、機械の状態、検査にも依存します。過剰または不適切に配置された力は精度を低下させる可能性があります。.
治具は図面のデータム面を使用すべきですか?
実用的な場合は、はい。データム面が不適切な場合、代替の位置決め方法は意図された機能関係を維持し、検証可能であるべきです。.
1つの治具で全工程を支えられますか?
場合によっては可能ですが、常にとは限りません。工具のアクセス、部品の向き、クランプ、検査により追加のセットアップが必要になることがあります。単一セットアップを強制するよりも、管理された転送計画の方が重要です。.
治具設計はいつレビューすべきですか?
工程計画の段階で、生産プログラミングが確定する前にレビューしてください。早期のレビューにより、図面や工程順序の変更がまだ現実的であるうちに、アクセス、クランプ、データムに関する問題を明らかにできます。.