
航空機内装、医療用滅菌トレイ、または高周波電子筐体向けの精密部品を調達している場合、おそらく次のような要件に遭遇したことがあるでしょう Ultem machining 重要な能力要件として。SABICがULTEM™というブランド名で開発したこの非晶性熱可塑性樹脂は、熱安定性、機械的強度、電気絶縁性の組み合わせを提供し、他のエンジニアリングプラスチックにはなかなか真似できません。しかし Ultemの加工 は、アセタールやアルミニウムの切削とは異なります。この材料の低い熱伝導率、高い剛性、応力割れへの感受性は、規律あるプロセス制御、専用工具、そして切削力下で異なるグレードがどのように挙動するかについての深い理解を要求します。本ガイドでは、知っておくべきすべてを解説します: Ultemプラスチック とは何か、どのように加工するか Ultem 1000 対 Ultem 2300, 、成功とスクラップを分ける重要なパラメータ、そしてJucheng Precisionのような経験豊富なCNC工場と提携することが、性能を発揮する部品と失敗する部品の違いを生む理由。.
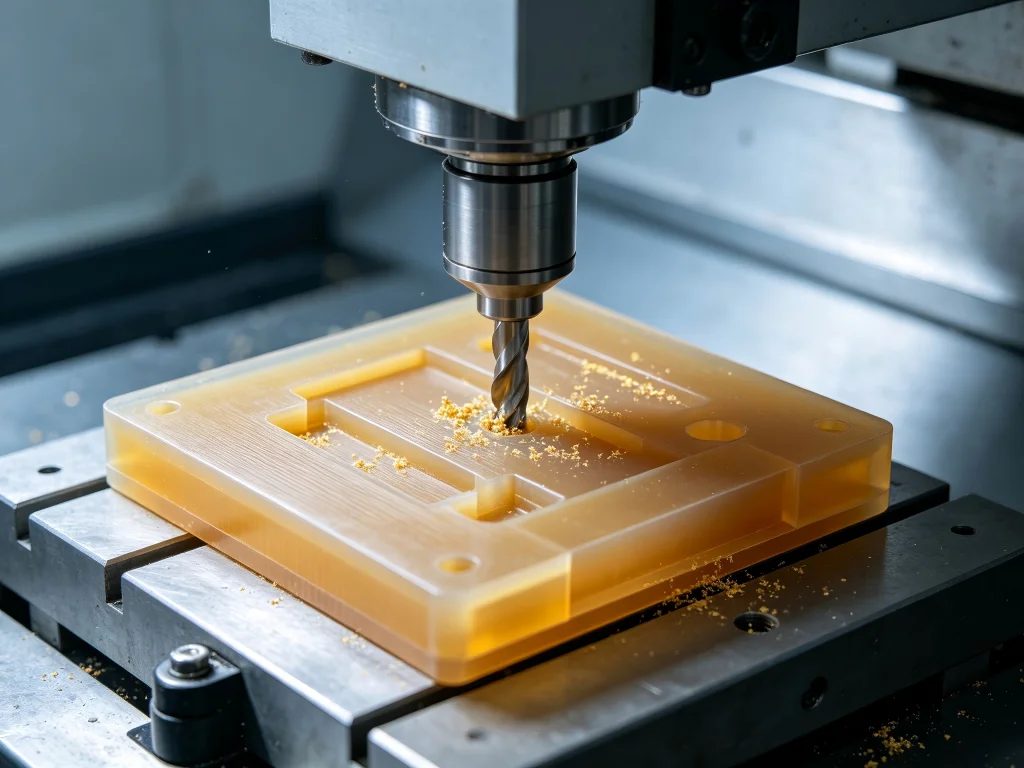
Ultemプラスチックとは?その名の背後にある材料を理解する
Ultemプラスチック はポリエーテルイミド(PEI)のブランド名であり、高性能な非晶性エンジニアリング熱可塑性樹脂です。明確な融点を持つ半結晶性ポリマーとは異なり、Ultemは温度が上昇するにつれて徐々に軟化し、熱劣化を起こさずに効率的に材料除去が行われる狭い加工ウィンドウを生み出します。このユニークな挙動は、217°Cのガラス転移温度(Tg)と170°C~180°Cの連続使用温度定格と相まって、ナイロン、アセタール、ポリカーボネートなどの従来のプラスチックでは失敗する用途に適しています。.
この材料の分子構造—柔軟性と加工性のためのエーテル結合と、耐熱性と機械的耐性のためのイミド基の組み合わせ—は、エンジニアがしばしば「軽量で電気絶縁性のパッケージに金属のような性能」と表現するものを提供します。本質的に難燃性で、化学添加剤なしでUL94 V-0定格を達成し、発煙量も最小限であるため、航空機キャビン内装やその他の防火安全が重要な環境で採用されています。.
Ultemの性能を定義する主要特性
なぜ Ultem CNC加工 がこれほど注意深い対応を必要とするため、材料の基本的な特性を見ることが役立ちます:
- 熱的性能: ガラス転移温度は217°C、連続使用温度は170~180°Cまで。ほとんどのエンジニアリングプラスチックが軟化する温度でも剛性を維持します。.
- 機械的強度: Ultem 1000の引張強度は約105 MPaで、一部の鋳造金属に匹敵します。優れた耐クリープ性により、機械加工部品は連続的な応力下でも厳しい公差を維持します。.
- 電気絶縁性: 絶縁破壊強度は約33 kV/mmで、マイクロ波放射をほぼ透過し、高周波RF部品に最適です。.
- 化学的および加水分解安定性: 自動車用流体、アルコール、水性酸に耐性があります。優れた加水分解安定性により、分子劣化を起こすことなくオートクレーブ滅菌サイクルを繰り返し行えます。.
- 寸法安定性: 低い熱膨張係数と最小限の吸湿性により、部品は温度や湿度の変化にわたって形状を維持します。.
これらの特性は、なぜ Ultem PEI 機械加工 が複数の業界で不可欠となっているかを説明しています。しかし、これらの特性は、この材料が現場で容赦がない理由も説明しています—その高い剛性と低い熱伝導率は、尊重を要する課題を生み出します。.
機械加工の課題:Ultemが異なる理由
経験豊富な機械工は、Ultemの加工を、延性金属というよりも脆いセラミックの加工に近いとしばしば表現します。この材料は、パラメータが正しければきれいに破断する短く脆い切りくずを生成しますが、最適範囲から外れると、粉状のダストの発生、あるいはさらに悪いことに表面の光沢化や溶融が見られます。.
熱管理:最大の敵
Ultemの熱伝導率は極めて低く、約0.22 W/m·Kです。これは、切削中に発生する熱が、バルク材料や切りくずに放散されるのではなく、切れ刃に集中することを意味します。その結果は深刻なものになり得ます:
- Surface glazing and melting that compromises dimensional accuracy
- Tool edge buildup that degrades surface finish
- Thermal stress cracking in thin-walled sections
- Discoloration indicating thermal degradation of the polymer matrix
- Dimensional distortion as residual stresses relax post-machining
The key to successful Ultem machining lies in removing material before heat accumulation reaches critical levels. This requires aggressive chip evacuation, appropriate cutting speeds, and often supplemental cooling strategies that go beyond standard flood coolant application.
Tool Wear and Selection
While unfilled Ultem 1000 is not as abrasive as glass-filled composites, it will still accelerate tool wear when machined incorrectly. Solid carbide tools are mandatory—high-speed steel (HSS) tools blunt too quickly. For machining Ultem 2300, the 30% glass fiber reinforcement makes the material significantly more abrasive, and many shops recommend polycrystalline diamond (PCD)-coated tools to combat rapid tool ablation.
Tool geometry matters as much as tool material. Two- or three-flute end mills provide larger gullets for efficient chip evacuation, preventing chip re-cutting and heat buildup. A higher helix angle—around 45° or more—is preferred because it provides a shearing action that reduces cutting forces.
Ultem 1000 vs. Ultem 2300: Choosing the Right Grade
One of the most common decisions in Ultem CNC加工 projects is whether to specify Ultem 1000 または Ultem 2300. The choice has significant implications for machining strategy, tooling costs, and final part performance.
| 特性 | Ultem 1000 (Unfilled) | Ultem 2300 (30% Glass-Filled) |
|---|---|---|
| 密度 | 1.27 g/cm³ | 1.51 g/cm³ |
| 引張強度 | ~105 MPa | 17,000–20,000 psi (~117–138 MPa) |
| Flexural Modulus | ~3,200 MPa | 850,000–950,000 psi (~5,860–6,550 MPa) |
| 被削性 | Easier; less tool wear; cleaner surface finish | More abrasive; requires specialized tooling; lower speeds |
| 表面仕上げ | Typically smoother, more pristine | May be less smooth due to glass fibers |
| 代表的な用途 | Insulators, housings, brackets,精密几何形状 | High-strength structural components, reusable medical devices |
Ultem 1000 is the unfilled base grade that offers the best balance of machinability and mechanical properties. It produces chips that are easier to control and generally delivers a cleaner surface finish. For parts that require tight dimensional tolerances, complex geometries, or optical-quality surfaces, Ultem 1000 is often the preferred choice.
Ultem 2300, by contrast, offers greater rigidity and improved dimensional stability at elevated temperatures, thanks to its 30% glass fiber reinforcement. However, the glass fibers make the material more abrasive and the chips more challenging to control. Tooling costs are higher, and surface finish may not reach the same level as unfilled grades.
The decision between these grades ultimately comes down to application requirements: if stiffness and strength at temperature are paramount, Ultem 2300 may be the better choice. If machinability, surface finish, and tool life are the primary concerns, Ultem 1000 is hard to beat.
Core Applications: Where Ultem Machining Delivers Value
Ultemプラスチック finds its way into some of the most demanding engineering applications across multiple industries. Understanding these use cases helps clarify why Ultem machining has become such a critical capability.
Aerospace and Aviation
The aerospace industry is perhaps the largest consumer of machined Ultem components. The material’s inherent flame retardance (UL94 V-0), low smoke emissions, and high strength-to-weight ratio make it ideal for aircraft interior components. Specific applications include:
- Cabin interior components that must meet FAR 25.853 flame requirements
- Instrument housings and bracketry that require dimensional stability across temperature extremes
- Electrical connectors and insulators where dielectric performance is critical
- Radome assemblies that must be transparent to microwave radiation
Medical Devices and Healthcare
Ultem’s biocompatibility and ability to withstand repeated autoclave sterilization cycles make it a material of choice for medical applications. The material maintains its properties through harsh sterilization methods that would destroy lesser plastics. Common medical applications include:
- Reusable surgical instruments and handles
- Medical device housings and probe enclosures
- Sterilization trays and containers
- Analytical instrument components
Electronics and Semiconductor
The electrical insulation properties of Ultem—high dielectric strength and stable dielectric loss factor across a broad frequency range—make it a standard material for high-frequency electronic applications. Semiconductor process components, electrical insulators, and connector bodies are typical applications.
自動車
Under-hood automotive applications benefit from Ultem’s heat resistance and dimensional stability. The material performs reliably in the high-temperature environments found in engine compartments and transmission systems.
Critical Selection Factors: What to Look For in an Ultem Machining Partner
すべてのCNC工場が Ultem PEI 機械加工 successfully. The material’s sensitivity to heat, stress, and tool wear means that capability, experience, and process control matter enormously. Here are the key factors to evaluate when selecting a machining partner for your Ultem components.
Tooling Expertise and Inventory
Ultem machining requires specialized tooling—solid carbide end mills with specific geometries, and for glass-filled grades, PCD-coated tools. A shop that understands the difference between machining Ultem 1000 and Ultem 2300, and stocks the appropriate tooling for each, is already ahead of the curve. Ask potential partners about their tool selection protocols for high-performance plastics.
Thermal Management Capabilities
Because heat is the primary enemy in Ultem CNC加工, a shop’s approach to thermal management is critical. This includes everything from cutting speed and feed rate selection to coolant strategy and chip evacuation. Shops that have experience with high-performance polymers will have established protocols for managing heat—aggressive chip evacuation, appropriate cutting speeds, and cooling strategies that go beyond standard flood coolant.
Stress Relief and Annealing Protocols
Ultem is susceptible to environmental stress cracking (ESC) when exposed to certain polar organic solvents, and internal stresses from machining can lead to warping or cracking over time. Experienced shops perform stress-relief annealing—heat treatment cycles both before and after machining—to relieve internal stresses and ensure long-term dimensional stability. For high-precision or large Ultem 1000 parts, stress relief before and after CNC machining may be necessary to reduce warping, cracking, or dimensional changes caused by internal stresses.
Quality Control and Metrology
Aerospace, medical, and semiconductor applications typically require tight tolerances—often in the ±0.01–0.02 mm range. A shop’s quality control capabilities, including CMM (coordinate measuring machine) inspection, optical comparators, and surface profilometers, directly impact whether your parts meet specifications.
材料調達とトレーサビリティ
Ultem is available in sheet, rod, plate, block, and resin forms. The quality of the raw material matters, and shops that source from reputable suppliers and maintain full traceability provide an additional layer of assurance.
Best Practices for Successful Ultem CNC Machining
Whether you are machining Ultem in-house or outsourcing to a specialized shop, understanding the best practices helps you ask the right questions and set appropriate expectations.
Cutting Parameters: Starting Points
For machining Ultem 1000, recommended roughing parameters with carbide tooling are 500–900 SFM with a chip load of 0.004–0.007 inches per tooth for a 1/2-inch end mill. For finishing, 700–1200 SFM with a chip load of 0.002–0.003 inches per tooth. For Ultem 2300, reduce speeds to 350–700 SFM with a chip load of 0.003–0.005 inches per tooth.
These are first-pass starting points. Actual parameters depend on machine rigidity, tool geometry, coolant application, and part geometry. The goal is to remove material efficiently while preventing heat accumulation at the cutting edge.
Tool Geometry and Coatings
End mills with 2 or 3 flutes provide larger chip clearance than 4-flute designs. A helix angle of 45° or more produces a shearing action that reduces cutting forces and heat generation. For glass-filled grades, diamond coatings or PCD tools extend tool life significantly.
Workholding Considerations
Ultem’s relatively low modulus of elasticity compared to metal makes it more susceptible to deformation under clamping pressure. Excessive or poorly distributed clamping force can cause the material to bow or flex, resulting in out-of-tolerance dimensions once the clamps are released. For thin-walled or complex geometries, machining-induced stresses can cause the part to warp after it is cut free from the stock material.
Coolant and Chip Evacuation
Proper chip evacuation is essential to prevent chip re-welding onto the machined surface. While flood coolant is common, some shops use air blast or mist systems to avoid thermal shock that can occur when cold coolant hits a hot cutting zone. The right approach depends on the specific operation, tooling, and part geometry.
Avoiding Sharp Corners
Applying radii to internal corners relieves stress concentrations and reduces tool wear. Sharp internal corners can cause the brittle material to chip or break out, especially when exiting a cut.
Why Jucheng Precision for Ultem Machining
With over a decade of experience in precision manufacturing, Jucheng Precision has built a reputation for handling demanding engineering thermoplastics, including Ultem (PEI). Founded in Shenzhen in 2012, the company operates from an 8,000-square-meter facility with over 190 employees, including 30 highly skilled technical personnel.
The facility houses more than 150 CNC machines, including 25+ Haas and Mazak units covering 3-axis, 4-axis, turning, grinding, wire EDM, and sinker EDM. This extensive equipment base allows Jucheng to handle everything from prototyping through low-volume and high-volume production runs.
For Ultem CNC加工 specifically, Jucheng has developed specialized protocols that address the material’s unique challenges:
- Specialized tooling: Razor-sharp carbide tools with specific ramp-in strategies for Ultem to ensure pristine surface finish
- Stress-relief annealing: Precise heat treatment cycles both before and after machining to relieve internal stresses and ensure long-term dimensional stability
- Quality certifications: ISO 9001:2015, ISO 14001, ISO 13485 (medical devices), and IATF 16949 (automotive)
- Advanced metrology: CMM, optical comparator, surface profilometer, and hardness tester supporting typical tolerances of ±0.005mm
- Rapid turnaround: Quotes within hours, parts as fast as 4 days
Jucheng’s testing has shown that for load-bearing brackets that do not see friction, Ultem is often the technically superior choice over alternatives like PEEK. The company’s experience across aerospace, medical, semiconductor, and automotive industries means they understand the specific requirements of each sector—from FAA flame ratings to USP Class VI biocompatibility.
Frequently Asked Questions About Ultem Machining
What is the difference between Ultem 1000 and Ultem 2300?
Ultem 1000 is the unfilled base grade offering the best balance of machinability and mechanical properties. Ultem 2300 contains 30% glass fiber reinforcement, providing greater stiffness and dimensional stability at elevated temperatures but with more abrasive machining characteristics and higher tooling costs.
Can Ultem be machined to tight tolerances?
Yes. With proper setup, tooling, and process control, Ultem CNC加工 can achieve tolerances of ±0.01–0.02 mm. Jucheng Precision routinely holds tolerances of ±0.005mm with appropriate part geometry and process controls.
What tooling is recommended for machining Ultem?
Solid carbide tools are mandatory—HSS tools blunt too quickly. For Ultem 1000, sharp carbide end mills with 2 or 3 flutes and a 45°+ helix angle work well. For Ultem 2300, PCD-coated or diamond tools are recommended to combat the abrasive effects of glass fibers.
Why does Ultem require annealing?
Ultem is susceptible to stress cracking and warping from internal stresses generated during machining. Stress-relief annealing—heat treatment cycles before and after machining—relieves these internal stresses and ensures long-term dimensional stability. This is particularly important for high-precision or large parts.
What industries use machined Ultem components?
Aerospace (cabin interiors, instrument housings), medical devices (surgical instruments, sterilization trays), electronics and semiconductor (insulators, connectors), and automotive (under-hood components) are the primary industries.
Is Ultem difficult to machine?
Ultem is more challenging than standard engineering plastics like acetal or nylon. Its low thermal conductivity traps heat at the cutting edge, and its high rigidity makes it prone to brittle fracture if parameters are incorrect. However, with appropriate tooling, cooling, and process control, Ultem PEI 機械加工 can be performed reliably and repeatably.
What surface finish can be achieved with machined Ultem?
Typical machined finishes range from Ra 3.2 μm (125 μin) to finer values depending on machining requirements. Ultem 1000 generally produces a cleaner surface than Ultem 2300 due to the absence of glass fibers.
How does Ultem compare to PEEK for CNC machining?
Both are high-performance thermoplastics, but they have different strengths. PEEK offers higher continuous service temperature (260°C vs. 170–180°C for Ultem). However, Ultem is often the technically superior choice for load-bearing brackets that do not see friction, and it is generally easier to machine than PEEK. The choice depends on the specific application requirements.
Whether you are specifying Ultem 1000 for a精密 electronic housing or Ultem 2300 for a high-strength aerospace bracket, understanding the material’s properties, machining challenges, and best practices is essential for success. Partnering with an experienced shop like Jucheng Precision—with the right tooling, process controls, and quality systems in place—ensures your components meet specification the first time, every time.
Ready to discuss your next Ultem machining project? Contact Jucheng Precision for a quick quote and engineering consultation.