
낮은 Ra 값이 자동으로 더 나은 CNC 표면을 의미하지는 않습니다. 이는 더 느린 마무리 패스, 더 새로운 공구, 더 안정적인 공작물 고정, 추가 연마 및 더 많은 검사를 필요로 할 수 있으며, 그럼에도 불구하고 파상도, 가공 방향, 스크래치 또는 밀봉 성능을 제어하지 못할 수 있습니다. 실용적인 목표는 부품의 기능을 안정적으로 지원하는 가장 덜 제한적인 표면 요구 사항을 지정하는 것입니다. 이 가이드는 엔지니어와 구매자가 도면이 견적 단계에 도달하기 전에 CNC 표면 거칠기를 접촉, 밀봉, 마모, 외관, 측정 및 비용과 연결하는 방법을 보여줍니다.
낮은 Ra 지시값에 숨겨진 비용 함정
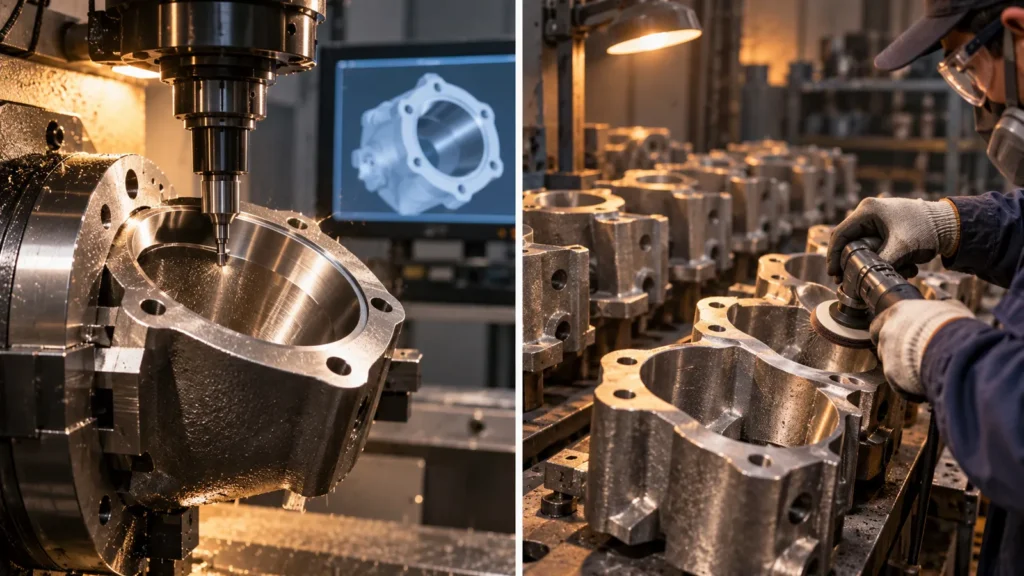
이것이 거칠기 요구 사항이 기능 표면에 속하는 이유이며, 자동으로 전체 모델에 적용되는 것은 아닙니다. 베어링 시트, 개스킷 안착면, 광학 대면 패널, 숨겨진 클리어런스 포켓은 동일한 역할을 하지 않습니다. 모든 면에 가장 까다로운 값을 적용하면 견적에 가장 어려운 해석의 비용과 위험이 포함됩니다.
Ra는 표면 이야기의 일부일 뿐입니다
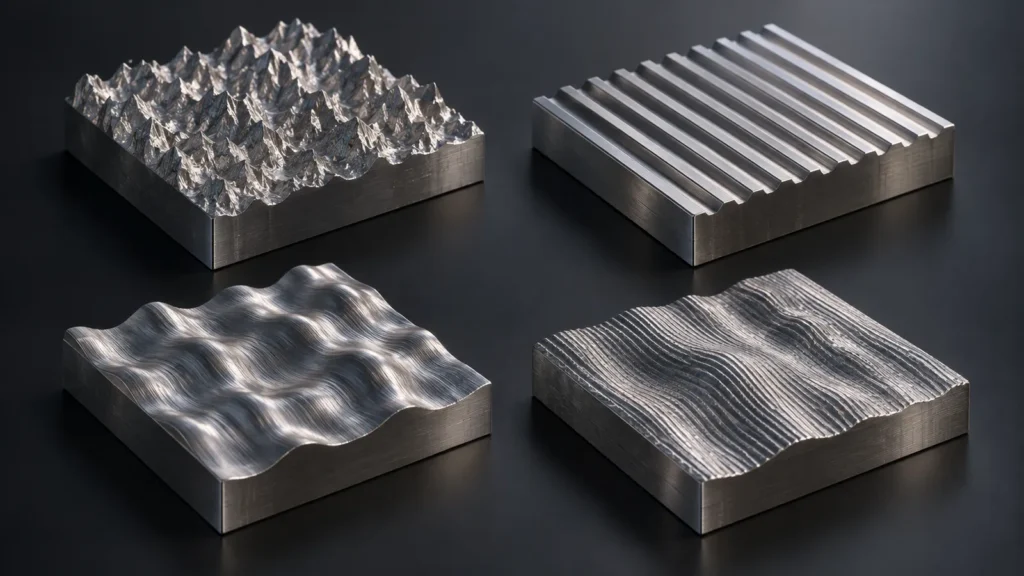
| 표면 용어 | 설명에 도움이 되는 것 | 단독으로 해결하지 못하는 것 |
|---|---|---|
| Ra | 평균 프로파일 편차 | 고립된 피크, 깊은 밸리, 레이, 웨이브니스 또는 시각적 균일성 |
| Rz | 샘플링 길이에 걸친 평균 피크-투-밸리 높이 | 텍스처의 간격 및 방향 |
| Lay | Dominant direction of the surface pattern | Amplitude or acceptance of scratches |
| Waviness | Longer-spaced surface variation | Fine roughness caused by the cutting process |
| Visual grade | Color, gloss, texture, scratches, and cosmetic consistency | A traceable numerical roughness result |
Use the broader CNC machining surface finishes guide when the decision also involves anodizing, blasting, polishing, plating, or another post-process. Roughness is one characteristic of the finished surface, not a synonym for every surface treatment.
접촉, 흐름 또는 외관부터 시작하십시오
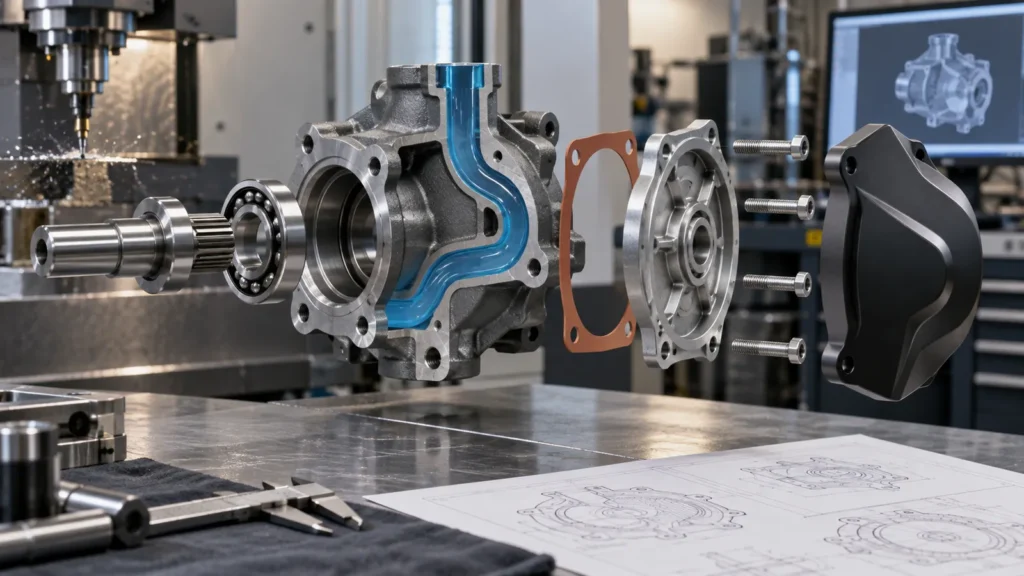
Mating and sliding interfaces
For a shaft, bushing, guide, or bearing seat, roughness works together with material, hardness, lubrication, geometry, and clearance. An extremely smooth surface is not always ideal: some interfaces need texture to retain lubricant, while sharp peaks may accelerate early wear. Specify the assembled function first and then choose the surface requirement with the fit.
Sealing faces and fluid paths
On gasket lands and sealing faces, lay direction and waviness can matter as much as average roughness. A directional tool pattern can create a leakage path. On fluid channels, burrs, transitions, cleanliness, and geometry may dominate over a small improvement in Ra.
Visible housings and controls
Customers judge appearance through texture consistency, tool marks, color, gloss, edge quality, and handling damage. A roughness number alone cannot define these. Cosmetic surfaces often need zones, viewing conditions, approved samples, and limits for scratches or dents in addition to—or instead of—a numerical Ra.
가공 공정이 결과를 형성하는 방법
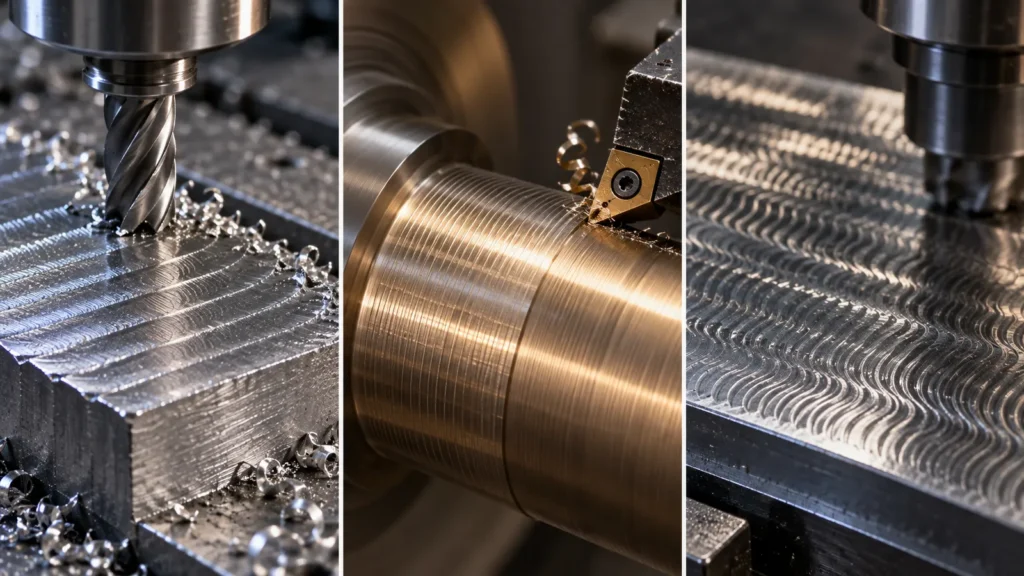
| Observed surface | Likely process questions | Useful next action |
|---|---|---|
| Regular feed marks | Feed, cutter geometry, stepover, and toolpath direction | Review the finishing pass and whether lay affects function |
| Chatter pattern | Tool reach, rigidity, workholding, spindle speed, and wall stiffness | Improve stability before demanding slower cosmetic rework |
| Torn or smeared material | Material condition, built-up edge, heat, tool sharpness, and coolant | Correct cutting conditions and verify material condition |
| Rounded polished edge | Manual access, polishing pressure, edge protection, and stock removal | Separate dimensional edges from cosmetic polish zones |
If the required texture is difficult to reach by cutting alone, a controlled secondary route may be appropriate. The site’s surface finishing capabilities overview helps connect the machined baseline to compatible post-process options.
의도한 것과 동일한 표면을 측정하십시오
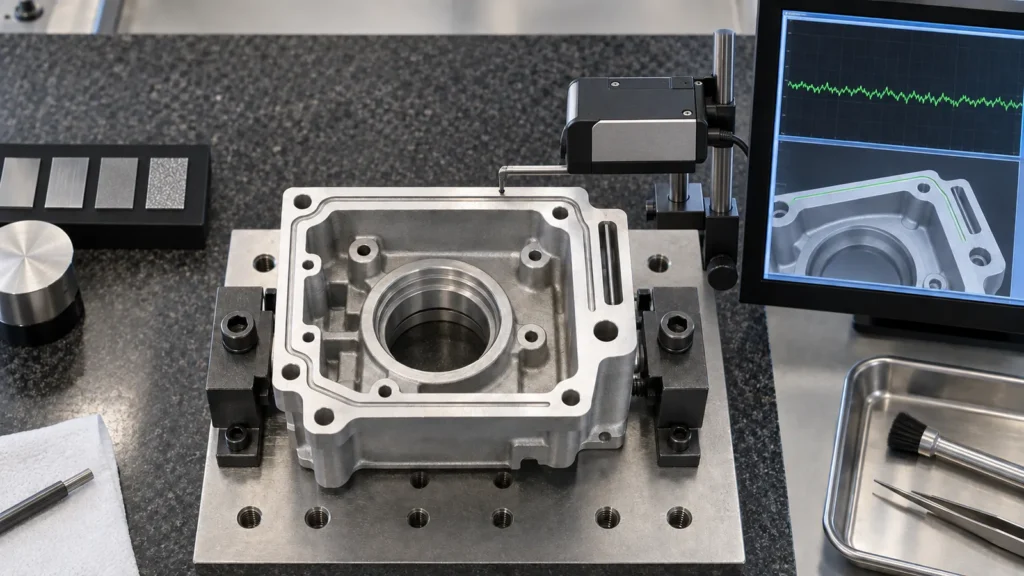
- Mark the exact measurement zone rather than pointing to the entire part.
- State the parameter, unit, maximum or range, and lay direction where function requires it.
- Confirm the evaluation location is physically accessible to the agreed instrument.
- Define whether measurement occurs before or after blasting, coating, polishing, or cleaning.
- Keep visual defects and numerical roughness in separate acceptance criteria.
- For critical features, agree on report format and sampling before production.
Measurement planning belongs in quality planning, not at the end of production. JUCHENG’s quality control overview explains the role of drawings, inspection planning, and documented verification across a machining project.
도면에 표기하는 더 나은 방법
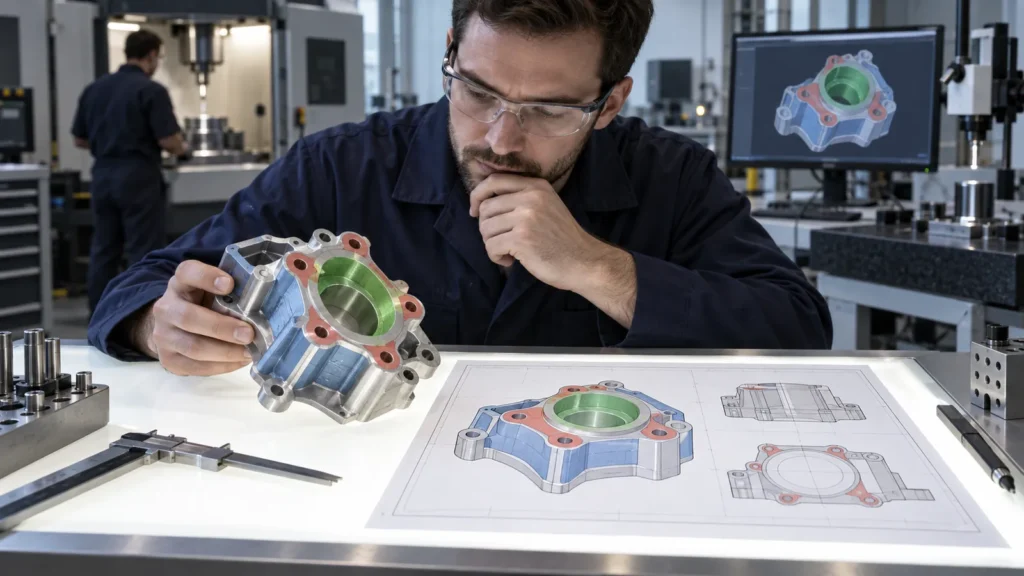
Example specification logic
- Functional face A: measured roughness requirement plus lay direction and inspection zone.
- Cosmetic zone B: visual texture and scratch limits controlled by approved sample.
- Bore C: final diameter and roughness verified after the last relevant finishing step.
- All other faces: standard machined condition with burrs removed and edges handled per drawing.
This structure gives the estimator a realistic route and gives inspection an unambiguous acceptance plan. It also makes value engineering possible: the supplier can challenge an expensive local callout without weakening the rest of the drawing.
RFQ 전 거칠기 검토
- Name the failure: leakage, wear, friction, poor adhesion, trapped contamination, objectionable tool marks, or something else.
- Identify the responsible surface: do not spread the requirement to unrelated faces.
- Select the characteristic: roughness parameter, lay, waviness, cosmetic sample, or a combination.
- Check manufacturability: tool access, stiffness, material behavior, secondary finishing, and handling.
- Plan verification: instrument access, measurement direction, timing, sample size, and records.
- Review total cost: machining time, post-processing, protection, inspection, and rejection risk.
The result should be specific enough to quote yet no tighter than the application needs. For available process combinations, compare the CNC surface finishing services page with the drawing’s material and functional requirements.
구매자가 거칠기에 대해 묻는 질문
Not always, because geometry, material, tool access, process capability, and quantity determine the real impact. However, a substantially smoother requirement can add finishing passes, tool control, polishing, protection, and inspection. The cost rises fastest when the callout covers difficult or nonfunctional surfaces.
Can bead blasting improve a roughness result?
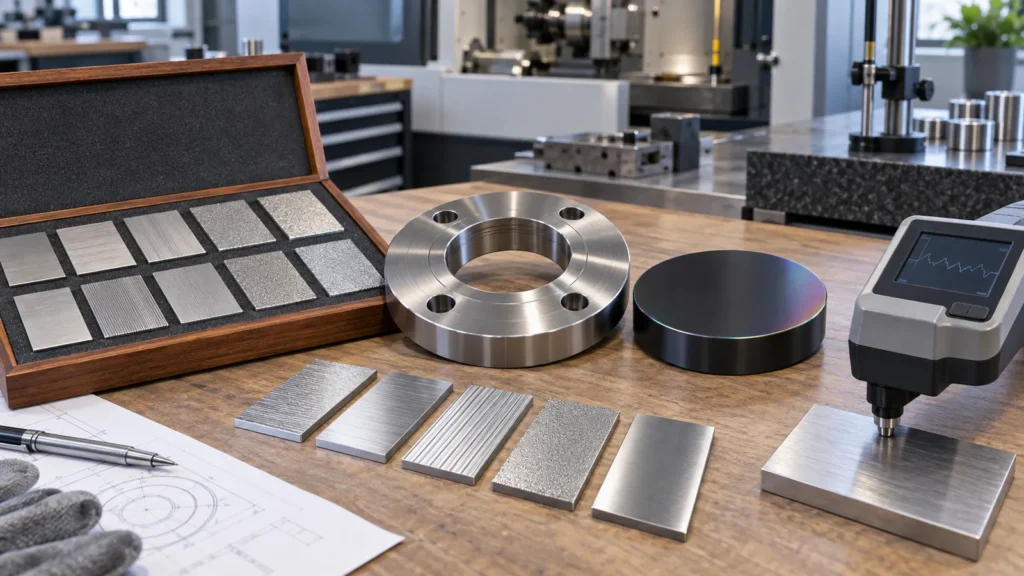
Blasting changes texture and can make appearance more uniform, but it does not simply convert a machined surface into a universally “better” numerical roughness. Media, pressure, material, masking, and measurement method affect the result. Specify blasting for its intended texture or preparation role and verify functional faces separately.
Should roughness be checked before or after coating?
That depends on function. A pre-coating value may control adhesion or the substrate condition, while the finished surface may control sealing, friction, or appearance. If both matter, identify both stages explicitly rather than assuming one measurement represents the other.
What information should accompany a roughness callout?
Provide the exact surface, parameter, unit, limit or range, lay direction when relevant, measurement stage, accessible inspection zone, and any separate cosmetic criteria. For a critical interface, include mating-part and service information during DFM review.