
Dans le paysage en constante évolution de la fabrication moderne, la demande de géométries complexes et de tolérances microscopiques n'a jamais été aussi élevée. Parmi le large éventail de technologies de fabrication soustractive, la découpe par électroérosion à fil conique se distingue comme un sommet de précision. Ce procédé spécialisé permet aux ingénieurs de créer des formes complexes et inclinées dans des matériaux trempés qui seraient impossibles à obtenir par fraisage ou tournage conventionnel. Que vous développiez des composants aérospatiaux ou des dispositifs médicaux de haute précision, comprendre les nuances de qu'est-ce que la découpe par électroérosion à fil et comment elle facilite le conicité complexe est essentiel pour rester compétitif sur le marché industriel actuel.
Alors que les industries repoussent les limites de la conception, jucheng s'est imposé comme un leader dans la fourniture de solutions CNC haut de gamme répondant à ces besoins spécifiques. En exploitant une technologie avancée de décharge électrique, le procédé de découpe par électroérosion à fil offre une méthode d'enlèvement de matière sans contact, garantissant que même les pièces les plus délicates restent exemptes de contraintes mécaniques. Dans ce guide complet, nous explorerons les principes mécaniques, les procédures opérationnelles et les avantages stratégiques de l'utilisation de la découpe par électroérosion à fil conique dans votre ligne de production.
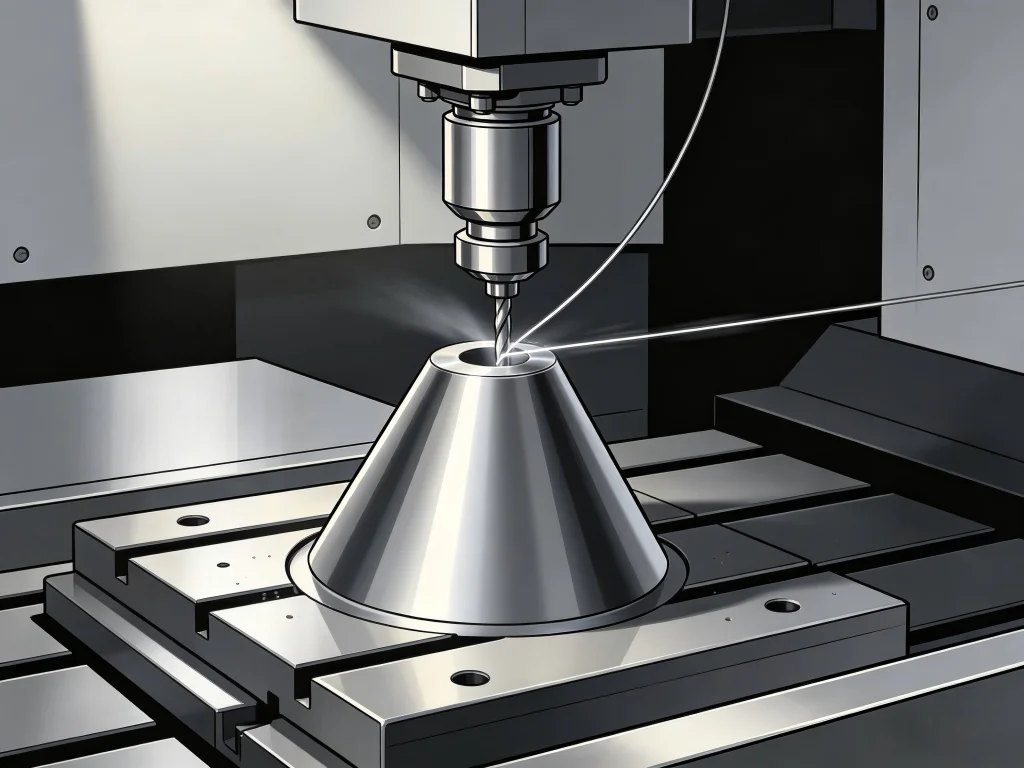
Comprendre les fondamentaux : qu'est-ce que la découpe au fil EDM ?
Pour appréhender la complexité de la découpe conique, il faut d'abord définir la technologie de base. La procédé de découpe par électroérosion à fil, également connue sous le nom d'usinage par électroérosion à fil (WEDM), consiste à utiliser un fil fin chargé électriquement pour “ trancher ” à travers un matériau conducteur. Ce fil, souvent appelé le outil de découpe au fil EDM, ne touche pas réellement la pièce. Au lieu de cela, il crée une série d'étincelles électriques rapides entre le fil et le matériau, immergé dans un fluide diélectrique—généralement de l'eau déminéralisée.
La procédure de découpe au fil EDM est régie par une érosion contrôlée. Lorsque les étincelles se produisent, elles fondent et vaporisent de petites quantités du matériau, qui sont ensuite évacuées par le fluide diélectrique. Cela permet la création de détails extrêmement fins et de coins internes nets. Dans une machine standard à 2 axes, le fil reste vertical. Cependant, dans la découpe par électroérosion à fil conique, la machine utilise un système à 4 ou 5 axes où les guides-fils supérieur et inférieur se déplacent indépendamment (axes U et V par rapport à X et Y), permettant au fil de s'incliner selon des angles précis.
Le rôle du fil de découpe au fil EDM
Le choix du fil de découpe au fil EDM est essentiel au succès de l'opération. Le plus souvent, on utilise du fil de laiton en raison de son excellente conductivité et de sa résistance à la traction. Cependant, pour des applications coniques spécialisées, des fils en molybdène à haute résistance ou revêtus de zinc peuvent être employés. Le diamètre du fil—généralement compris entre 0,1 mm et 0,3 mm—détermine le “ trait de scie ” ou la largeur de la coupe. En découpe conique, le fil doit maintenir une tension constante pour éviter le “ retard de fil ”, qui pourrait entraîner des imprécisions en haut ou en bas de la pièce.
La mécanique technique de la conicité
La capacité d'incliner le fil nécessite un contrôleur CNC sophistiqué. Pendant la procédure de découpe au fil EDM, the software calculates the offset for both the upper and lower guides. This is not a simple linear movement; the controller must account for the change in the wire’s length and the varying spark gap caused by the angle. Many practitioners on forums like Reddit often discuss the “taper compensation” feature found in high-end machines like those offered by jucheng, which automatically adjusts for wire flex and geometric distortion.
There are generally two types of tapers achieved in this process:
- Constant Taper: Where the angle remains the same throughout the profile of the cut.
- Variable Taper: Where the angle changes as the wire moves along the path, allowing for complex transitional shapes from a square base to a circular top, for example.
Core Applications Across High-Tech Industries
La polyvalence de la découpe par électroérosion à fil conique makes it indispensable in several sectors. Because the process is unaffected by material hardness, it is the preferred choice for working with titanium, inconel, and hardened tool steels. jucheng has seen a significant uptick in clients from the following fields:
1. Tool and Die Making
This is the traditional home of the procédé de découpe par électroérosion à fil. Tapered holes are essential for extrusion dies and injection molds, where a “draft angle” is required to allow the finished part to be ejected easily. The precision of the outil de découpe au fil EDM ensures that these angles are consistent within microns.
2. Aerospace Engineering
In aerospace, components often feature complex cooling holes or interlocking turbine blade roots. These geometries require the multi-axis movement that only la découpe par électroérosion à fil conique can provide. The lack of heat-affected zones (HAZ) compared to laser cutting is a major benefit for flight-critical parts.
3. Medical Device Manufacturing
Surgical instruments and orthopedic implants often require intricate, tapered slots. The fil de découpe au fil EDM can navigate these tiny paths without burring, which is vital for components that will be used inside the human body.
Critical Factors When Choosing an EDM Solution
Selecting the right machinery and partner is a strategic decision. Users often debate the merits of various brands on platforms like Facebook industry groups, but several objective factors should guide your choice:
| Factor | Description | Impact on Quality |
|---|---|---|
| Positional Accuracy | The ability of the X, Y, U, and V axes to move to the exact coordinates. | Directly affects the dimensional tolerance of the taper. |
| Generator Technology | How the machine manages the electrical pulse. | Determines the surface finish (Ra value) and cutting speed. |
| Wire Tension Control | The system that keeps the fil de découpe au fil EDM taut during angled moves. | Prevents “belly” or curvature in the tapered surface. |
| Dielectric System | Filtration and temperature control of the deionized water. | Ensures consistent spark conditions and prevents thermal expansion of parts. |
Installation and Maintenance: Ensuring Longevity
To maintain the high precision of la découpe par électroérosion à fil conique, a rigorous maintenance schedule is required. The environment plays a significant role; machines should ideally be placed in a temperature-controlled room to avoid the expansion and contraction of the machine casting. jucheng recommends the following routine checks:
- Power Feed Contact Cleaning: The points where electricity is transferred to the wire must be kept clean of debris to prevent “arcing” and wire breakage.
- Filter Replacement: The dielectric fluid must be pristine. Clogged filters lead to poor flushing, which causes unstable sparks and a rougher surface finish.
- Resin Monitoring: Deionized water needs a specific conductivity level. Ion exchange resins must be replaced when the water becomes too conductive.
- Guide Alignment: For taper cutting, the vertical alignment of the upper and lower guides (the “zero” position) must be calibrated frequently using a master square or laser alignment tool.
The Jucheng Advantage: Why We Lead in EDM Tech
Choosing jucheng means more than just buying a machine; it means investing in a partnership. Our la découpe par électroérosion à fil conique systems are engineered with the latest CNC controllers, capable of handling 45-degree tapers with ease. We understand that in the procédé de découpe par électroérosion à fil, reliability is paramount. That is why our machines feature high-rigidity castings and ultra-precise linear scales.
Our commitment to the procédure de découpe au fil EDM extends to our support. We provide extensive training for operators, ensuring they can maximize the potential of the outil de découpe au fil EDM. From selecting the right fil de découpe au fil EDM for a specific alloy to optimizing cutting parameters for speed vs. finish, jucheng is there to guide you through every micron of the process.
Frequently Asked Questions (FAQ)
1. What is the maximum angle possible in taper cutting wire edm?
While standard machines can handle 10-15 degrees, high-performance machines from jucheng can achieve tapers up to 45 degrees or more, depending on the height of the workpiece and the guide configuration. It is important to note that as the angle increases, the maximum thickness of the workpiece the machine can cut may decrease.
2. Does wire cutting produce heat that could damage the part?
La procédé de découpe par électroérosion à fil is a thermal process, but it is extremely localized. The dielectric fluid acts as a coolant, immediately quenching the area. While a microscopic “recast layer” exists, it is significantly smaller than the heat-affected zone found in laser or plasma cutting, making it safe for most precision applications.
3. How do I choose the right edm wire cut wire?
For most general purposes, a standard brass wire is sufficient. However, if you are performing high-speed cutting or working with very thick materials, a zinc-coated wire might be better as it offers better flushing properties. For ultra-fine details, a tungsten or molybdenum wire might be used due to its high tensile strength at small diameters.
4. What is the typical surface finish of a wire-cut part?
With multiple “skim passes,” a la découpe par électroérosion à fil conique machine can achieve a mirror-like finish with an Ra value of less than 0.1 μm. The initial “rough cut” will be much coarser, but subsequent passes using lower energy levels refine the surface.
5. Can I cut non-conductive materials?
No, the procédure de découpe au fil EDM requires the material to be electrically conductive. This includes all metals, graphite, and some ceramics. If the material does not allow electricity to pass through it, the spark cannot be generated.
6. Is the edm wire cut tool reusable?
No, the wire used in procédé de découpe par électroérosion à fil is used only once. It is fed from a supply spool, passes through the workpiece, and is then collected in a scrap bin or chopped for recycling. This ensures that a fresh, perfectly round wire is always at the point of the cut, which is vital for maintaining precision.
7. Why is deionized water used instead of oil?
Most wire EDM machines use deionized water because it has a lower viscosity than oil, allowing it to flush the tiny kerf more effectively. However, some specialized “oil-based” wire machines exist for even finer surface finishes and smaller spark gaps.
8. How does Jucheng ensure machine accuracy over time?
jucheng utilizes hand-scraped surfaces on critical components and high-grade ball screws. Additionally, our software includes pitch error compensation and thermal growth compensation to ensure that the machine remains accurate even during long production runs in varying temperatures.
Solving Complex Geometries: A Problem/Solution Approach
Imagine a scenario where a manufacturer needs to produce a series of complex extrusion dies for a new automotive seal. These dies require a variable taper that changes continuously along a 3D path. Traditional machining would require a 5-axis mill, but the hardness of the D2 tool steel makes tool wear an expensive nightmare. Furthermore, the sharp internal corners are impossible for a physical cutting tool to reach.
This is where la découpe par électroérosion à fil conique acts as the ultimate solution. By using the outil de découpe au fil EDM, the manufacturer can program the exact taper into the CNC. Because there is no physical force between the wire and the steel, there is no tool deflection. The procédé de découpe par électroérosion à fil carves through the hardened steel with the same ease as soft aluminum. The result is a perfect die with a surface finish that requires no manual polishing, significantly reducing lead times and costs.
Furthermore, by utilizing the high-speed capabilities of jucheng equipment, the procédure de découpe au fil EDM can be automated for overnight runs. This solves the “bottleneck” problem often found in tool rooms. By the time the technicians arrive in the morning, the complex tapered parts are finished, cleaned, and ready for assembly. This efficiency is why modern shops are increasingly moving toward advanced EDM solutions to solve their most difficult geometry puzzles.
Conclusion
In conclusion, la découpe par électroérosion à fil conique is a sophisticated and indispensable technology for any manufacturer dealing with high-precision, complex geometries. From the initial understanding of qu'est-ce que la découpe par électroérosion à fil to the selection of the correct fil de découpe au fil EDM, every step of the process requires technical expertise and reliable equipment. Whether you are tackling a specific production problem or looking to upgrade your facility’s capabilities, jucheng offers the technology and support necessary to achieve excellence. By focusing on precision, maintenance, and the right application of the procédé de découpe par électroérosion à fil, you can ensure that your components meet the highest standards of the modern industrial world.
Ready to elevate your machining precision? Explore the full range of high-performance CNC and EDM solutions at jucheng. Our team of experts is ready to help you optimize your procédure de découpe au fil EDM for maximum efficiency and accuracy. Contact us today to discuss your next project!