
Règle de décision : comparez la route de fabrication complète—programmation, montages, fixations, temps de coupe, portée des outils, inspection et risque—et non le taux horaire machine isolé.
La mauvaise question est “ Quelle machine coûte le plus cher par heure ? ”
 Un taux horaire machine reflète l'équipement, la main-d'œuvre, la maintenance, l'utilisation et les frais généraux, mais un acheteur achète des pièces conformes—pas du temps machine. L'aperçu parent de coût de l'usinage CNC montre comment la préparation, le temps de cycle, l'outillage, le contrôle, la finition et le risque se combinent dans un devis. Le nombre d'axes modifie plusieurs de ces blocs de coûts en même temps.
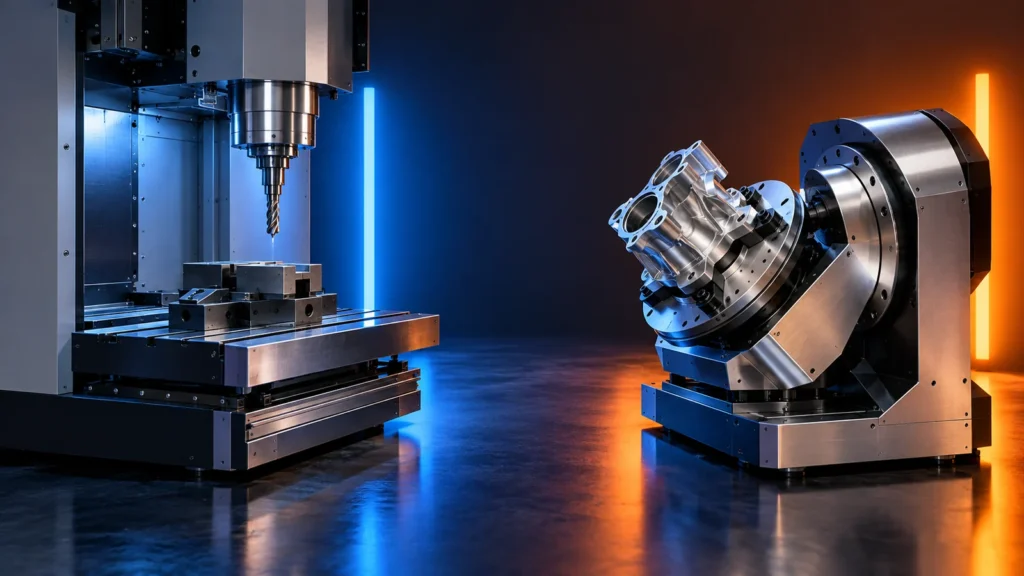
Une machine 3 axes déplace l'outil de coupe selon X, Y et Z. Atteindre une autre face de la pièce nécessite normalement une réorientation ou une nouvelle préparation. Une machine 5 axes ajoute deux mouvements rotatifs, permettant à l'outil ou à la pièce d'aborder les caractéristiques depuis des directions supplémentaires. La comparaison des coûts dépend de si cet accès supplémentaire élimine suffisamment de travail ailleurs dans la gamme.
| Question de coût | Gamme 3 axes | Gamme 5 axes |
|---|---|---|
| Combien d'orientations ? | Peut nécessiter plusieurs préparations manuelles | Peut combiner des faces en une seule préparation |
| Quel maintien de pièce est nécessaire ? | Travail simple en étau ou plusieurs montages | Maintien de pièce initial plus spécialisé |
| Comment les références sont-elles transférées ? | Réétablies après réorientation | Davantage de relations peuvent rester dans un même système de coordonnées |
| Quelle portée d'outil est requise ? | Des outils longs peuvent être nécessaires pour un accès incliné | L'outil peut s'approcher plus près de la direction normale |
| Quelle est la complexité de la programmation ? | Trajectoires d'outil plus simples, planification de montage plus importante | Simulation et contrôle de collision plus complexes |
Faire passer la même pièce par deux gammes d'usinage
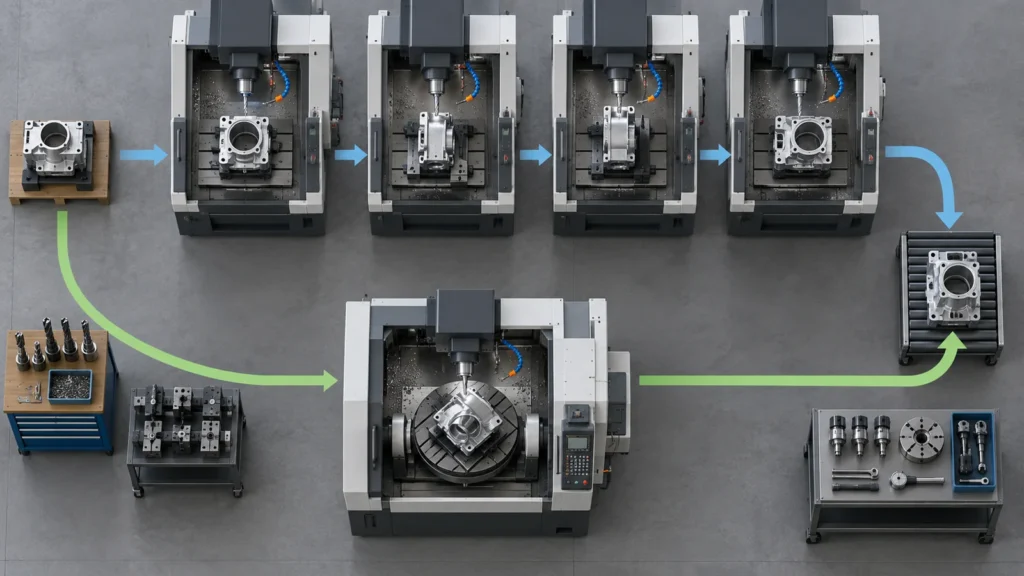 Considérez un boîtier avec une poche supérieure, des orifices latéraux, une face d'étanchéité inclinée et plusieurs relations de position. Un plan 3 axes pourrait usiner le dessus, transférer la pièce sur un montage latéral, répéter ce transfert pour une autre face et utiliser un montage incliné pour la surface d'étanchéité. Un plan multi-axes pourrait établir une seule référence principale et atteindre plusieurs caractéristiques sans retirer la pièce.
Cet exemple ne prouve pas que l'usinage 5 axes est automatiquement moins cher. La gamme multi-axes peut nécessiter davantage de préparation FAO, une simulation de collision minutieuse, un maintien d'œuvre qualifié et une disponibilité machine. La comparaison ne devient utile que lorsque les deux gammes incluent toutes les opérations, du brut à la pièce acceptée.
La Processus de fraisage CNC le guide fournit un contexte de processus plus large. Ici, la décision est plus restreinte : quelle gamme produit les relations requises avec le moins de travail total et d'incertitude ?
La quantité peut inverser la réponse
At one or ten parts, avoiding several dedicated fixtures may make a flexible 5-axis setup attractive. At hundreds or thousands of parts, repeatable workholding, pallet loading, cycle balancing, and available spindle capacity may favor a different route. The correct comparison uses the buyer’s release quantity and repeat-order pattern—not an assumed annual volume that may never be ordered.
Revision maturity matters too. A prototype that is still changing benefits from adaptable workholding. A stable production design may justify purpose-built fixtures and a carefully optimized 3-axis sequence. Buyers should therefore request quantity breaks without assuming the same process will remain optimal at every volume.
3-Axis Wins When Extra Motion Does Not Remove Extra Work
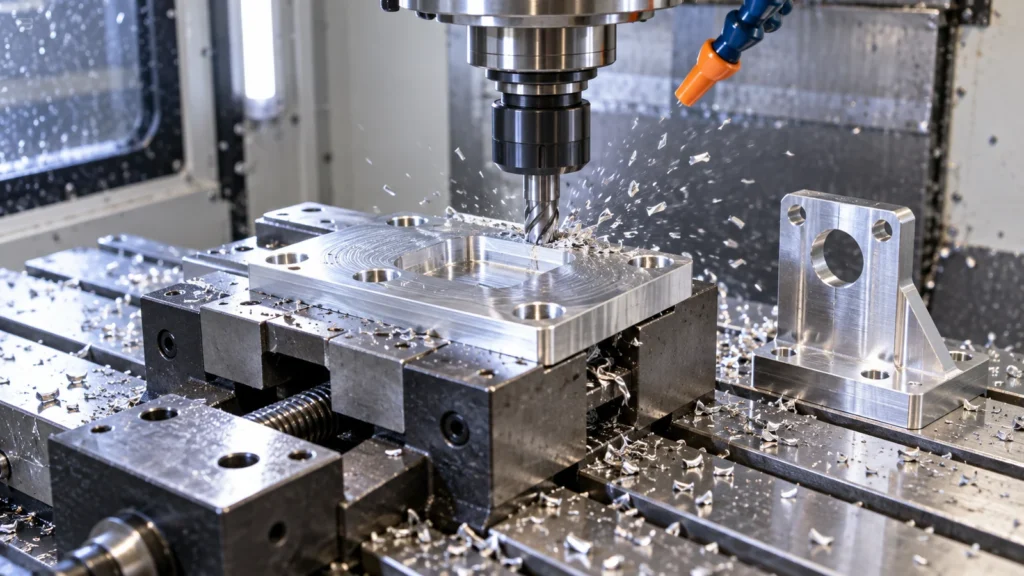 Simple plates, brackets, spacers, covers, and parts dominated by features on one accessible side often suit 3-axis machining. Standard vises and familiar cutters keep programming, setup, and proving straightforward. If a second side only needs a simple flip, the additional orientation may cost less than assigning a more advanced machine.
Three-axis can also be attractive when production uses stable dedicated fixtures. A repeat batch may justify workholding that locates the part quickly and consistently. Once that route is proven, moving it to another machine solely to reduce setup count may not improve total cost.
- Most features are reachable from one direction.
- Secondary faces have generous positional relationships.
- The geometry accepts short standard tools.
- Workholding is simple and repeatable.
- The quantity supports a proven fixture or pallet strategy.
- No undercuts or continuously changing tool orientations are required.
5-Axis Wins When Access and Relationships Dominate the Job
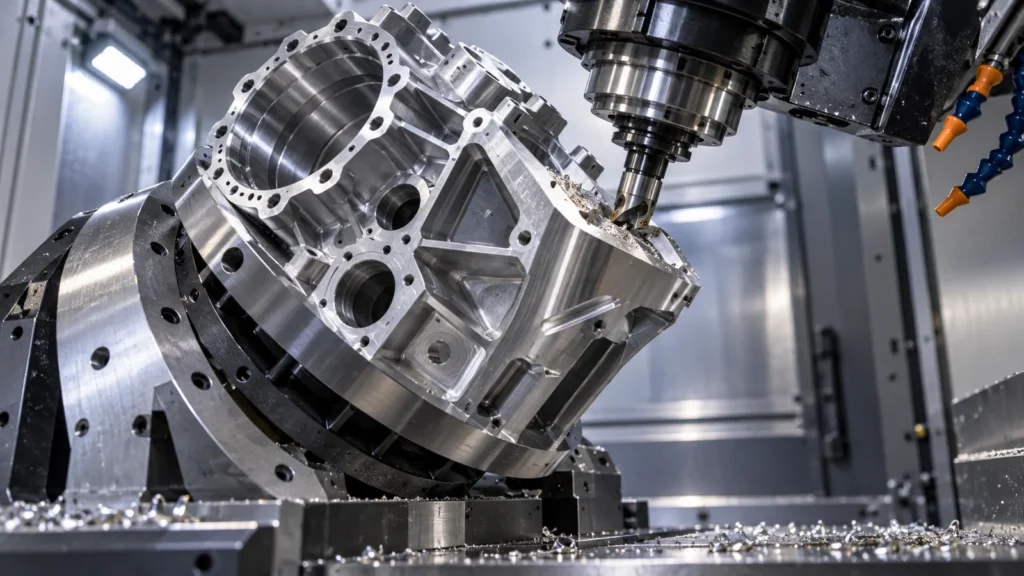 Multi-face parts, angled holes, impeller-like surfaces, compound contours, and features with tight relationships across orientations can benefit from 5-axis access. Fewer removals from the fixture can reduce handling and the accumulation of location error. Tilting the workpiece or tool can also permit shorter, stiffer cutters, which may improve surface consistency and reduce deflection on deep or angled features.
A 5-axis route can be especially valuable at prototype and low-volume quantities because there may be too few parts to amortize several custom fixtures. One adaptable setup can replace the design, manufacture, and proving of dedicated workholding. At higher quantities, the answer can change: a fast 3-axis cell with optimized fixtures may outperform a flexible multi-axis route.
The site’s capacité de fraisage 5 axes page explains the process offering. A quote should still justify why the selected route fits the individual geometry rather than using axis count as a blanket quality label.
Tool orientation can affect more than cycle time
Approaching a surface closer to its normal direction can allow a shorter tool, improve chip evacuation, reduce holder interference, and provide a more consistent contact condition. These advantages may reduce finishing passes or hand blending on complex surfaces. They are valuable only when the final surface and dimensional requirements need them; using 5-axis motion on generous geometry may add programming effort without changing acceptance.
Do Not Confuse 3+2 Positioning with Simultaneous 5-Axis Cutting
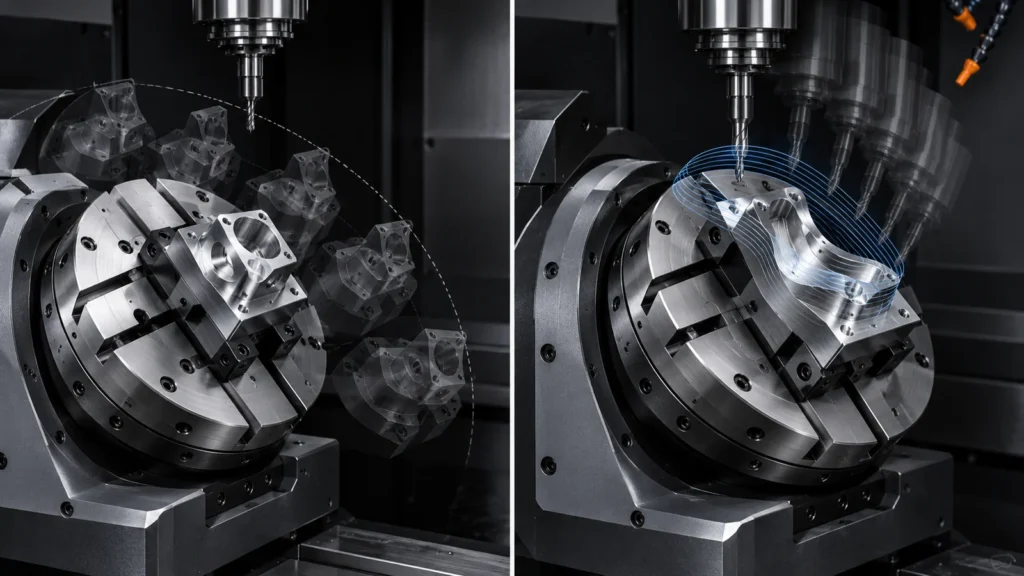 Many parts called “5-axis” do not require all axes to move during the cut. In 3+2 positional machining, rotary axes orient the part, lock it at an angle, and allow conventional three-axis cutting from that direction. This can combine faces and improve access without the programming and motion demands of simultaneous machining.
Simultaneous 5-axis motion is appropriate when the cutter orientation must change continuously along a complex surface, when tool contact needs close control, or when geometry cannot be produced through indexed positions alone. Specifying simultaneous machining for a part that only needs indexed access can narrow the supplier pool without improving the result.
The Cheapest Route Must Still Control Accuracy and Scrap Risk
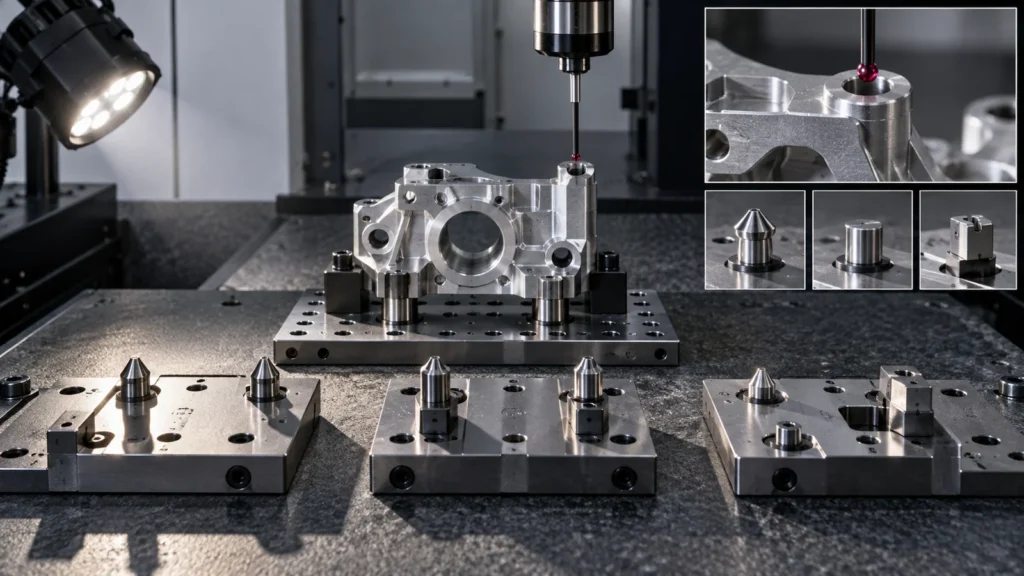 Each time a part is unclamped and re-established, variation can enter through locating surfaces, debris, clamping force, fixture condition, and datum pickup. That does not make multi-setup machining unreliable; well-designed fixtures and inspection can control it. It does mean the quote should account for how critical relationships survive the transfer.
Five-axis machining introduces different risks. Rotary-axis calibration, tool-center-point control, collision clearance, post-processing, probing strategy, and operator experience all matter. A single-setup claim is only valuable when the machine, program, and inspection plan can verify the required result.
The appropriate quality control workflow should follow the chosen route. Multi-face positional relationships may need in-process probing or CMM verification, while simpler parts may be efficiently accepted with dedicated gauges and standard dimensional checks.
One setup does not mean one operation
Marketing descriptions sometimes treat “single setup” as though the entire part emerges complete without interruption. In practice, the route can still include probing, roughing, semi-finishing, tool changes, deburring, a second operation for the clamped face, and final inspection. The benefit is that selected critical features stay related within one controlled orientation—not that all manufacturing work disappears.
Likewise, several 3-axis setups are not automatically a defect. If locating surfaces are robust, fixtures are proven, and the critical relationships tolerate the transfers, multiple operations may be predictable and economical. The quotation should expose these assumptions so the buyer can distinguish a capable route from an optimistic one.
Ask for a Route Explanation, Not a Preferred Axis Count
A buyer can unintentionally inflate cost by requiring 5-axis machining in the RFQ when the drawing only needs a conforming part. Unless the process itself is controlled for a validated reason, specify function, material, critical characteristics, finish, quantity, and inspection evidence. Let qualified suppliers propose the route.
When quotes use different equipment, request enough information to normalize them:
- Number of machining setups and major datum transfers.
- Whether the route is 3-axis, indexed 3+2, or simultaneous 5-axis.
- One-time fixture or programming charges.
- Inspection plan for cross-face and angled relationships.
- Quantity assumptions and repeat-order treatment.
- Operations performed outside the quoting supplier.
Also review the functional requirements in the Tolérances d'usinage CNC article before comparing routes. A cost advantage is meaningful only when both suppliers price the same acceptance conditions.
3-Axis and 5-Axis Cost Questions
Is 5-axis machining always more expensive?
No. Its machine rate may be higher, but fewer setups, fixtures, datum transfers, and long-tool operations can reduce total part cost for suitable geometry.
Is 3-axis better for simple parts?
Often. If features are accessible with simple workholding and one or two orientations, 3-axis machining can provide the most direct route.
Does every multi-face part need simultaneous 5-axis machining?
No. Indexed 3+2 machining may orient the part to several faces while cutting with conventional three-axis motion.
Why can fewer setups improve cost?
They can reduce handling, fixture preparation, datum recovery, in-process checks, and the risk associated with transferring critical relationships.
Should the drawing specify the machine axis count?
Only when a controlled process requirement makes it necessary. Otherwise specify the functional result and let the supplier propose a capable manufacturing route.