
드릴이 두 포트를 연결했다고 해서 PVDF 통로가 완성되는 것은 아닙니다. PVDF 가공에는 교차부에 대한 합의된 상태 조건, 부착된 재료를 제거하는 접근 가능한 방법, 그리고 그 결과를 검사하는 방법이 필요합니다. 먼저 어떤 엣지가 씰이나 유체 흐름에 접촉하는지, 어떤 엣지가 완화(relief)될 수 있는지 표시하십시오. 그런 다음 해당 부품이 어떻게 세정되고 합격 판정될지 결정하십시오. 깨끗해 보이는 외부 표면이나 폴리머 명칭만으로는 통로 내부의 상태를 입증할 수 없습니다.
PVDF, 즉 폴리불화비닐리덴은 재료 특성이 사용 조건에 적합한 엔지니어링 부품에 사용됩니다. Ensinger는 PVDF 소재 형상 및 기타 블랭크의 밀링과 선반 가공을 설명합니다. 여기서의 논의는 가공 부품을 어떻게 지정할지에 관한 것이며, 명시되지 않은 유체 시스템의 화학적 호환성, 순도 등급 또는 사용 수명을 확립하지는 않습니다.
작업 선정 전에 통로 맵을 작성하십시오
축방향 보어, 두 개의 교차 드릴 포트, 장착면을 가진 작은 분배 블록을 예로 들어 보겠습니다. 각 통로의 공구 진입점, 교차부, 출구를 표시하십시오. 교차부에 도달한 드릴이 반드시 디버링 공구나 카메라를 위한 공간을 남기는 것은 아닙니다. 형상이 아직 변경 가능한 동안 이러한 접근 요구 사항을 함께 설계하십시오.
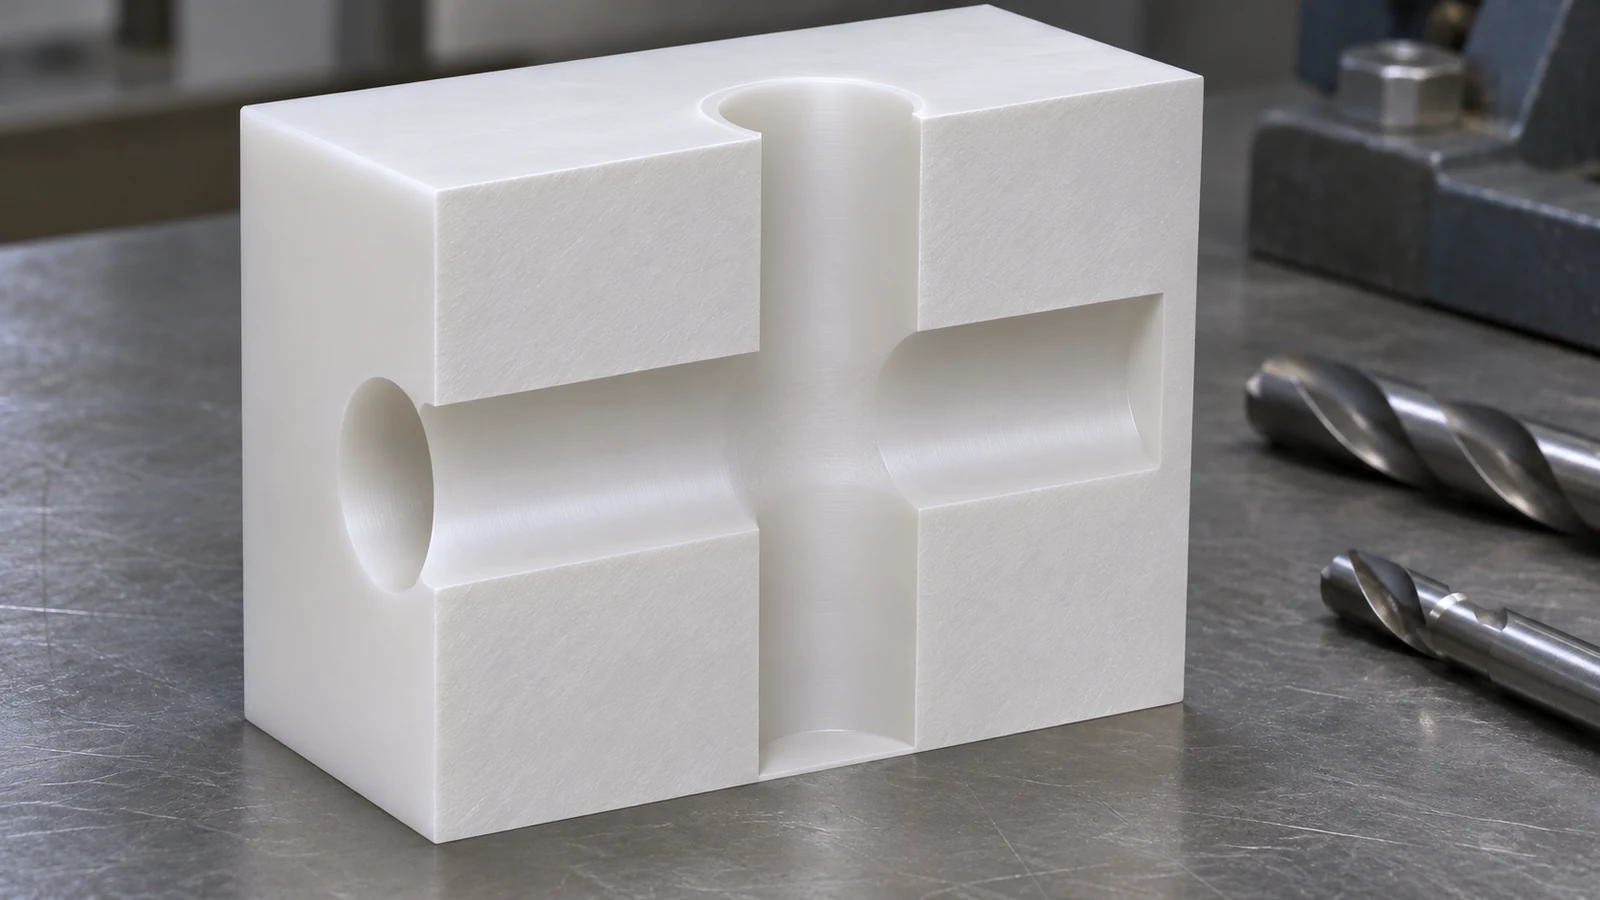 관통 통로, 분리 가능한 마감재 또는 변경된 포트 방향이 의도된 기능을 바꾸지 않고 마감과 검사를 가능하게 할 수 있는지 검토하십시오. 모든 마감재는 또한 밀봉과 청결성 문제를 야기합니다. 조립된 시스템에 무엇이 추가되는지 검토하지 않은 채 절삭을 단순화하기 위해서만 플러그를 도입하지 마십시오.
통로 형상과 장착 형상을 분리하십시오. 포트는 씰 면과의 관계가 필요할 수 있지만, 외부 장착 홀은 조립에 충분한 정밀도만 있으면 됩니다. 이러한 작업을 독립적으로 정의하면 전체 블록이 하나의 인터페이스에 대한 가장 엄격한 요구 사항을 물려받는 것을 방지할 수 있습니다.
실제로 합격 판정 대상이 되는 엣지를 식별하십시오
부착된 버, 번진 립, 찢어진 엣지, 의도적인 챔퍼는 서로 다른 상태입니다. “디버링”만 명시한 도면은 한 공급업체는 모든 엣지를 깎아내고 다른 공급업체는 느슨한 재료만 제거하면서 날카로운 기능적 전이부를 보존하는 결과를 초래할 수 있습니다. 밀봉, 삽입 또는 유동을 변화시키는 위치에서 허용 가능한 엣지 처리를 명시하십시오.
| 위치 | 잠재적 문제 | 유용한 도면 또는 공정 지시 |
|---|---|---|
| 교차 보어 접합부 | 쉽게 볼 수 없는 곳에 남아 있는 부착 재료 | 제거 및 검사 접근 범위 정의 |
| 시일 진입 모서리 | 날카롭거나 손상된 립은 삽입을 방해함 | 허용되는 리드인 및 표면 상태 정의 |
| 나사 입구 | 느슨한 칩 또는 변형된 첫 나사산 | 절삭 및 세척 후 입구 검사 |
| 장착 주변부 | 불필요한 외관 재작업 | 취급 모서리와 기능 인터페이스 분리 |
For PVDF 가공, 공정 순서는 가장 민감한 인터페이스가 이후의 칩 이동과 공구 접촉으로부터 보호되도록 해야 합니다. 시일 랜드를 먼저 마감한 후 다른 공정의 칩이 그 위를 지나가더라도, 최종 검사에서는 실제로 전달된 표면을 여전히 평가해야 합니다.
픽스처로 움직임을 숨기지 말고 깨끗하게 절삭하십시오
Heat and restraint influence polymer geometry during machining. A tool that rubs instead of cutting can change the surface, while a fixture can hold the component in a shape that it will not retain after release. Use tool condition, support and chip evacuation as connected process variables rather than treating a smaller feed or a tighter clamp as an automatic improvement.
On a block with a deep passage, accumulated chips can increase rubbing and obscure whether the drill is still cutting effectively. On a thin mounting ear, the same force may produce local deflection. Inspect the relevant feature after release before concluding that the machine’s in-cycle position demonstrates the finished geometry.
The trial should use the actual grade and stock form. Record any coolant or cleaning restrictions before selecting a cutting fluid. A material compatibility concern should be resolved with the stock supplier and application owner; a generic claim of chemical resistance is not approval of every fluid used during manufacturing.
디버링, 세정, 검증은 별개의 산출물입니다
Deburring removes or modifies unwanted attached material. Cleaning removes specified contamination. Inspection establishes whether the required condition has been achieved. Cleaning alone cannot be assumed to remove every firmly attached lip, and a burr-free edge can still carry unwanted residue.
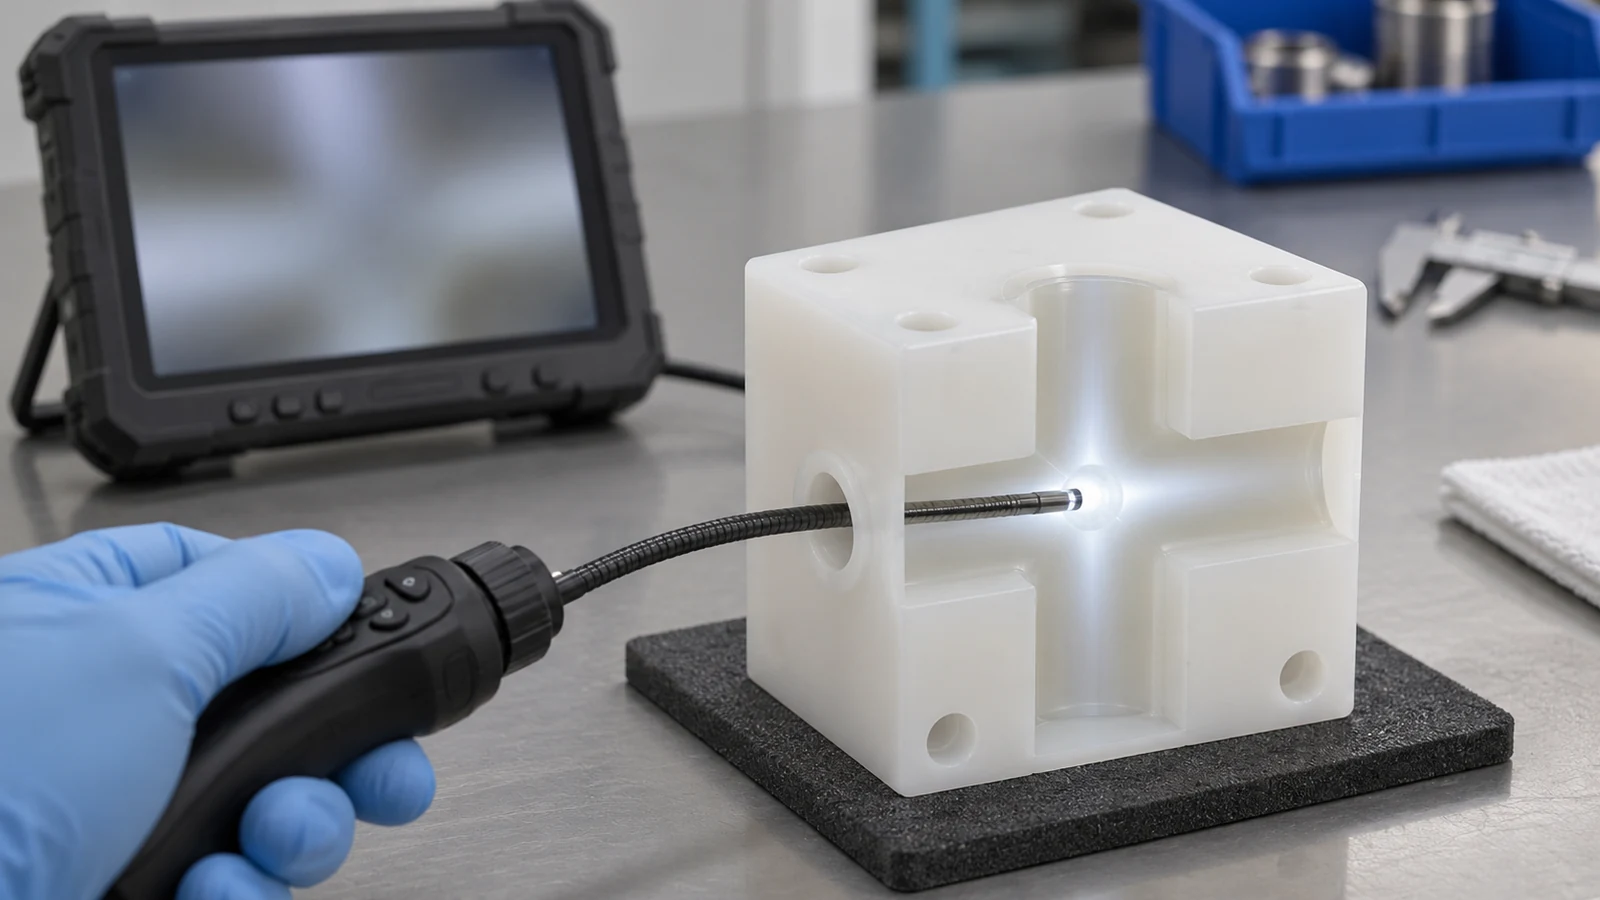 Agree what must be inspected, how it can be reached and what the inspection record will show. A borescope may reveal a visible lip but cannot automatically quantify an edge radius. A flushing result may support a defined residue requirement but does not prove the geometry of an inaccessible intersection. Match each method to the question it can answer.
For sensitive passages, identify the allowed manufacturing aids, wash medium where controlled, drying condition, handling and protective packaging. If the buyer needs a particle limit or another cleanliness test, name the method and acceptance basis separately. This component-level agreement is more precise than an unsupported label such as “ultra-clean PVDF.”
검사자가 사용할 수 있는 도면을 발행하십시오
Include the exact PVDF requirement, a model and drawing, datum relationships, port and thread specifications, controlled edge details and any restricted residues. Show the assembled seals or mating geometry where they explain the functional surfaces. Keep general tolerances on noncritical areas unless a particular function justifies a tighter limit.
The plastic material reference helps organize material choices, but the released drawing must identify the actual grade and finished-part requirements. A quotation should explain any inspection access that cannot be achieved and any cleaning requirement that needs a separate qualified process. PVDF machining acceptance is strongest when the geometry, surface and residue requirements are individually verifiable.
PVDF 관련 실무 질문
Should every internal edge have the same chamfer?
No. Seal entries, thread starts and flow intersections serve different functions. Specify the intended edge where it affects performance and review accessibility.
Can a clear flushing liquid prove a cross-hole is burr-free?
아니요. 액체가 투명해 보여도 부착된 립(lip)이 남아 있을 수 있습니다. 교차부 자체를 다루는 검사 방법을 사용하십시오.
PVDF 코팅은 PVDF 소재 가공과 동일한 범위입니까?
아니요. 금속 부품에 코팅하는 것과 폴리머 블랭크에서 재료를 제거하는 것은 서로 다른 기재, 공정 및 합격 기준을 수반합니다.
소재 형태가 바뀌면 무엇을 변경해야 합니까?
고정, 재료 제거, 검사 및 승인된 자격 검증을 재검토하십시오. 다른 블랭크는 원래 시험에서 관찰된 모든 거동을 재현하지 않고도 재료를 절약할 수 있습니다.