
Perché lo stesso pezzo CNC può ricevere preventivi molto diversi? La risposta di solito non è una misteriosa differenza di ricarico. Ogni fornitore sta prezzando un percorso produttivo: materiale e forma del grezzo, programmazione, attrezzaggi, sistemi di fissaggio, tempo di taglio, utensileria, finitura, ispezione, documentazione, imballaggio e il rischio tecnico creato dal disegno. Comprendere questi fattori aiuta gli ingegneri a ridurre i costi evitabili e aiuta gli acquirenti a confrontare i preventivi sullo stesso ambito.
Un preventivo CNC è un piano di produzione

Due preventivi possono quindi essere entrambi tecnicamente ragionevoli pur coprendo ambiti diversi. Uno può includere certificati dei materiali, report dimensionale completo, finitura, imballaggio protettivo e un ciclo di lavorazione conservativo. Un altro può prezzare solo la lavorazione e lasciare aperti tali elementi. La prima domanda quando un preventivo sembra alto non è “Puoi farmi uno sconto?” ma “Quale requisito o assunzione sta guidando il ciclo?”
Per un approfondimento su come i requisiti CAD diventano attrezzaggi, percorsi utensile, finitura e ispezione, consulta la sezione del sito Guida al processo di lavorazione CNC.
I fattori di costo dietro un pezzo lavorato

| Categoria di costo | Che cosa genera il costo | Domanda dell'acquirente |
|---|---|---|
| Ingegneria e attrezzaggio | Revisione DFM, programmazione, attrezzature di fissaggio, setup utensili, allineamento dei datum e prove del primo pezzo | Quali costi non ricorrenti sono inclusi o ammortizzati? |
| Materiale e resa | Grado, tempra, dimensione del grezzo, sovrametallo di taglio, scarti e certificazione | Tutti i fornitori stanno quotando la stessa condizione del materiale e la stessa assunzione sul grezzo? |
| Tempo di lavorazione | Asportazione di materiale, cambi utensile, rotazioni del pezzo, sbraccio utensile e passate di finitura | Quale geometria o fase di processo consuma più tempo? |
| Post-lavorazione | Trattamento termico, anodizzazione, placcatura, passivazione, lucidatura, marcatura e pulizia | I processi esterni sono specificati e inclusi sulla stessa base? |
| Qualità e logistica | Ambito di ispezione, report, tracciabilità, imballaggio, programma e termini di consegna | Il preventivo basso omette prove o ambito di consegna necessari al progetto? |
Geometria: dove i minuti diventano denaro
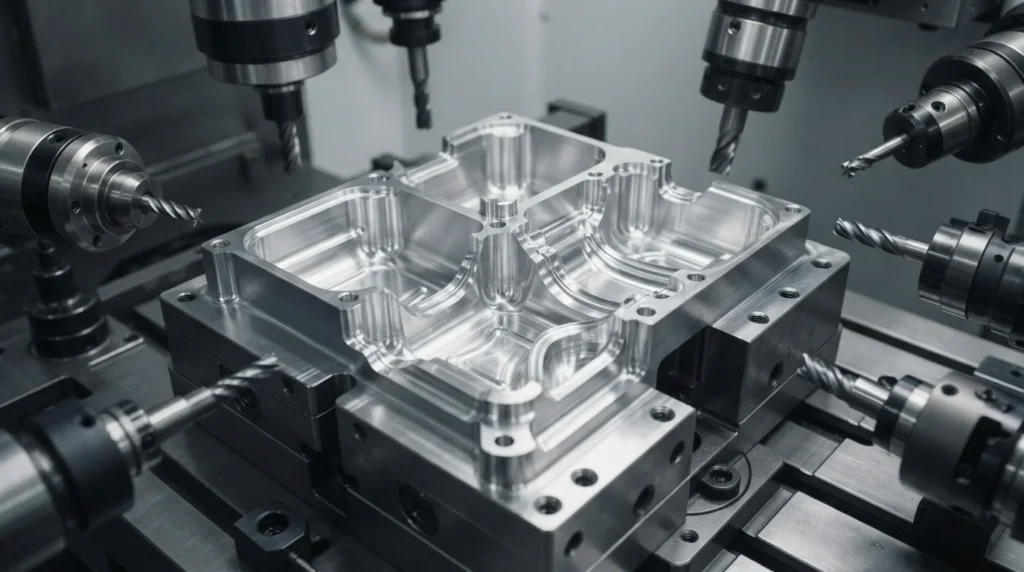
Caratteristiche che spesso aumentano il tempo di processo
- Tasche profonde o cavità strette che richiedono utensili a lunga portata e taglio più lento.
- Raggi interni molto piccoli che richiedono utensili di piccole dimensioni e passate aggiuntive.
- Pareti sottili, nervature alte o sezioni flessibili che necessitano di supporto e taglio conservativo.
- Superfici tridimensionali complesse che richiedono maggiore controllo del percorso utensile e finitura.
- Caratteristiche posizionate su molte facce, che aumentano il riposizionamento, la tastatura e il lavoro di trasferimento dei datum.
- Grandi differenze di volume tra grezzo e pezzo finito che aumentano il tempo di sgrossatura e lo scarto di materiale.
Un pezzo non diventa economico semplicemente perché il suo volume finito è piccolo. Un pezzo piccolo con accesso difficoltoso può richiedere più tempo di un pezzo più grande con geometria semplice e aperta. Chiedere al fornitore di identificare la caratteristica o la configurazione che determina la stima.
Materiale e forma del grezzo
Il materiale influisce sia sul costo diretto sia sul rischio di processo. La qualità, la tempra, la durezza, la disponibilità, la forma del grezzo e il requisito di certificazione possono modificare utensili, strategia di taglio, tempo ciclo, finitura e ispezione.
Do not compare only the raw material name
“Aluminum,” “stainless steel,” or “plastic” is not always a complete commercial specification. Different grades and conditions can have different machinability, strength, surface behavior, and availability. A certified plate, a bar, a billet, or a customer-supplied blank may lead to different yield and documentation assumptions.
Utilizzare la CNC materials library as a starting point for material-family discussions, then put the exact grade, condition, and documentation requirement in the RFQ.
Tolleranza, finitura e rischio di ispezione
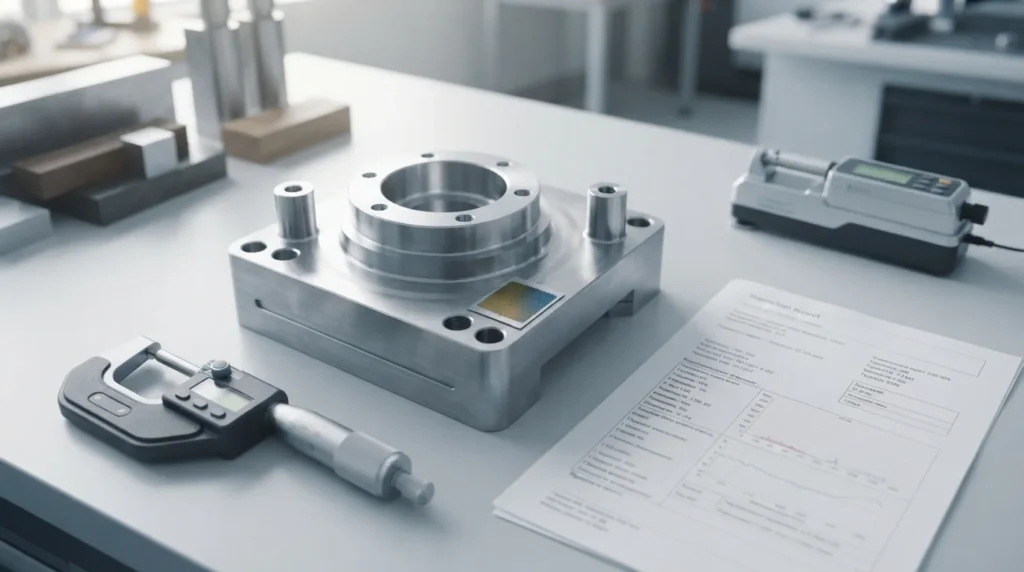
Pay for function, not habit
A useful cost review marks which features control fit, sealing, motion, alignment, load, or appearance. General features can often use a sensible general tolerance, while functional interfaces receive individual controls and an agreed inspection method. The site’s CNC tolerance guide explains how to make that distinction before tightening every dimension.
Inspection is part of the product scope
A quote for routine checks is not necessarily equivalent to one that includes a full dimensional report, material evidence, traceability, functional assembly, or special measurement conditions. State the inspection deliverables so suppliers are pricing the same acceptance burden.
Perché la quantità cambia il modello di costo
Setup, programming, fixturing, inspection planning, and material preparation are often distributed across the quantity. A one-piece prototype carries those non-recurring tasks on a single part. A repeat run can spread them across a batch, while higher volume may justify a more efficient fixture, tool strategy, inspection sampling plan, or process route.
| Project stage | Main cost concern | Useful commercial question |
|---|---|---|
| Prototype or first article | Engineering time, setup, learning, and one-time risk | Which setup or tooling costs are non-recurring? |
| Small batch | Setup allocation and material yield per part | What is the unit price at the actual quantity break? |
| Repeat production | Process repeatability, replenishment, inspection sampling, and schedule | What remains fixed, and what changes with volume or revision? |
Come confrontare equamente i preventivi CNC
- Confirm that the same drawing revision, CAD model, units, quantity, and delivery destination were quoted.
- Compare exact material grade, condition, stock form, certification, and traceability assumptions.
- Check whether tolerances, GD&T, surface roughness, finishing, deburring, cleaning, and packaging are included.
- Ask whether programming, setup, fixtures, tooling, first-article inspection, and reports are separate charges.
- Check the process route, lead-time basis, shipping terms, payment assumptions, and validity period.
- Ask what exclusions, substitutions, deviations, or engineering assumptions could change the final price.
The lowest unit price may simply represent a narrower scope. The best quote is the one whose price, quality evidence, schedule, and technical assumptions match the project’s real needs.
Un percorso DFM per ridurre i costi
Cost reduction should begin with the drawing and function, not with an arbitrary request to cut the supplier’s margin. A focused DFM review can ask:
- Can non-critical tight tolerances be relaxed without changing fit or performance?
- Can internal radii, pocket depths, wall thicknesses, or tool access be made easier to machine?
- Can several features share a datum or setup without weakening the functional design?
- Can the material grade, stock size, or finish be selected for the actual environment and appearance?
- Can inspection focus on critical characteristics instead of measuring every feature with the same burden?
- Can the quantity, batch size, or release schedule distribute setup and fixture cost more effectively?
Cost and precision are not opposites. Clearer functional priorities often allow a supplier to protect the important features while simplifying the rest of the process.
Cosa includere in una RFQ
A complete RFQ reduces uncertainty and makes quotes comparable. Include the current 2D drawing and 3D model, revision, quantity, delivery requirement, material and condition, finish, critical tolerances, GD&T, threads, inspection documents, packaging, and any regulatory or traceability requirement.
Explain the function of unusual features, the assembly interfaces, and the dimensions that cannot be changed. When the package is ready, submit it through the CNC machining quote workflow and ask the supplier to state major assumptions in the response.
Domande frequenti sui costi di lavorazione CNC
What is the biggest factor in CNC machining cost?
There is no universal single factor. Geometry, setup count, machining time, material, tolerance, finishing, inspection, quantity, and schedule risk interact. For many parts, the most useful question is which feature or requirement creates the longest or riskiest process step.
Why do two CNC suppliers quote different prices?
They may be assuming different material, setups, machines, tooling, finishing, inspection scope, lead time, packaging, or risk. A lower quote may exclude work that another supplier has included. Compare scope and assumptions before comparing totals.
Does quantity reduce CNC part price?
Often it can, because setup, programming, fixture, and first-part costs may be distributed across more parts. The actual effect depends on geometry, process stability, material yield, inspection plan, batch size, and whether the design changes between releases.
Do tight tolerances increase price?
They can increase finishing, process-control, measurement, and scrap risk. The best cost strategy is to apply tight controls only to features that need them and to define the datum and inspection method clearly.
How can I reduce CNC machining cost without reducing quality?
Use DFM to simplify tool access, internal radii, setups, stock, material, tolerances, finishing, and inspection while protecting function. Ask the supplier to identify the actual cost driver and propose a controlled alternative rather than removing requirements blindly.