
This guide organizes low-volume work around release cadence rather than a universal quantity range. It shows how to choose fixtures, inspection, inventory, and supplier controls for pilot builds, recurring small batches, service parts, and high-mix programs.
Define Low Volume by Operating Pattern
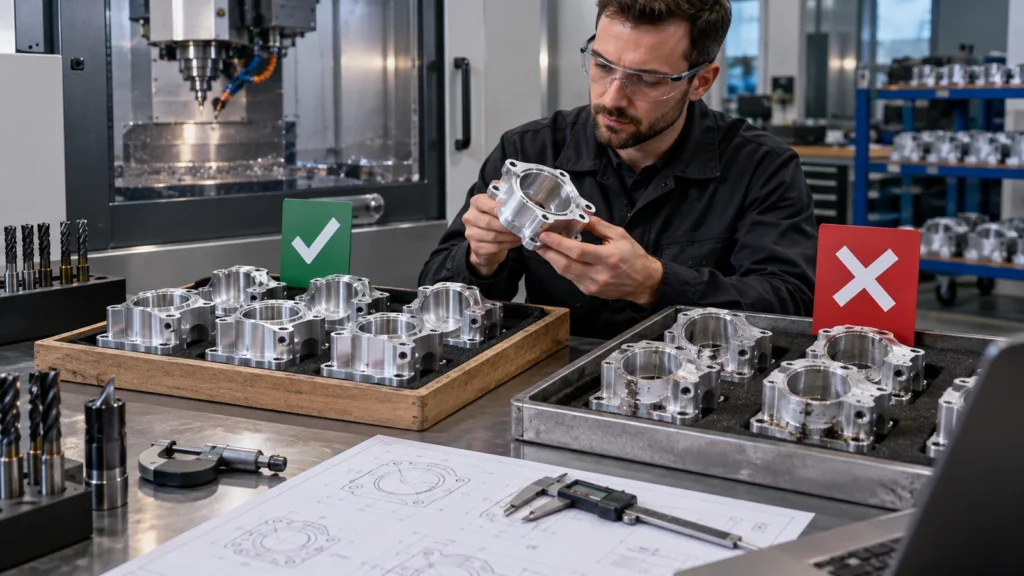 Ten complex housings released every month may require more production discipline than a one-time order for several hundred simple spacers. Define annual demand, order quantity, release frequency, product life, revision likelihood, mix of part numbers, and required response time. These factors determine how much setup knowledge must be preserved.
Classify the order as pilot, bridge, recurring production, replacement supply, or high-mix support. Each has a different reason for remaining small. That reason should influence inventory, fixture ownership, inspection, and how quickly engineering changes must be absorbed.
Release Cadence Shapes the Process More Than Annual Volume
Frequent small releases repeat setup, first-piece approval, material handling, finish batching, and administrative work. One larger release spreads those costs but increases inventory and revision exposure. Buyers should provide expected releases during quotation so suppliers can price the actual operating pattern.
| Release pattern | Main risk | Risposta di pianificazione |
|---|---|---|
| One pilot lot | Unresolved design and process learning | Capture deviations and readiness actions |
| Monthly repeat batch | Repeated setup and lot-to-lot drift | Stored fixtures, setup records, first-piece rules |
| High-mix family | Wrong revision or mixed components | Common datum strategy and strong identification |
| Service demand | Long gaps and obsolete inputs | Archive programs, gauges, material, and approvals |
Right-Size Fixture Investment
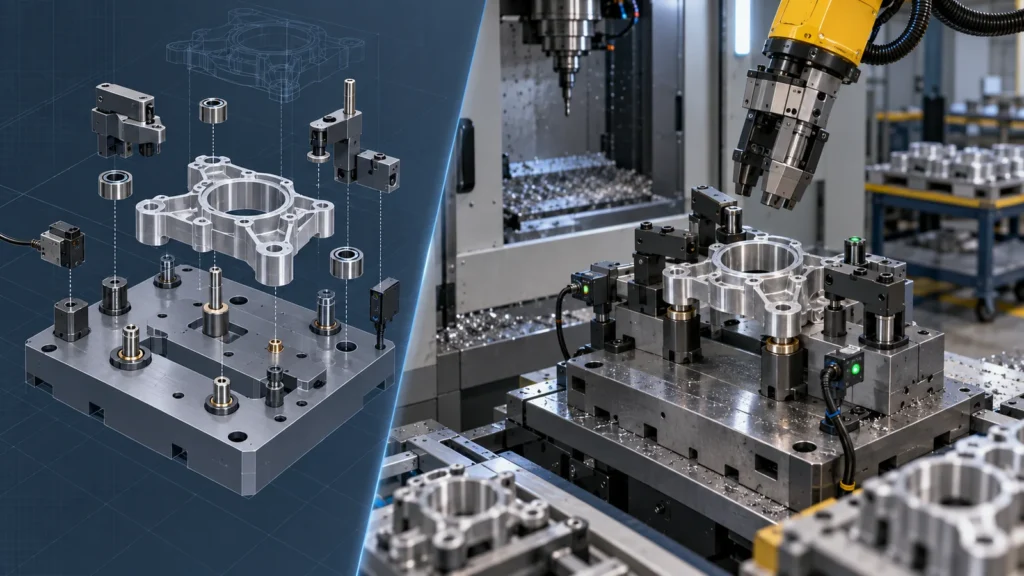 Use flexible vises and modular workholding while revisions are active. Add dedicated soft jaws, locating nests, pallets, or gauges when repeat setup time and variation justify them. The fixture does not need to be elaborate; it needs to locate consistently, support cutting forces, prevent incorrect loading, and survive the intended order life.
Document ownership, storage, maintenance, revision, and replacement. A fixture paid for in the first order has no value if it cannot be found or no longer matches the latest drawing at the next release.
For part families, a common base with changeable locators can spread investment while preserving flexibility. Review datum logic across the family before standardizing; a convenient common fixture should not force poor machining access.
A Quality Plan That Scales Down Intelligently
 Low quantity does not remove risk, but it changes how controls are applied. Identify critical characteristics, first-piece checks, in-process monitoring, final inspection, and records. A complete report on every dimension for every release may be wasteful; no documented checks may be unacceptable.
Use risk, process stability, and customer requirements to select inspection. Define how nonconforming parts are identified, segregated, and dispositioned. If a batch is small enough that one failure affects the assembly schedule, fast communication can matter more than a complex statistical plan.
The Controllo qualità CNC structure should remain consistent even when sampling and documentation are right-sized.
Materials and Outside Processes Can Set the Minimum Lot
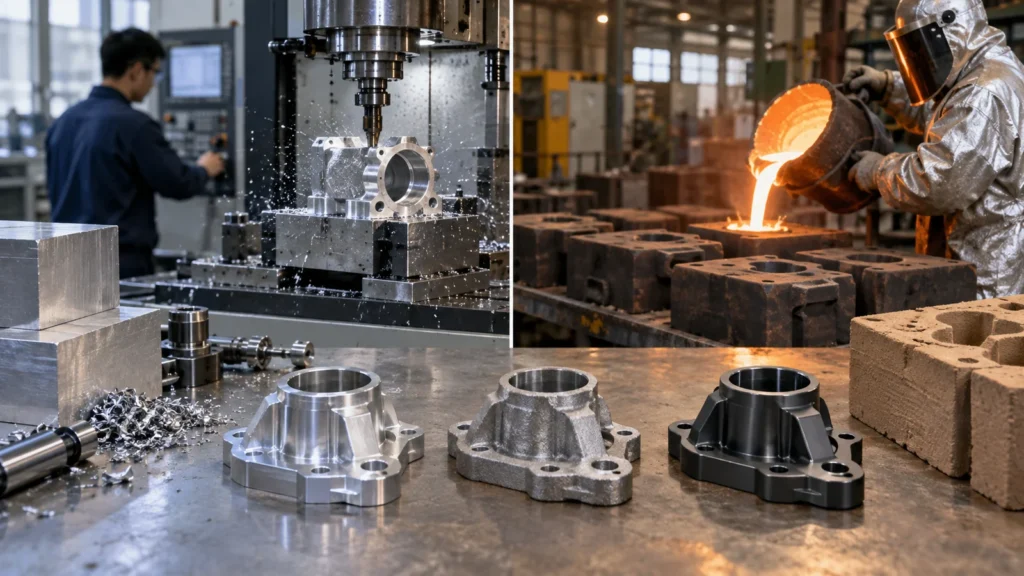 Material suppliers, heat treaters, anodizers, platers, and other processors may have minimum charges or batch schedules that dominate a small order. Buying exact material for every release can increase cost and lead time; holding stock can create cash and revision exposure.
Agree whether material can be reserved across orders, how traceability is maintained, and who owns unused stock. For finishes, define masking, color expectations, rack marks, thickness-sensitive features, and lot consistency. Mixing releases into larger finish batches may save cost but requires identification and schedule discipline.
Create Repeat-Order Memory
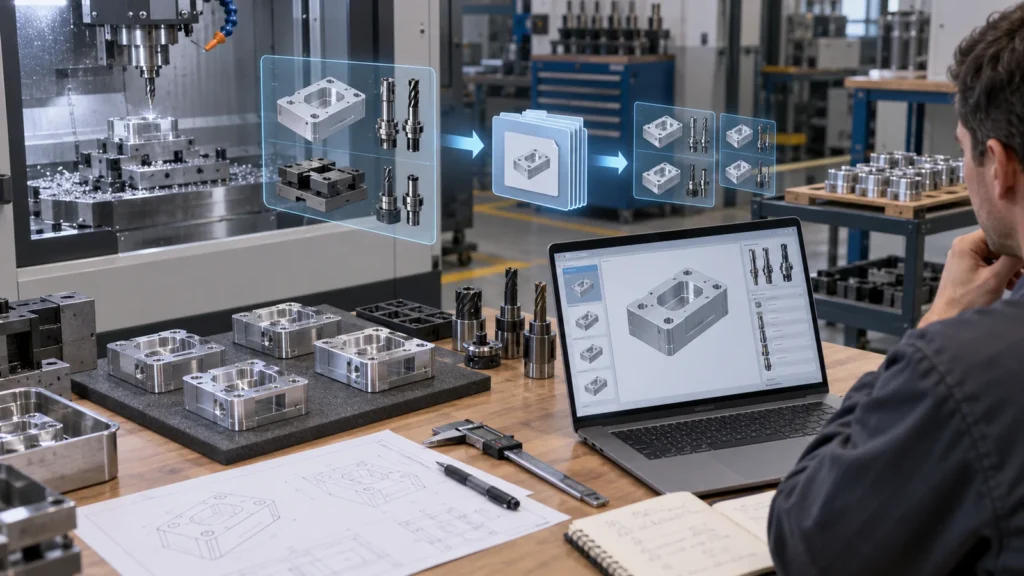 A repeat order should begin with the last approved facts: revision, material source, program, tools, fixture, setup photos, probe routine, first-piece results, finish sample, packaging, deviations, and lessons learned. Store this as a controlled job record rather than relying on individual memory.
Before launch, compare the new purchase order with the archived route. Confirm drawing revision, quantity, delivery cadence, standards, finish, inspection, and any expired material or calibration. Small changes can invalidate old fixtures or gauges even when the part number remains unchanged.
Record actual cycle, scrap, tool life, inspection effort, and delivery issues after each batch. This turns low-volume repetition into continuous improvement instead of repeated prototyping.
Cost Levers That Do Not Weaken Function
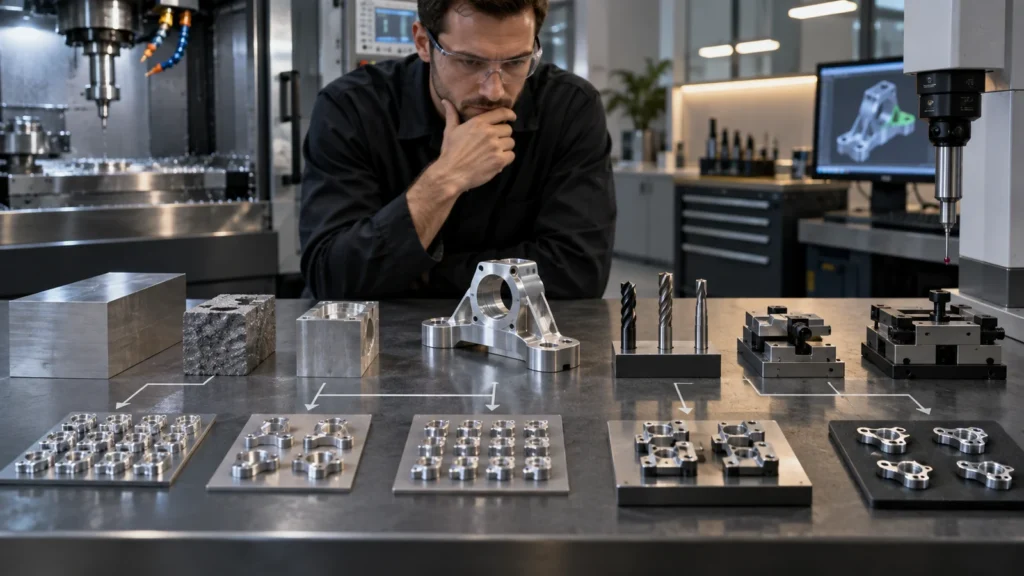
Each lever should be evaluated through the costo della lavorazione CNC model so savings are not purchased through hidden assembly or quality risk.
Low-Volume Planning Board
 Track demand horizon, next release, frozen revision, stock status, fixture status, outside processes, critical inspection, approved deviations, packaging, and open corrective actions. Assign an owner and due date to every uncertainty. The board can be simple, but it should make restart risks visible before the purchase order arrives.
Review the board when forecasts change. An order that grows may justify dedicated fixtures or a different process; a shrinking service demand may justify stocking raw material rather than finished parts. Low volume is a moving operating condition, not a permanent label.
This planning supports the parent Prototipazione e produzione CNC strategy by preserving flexibility without sacrificing repeatability.
Small-Batch FAQs
Is low-volume CNC always more expensive per part?
It often carries more setup cost per unit, but total economics depend on geometry, release pattern, fixture reuse, material, finish, inspection, and the avoided tooling or inventory of another process.
Should every repeat batch receive a first article?
Some form of first-piece verification is prudent after setup. The required report and approval level depend on risk, customer requirements, changes, and process history.
Who should own dedicated fixtures?
Ownership should be explicit. Also define storage, maintenance, access, transfer rights, revision control, and disposition at program end.
Can low-volume production use prototype programs?
Yes, after review. Validate revision, setup, toolpaths, compensation, inspection, and repeatability rather than assuming a program that made one good part is production-ready.