
Quando gli ingegneri iniziano a lavorare parti in PMMA, la prima domanda è spesso semplice: “Il fornitore è in grado di mantenere le dimensioni?” In pratica, questa è solo una parte della sfida. Un componente in PMMA può superare l'ispezione dimensionale e comunque risultare difettoso perché i bordi sono opachi, un foro praticato sviluppa una crepa, una superficie lucidata mostra distorsioni, oppure le sollecitazioni residue di lavorazione causano craquelure dopo il montaggio.
Il PMMA, comunemente chiamato acrilico, può essere un materiale eccellente per involucri trasparenti, coperture ottiche, guide di luce, finestre di ispezione, componenti per display, parti per apparecchiature medicali e prototipi di precisione. Combina trasparenza, rigidità, stabilità ai raggi UV, basso peso e buona lavorabilità. Tuttavia, non si comporta come l'alluminio, il POM o il policarbonato durante il taglio CNC.
La decisione di acquisto, quindi, non dovrebbe concentrarsi solo sulla macchina CNC. Grado del materiale, geometria dell'utensile, gestione del calore, attrezzaggio, strategia dei percorsi utensile, finitura, ispezione, imballaggio ed esperienza del fornitore possono tutti influenzare il risultato finale.
Questa guida esamina la lavorazione del PMMA dal punto di vista dell'acquirente. Spiega cos'è il PMMA, come funziona la lavorazione CNC con l'acrilico, perché le parti trasparenti a volte diventano bianche o si crepano, quali tolleranze sono realistiche, come valutare i fornitori e quando il PMMA può essere una scelta migliore rispetto al policarbonato o ad altre plastiche tecniche.
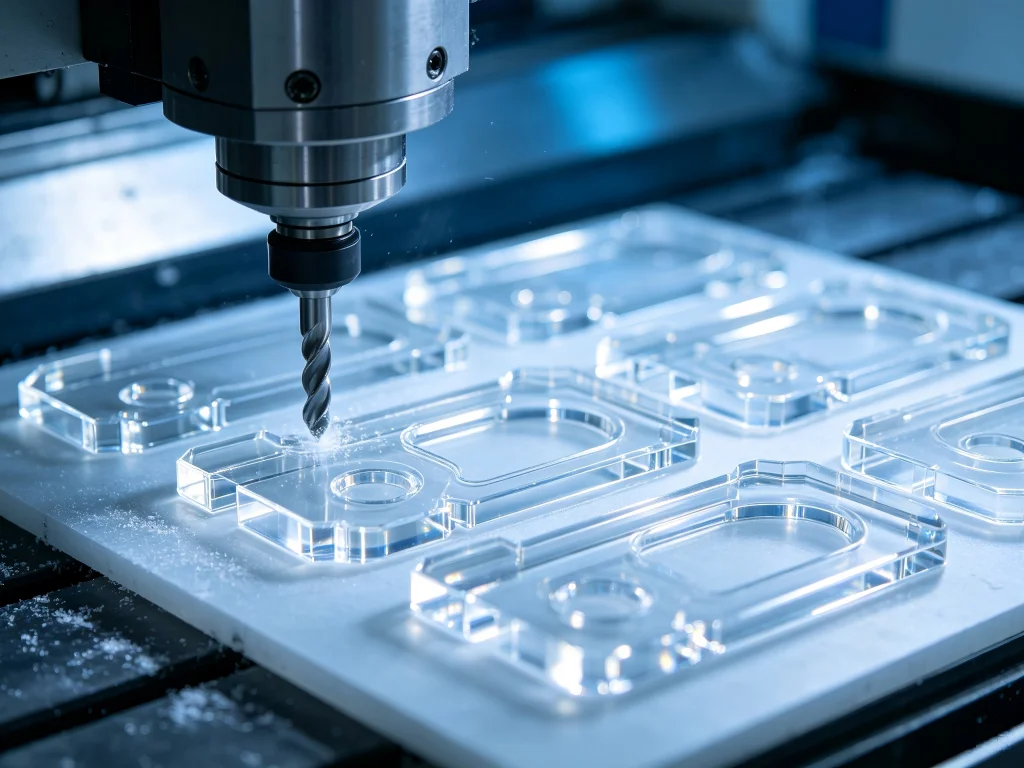
Cos'è il PMMA e perché viene lavorato con CNC?
PMMA sta per polimetilmetacrilato. È un termoplastico trasparente ampiamente noto attraverso termini e nomi commerciali come acrilico, vetro acrilico, Plexiglas, Perspex e Lucite.
La sua combinazione di aspetto ottico e rigidità meccanica rende il PMMA particolarmente utile quando un componente deve essere sia funzionale che visivamente pulito. A differenza del vetro comune, il PMMA può essere fresato, forato, tornito, inciso, filettato, lucidato e formato utilizzando attrezzature di produzione comunemente associate alla lavorazione di metalli e plastiche.
Per gli ingegneri di prodotto, questo crea un vantaggio importante. Un componente trasparente non necessita sempre di uno stampo.
Un produttore potrebbe lavorare un prototipo, venti componenti di validazione o un lotto di produzione a basso volume direttamente da barre di PMMA. Le revisioni di progetto possono quindi essere introdotte tramite modifiche CAD e CAM invece che con costose modifiche allo stampo.
Le ragioni comuni per cui gli ingegneri specificano l'acrilico lavorato includono:
- È richiesta un'elevata trasparenza ottica.
- Il componente necessita di una migliore stabilità ai raggi UV rispetto a molte comuni plastiche trasparenti.
- La produzione a basso volume rende difficile giustificare lo stampaggio a iniezione.
- Il progetto contiene tasche, fori, canali, svasature, filettature o caratteristiche di montaggio di precisione.
- Un prototipo trasparente deve rappresentare fedelmente il design di produzione finale.
- Il componente necessita di una superficie estetica ad alta lucidità o lucidata.
- I team di ingegneria necessitano di iterazioni di progetto rapide prima dell'investimento in attrezzature.
Il PMMA è particolarmente attraente quando l'aspetto è importante. Un grado acrilico opportunamente selezionato e finito potrebbe produrre un aspetto premium simile al vetro rimanendo al contempo più facile da lavorare in geometrie complesse.
La distinzione importante: lavorabile non significa facile
L'acrilico è spesso descritto come facile da lavorare. Questa affermazione necessita di contesto.
Il PMMA può essere tagliato in modo pulito con utensili affilati, ma la finestra di lavorazione è diversa da quella utilizzata per i metalli. Il materiale ha una conduttività termica relativamente bassa rispetto ai metalli. Il calore generato attorno al tagliente non si dissipa rapidamente attraverso il pezzo.
Se il processo di taglio genera calore eccessivo, il materiale attorno all'utensile può ammorbidirsi. I trucioli possono iniziare ad aderire al tagliente. L'utensile contaminato genera quindi attrito aggiuntivo. Più attrito produce più calore, e il problema può accelerare rapidamente.
Il risultato può includere bordi fusi, pareti opache, superfici sbavate, errori dimensionali o utensili da taglio rotti.
Ecco perché i fresatori esperti di plastica spesso ragionano in termini di formazione del truciolo piuttosto che semplicemente di velocità massima del mandrino.
L'obiettivo è tagliare il polimero in modo pulito e rimuovere sia il truciolo sia gran parte del calore generato prima che uno dei due possa danneggiare la superficie.
Perché i problemi di lavorazione del PMMA di solito iniziano con il calore
Immagina che un ingegnere degli acquisti riceva due preventivi visivamente simili.
Il Fornitore A propone parametri di lavorazione aggressivi e promette una produzione molto rapida. Il Fornitore B propone un'operazione di sgrossatura controllata seguita da passate di finitura dedicate e lucidatura aggiuntiva per le superfici ottiche.
Il primo preventivo può sembrare più economico.
Tuttavia, l'economia della lavorazione del PMMA non può sempre essere misurata solo dal tempo ciclo.
Quando il calore si accumula attorno alla zona di taglio, possono verificarsi diversi problemi:
- i trucioli possono risaldarsi sulla superficie lavorata;
- il filo di taglio può sviluppare accumuli plastici;
- le caratteristiche sottili possono deformarsi;
- la rugosità superficiale può aumentare;
- le sollecitazioni interne possono diventare più significative;
- i fori possono presentare cricche locali;
- le pareti trasparenti possono diventare opache;
- la lucidatura successiva può richiedere molto più lavoro.
Un ciclo di taglio più rapido che genera dieci pezzi scartati non è una produzione più rapida.
Una buona lavorazione del PMMA bilancia quindi velocità del mandrino, carico del truciolo, geometria dell'utensile, velocità di avanzamento, profondità di taglio, strategia di raffreddamento, rigidità della macchina, attrezzatura di fissaggio e geometria del pezzo.
PMMA colato vs PMMA estruso: una decisione d'acquisto che conta
One of the first questions a CNC supplier should ask is not “How many pieces?” It should be “Which PMMA grade and stock form does the application require?”
Cast and extruded acrylic can behave differently during machining.
Cast PMMA is often preferred for demanding machining and cosmetic applications because it may provide favorable machining behavior and lower sensitivity to certain stress-related problems. Extruded material can offer advantages in thickness consistency and cost for appropriate applications.
Neither should automatically be described as universally superior.
The correct selection depends on dimensional requirements, optical requirements, stock thickness, geometry, finishing process, volume, and cost target.
When Cast Acrylic May Be Preferred
Cast PMMA may be considered when a project places strong emphasis on machining quality, thicker sections, polished edges, detailed features, or optical appearance.
It can be a practical option for:
optical prototypes, transparent manifolds, display blocks, instrument windows, laboratory components, light guides, premium enclosures, inspection fixtures, and complex clear machined components.
When Extruded Acrylic May Make Sense
Extruded PMMA could make economic sense for applications involving relatively simple geometry, controlled sheet thickness, high material utilization, or projects where the design and machining process have already been validated for that stock.
A buyer should therefore avoid specifying only “clear acrylic.”
A more useful RFQ identifies the grade, stock form, transparency requirement, color if applicable, thickness, dimensional requirements, cosmetic surface requirements, and any environmental exposure.
PMMA vs Polycarbonate vs POM: Which Material Should You Buy?
PMMA is not automatically the best plastic simply because a component needs to be transparent. Polycarbonate may be preferable when impact resistance dominates the design. POM may be preferable when transparency is unnecessary but dimensional stability, wear behavior, and mechanical function matter.
| Decision Factor | PMMA / Acrylic | Policarbonato | POM / Acetal |
|---|---|---|---|
| Transparency | Excellent; often selected for optical and cosmetic parts | Very good | Generally opaque |
| Visual Appearance | Excellent polished appearance | Buono | Primarily functional |
| Impact Resistance | Moderate and relatively brittle | Much higher; often preferred for impact | Good mechanical durability |
| UV/Outdoor Potential | Generally strong | Grade dependent | Grade dependent |
| CNC Machinability | Good with correct plastic-machining strategy | Good but heat management remains important | Eccellente |
| Optical Components | Strong candidate | Useful where toughness is important | Not appropriate for transparency |
| Polished Clear Finish | Excellent potential | Possible | Not normally relevant |
| Stress/Cracking Concern | Requires careful machining and finishing | Generally tougher but chemically sensitive in some environments | Usually less brittle |
| Typical Buying Priority | Clarity + appearance + precision | Transparency + impact strength | Mechanical performance + dimensional function |
The comparison highlights a useful purchasing principle: material selection should begin with failure mode.
If the most unacceptable failure is optical distortion or poor appearance, PMMA could be attractive. If the unacceptable failure is impact fracture, polycarbonate may deserve greater consideration. If the component is an internal mechanical element and transparency provides no value, another engineering plastic could be more economical.
How CNC Machining PMMA Actually Works
The basic CNC process appears similar to machining other plastics. CAD geometry defines the component. CAM software converts that geometry into toolpaths. The CNC controller moves cutting tools relative to the workpiece to remove material.
What changes is the process strategy.
1. Material Preparation
Raw PMMA stock should first be verified against the drawing and purchase specification. Thickness, grade, color, surface condition, and protective masking may need confirmation before machining begins.
Material handling matters more for clear parts than many buyers expect. A scratch created before the CNC cycle may remain visible after the part has been completed.
Protective film may therefore remain on suitable surfaces during early processing where the manufacturing sequence allows it.
2. Workholding
PMMA needs secure support, but excessive clamping pressure can be counterproductive.
A metal component may tolerate significant vise pressure. A clear acrylic component could develop localized stress or cosmetic damage when held incorrectly.
Depending on geometry, the machining strategy may use soft jaws, vacuum fixtures, sacrificial plates, custom fixtures, low-distortion clamping, or combinations of these methods.
Thin sheet components deserve particular attention because poor support may permit vibration or lifting during machining.
3. Rough Machining
Roughing removes most unwanted material while leaving controlled stock for final finishing where required.
The objective is not simply maximum material removal.
Toolpaths should support efficient chip evacuation and prevent repeated cutting of hot chips. A chip that remains in the cutting zone can be cut again, adding unnecessary heat and potentially damaging the surface.
4. Finish Machining
A dedicated finishing operation may dramatically improve dimensional control and cosmetic appearance.
Rather than forcing one cutting pass to perform roughing and finishing simultaneously, the process could leave a small, controlled allowance. A sharp finishing tool then removes that material under more stable conditions.
This approach can be especially valuable for visible edges, sealing surfaces, precision pockets, light-guiding surfaces, and components that will receive secondary polishing.
5. Deburring and Edge Treatment
PMMA parts may require careful deburring after CNC processing. Aggressive hand finishing can introduce scratches, rounded edges, or inconsistent geometry.
The deburring method should therefore reflect the drawing requirements.
A hidden mechanical edge and an optically visible edge should not automatically receive the same treatment.
6. Inspection
Inspection should verify more than dimensions when appearance is part of the specification.
A practical inspection plan may include dimensional checks, thread verification, visual inspection, surface requirements, transparency evaluation, cosmetic zones, and packaging inspection.
The Tooling Question: Why Cutter Geometry Matters
Machinists discussing acrylic frequently return to one subject: sharp tools.
That makes sense because PMMA responds poorly when the tool rubs instead of cuts.
Tool geometry designed for efficient plastic cutting could provide better chip formation and evacuation than a general-purpose cutter selected without considering the polymer.
Single-flute or O-flute cutters are frequently considered for acrylic machining because their open geometry provides room for chips to escape. Depending on the feature and finish requirement, polished carbide tooling or specialized finishing cutters may also be appropriate.
For highly demanding optical surfaces, specialized diamond tooling could be considered.
The important point for buyers is not to dictate one universal cutter.
Instead, ask the supplier how tooling changes between roughing, finishing, drilling, engraving, and optical-surface operations.
A supplier that treats every PMMA feature with the same generic end mill may have difficulty achieving repeatable cosmetic quality.
RPM Is Only Half the Story
One of the most common questions online is: “What RPM should I use for acrylic?”
There is no single correct number.
The appropriate spindle speed depends on cutter diameter, flute count, tool geometry, feed rate, depth of cut, machine rigidity, coolant or air strategy, material grade, and desired finish.
This explains why copying another shop’s spindle setting may fail.
A small desktop router and a rigid industrial machining center cannot necessarily use the same parameters even if both are cutting PMMA.
The more useful concept is chip load.
If feed is too low relative to spindle speed, the cutter may rub or create very small chips. Heat rises. The polymer can soften and stick to the cutter.
If the cutting load becomes excessive, however, brittle edges may chip or a small tool could fail.
Stable PMMA machining exists between these extremes.
That balance should be developed through process knowledge and validated machining parameters rather than an arbitrary “maximum RPM” rule.
Why PMMA Turns White During CNC Machining
Cloudy or milky surfaces are among the most frustrating defects in transparent acrylic components.
The root cause could involve several mechanisms rather than one simple problem.
Possible contributors include excessive cutting heat, rubbing, dull tooling, poor chip evacuation, unsuitable cutting geometry, excessive vibration, heavy roughing marks, or stress introduced during machining.
The corrective strategy therefore begins with diagnosis.
If material is visibly melting, thermal management deserves immediate attention. If the edge contains regular tool marks but no melting, finishing parameters and cutter geometry may deserve more attention. If cracks appear later rather than immediately, residual stress and chemical exposure should also be investigated.
In other words, “polish it more” is not always the right solution.
A polished surface cannot reliably compensate for an unstable machining process.
Preventing Chipped Edges
Chipping often occurs where a cutter enters or exits an unsupported acrylic edge.
This can be particularly troublesome around thin walls, narrow tabs, drilled exits, and outside contours.
The CAM strategy could therefore control where and how the tool enters and exits the component.
Practical approaches may include maintaining better material support, changing toolpath direction where validated, adjusting entry and exit motion, reducing finishing load, leaving sacrificial material, or separating rough and finish operations.
The important purchasing lesson is that edge quality is not determined only by the nominal tolerance on the drawing.
If an edge is optically visible, tell the supplier.
A machinist cannot infer every cosmetic requirement from a STEP model.
Drilling PMMA Without Creating Future Cracks
Acrylic drilling deserves its own process planning.
Heat can accumulate around the drill. Breakthrough can create chipping. Poor tool geometry may place excessive stress around the hole. Tight fasteners can then add assembly stress.
A hole that looks acceptable immediately after manufacturing may therefore become a failure point later.
Designers should consider hole diameter, wall thickness around the hole, edge distance, countersink geometry, fastener load, inserts, and the chemical environment of the final assembly.
If the component will be repeatedly fastened and removed, relying on a small directly machined plastic thread may not always be the best long-term design.
A metal threaded insert or different fastening concept could provide better serviceability depending on load and geometry.
What Tolerance Should You Specify?
This is one area where buyers can accidentally increase cost without improving product performance.
A drawing that places extremely tight tolerances on every PMMA dimension forces the supplier to treat noncritical features like precision interfaces.
That may increase machining time, inspection effort, scrap risk, and price.
Instead, divide dimensions according to function.
A bearing location, optical alignment feature, sealing surface, assembly interface, or precision locating hole may justify tighter control. An external cosmetic profile may not.
PMMA is still a polymer. Temperature and internal stress can influence dimensions differently than they would in a stable metal component.
The right tolerance is therefore the tolerance the assembly actually needs.
JUCHENG publishes a general machining tolerance of ±0.005 inch (±0.127 mm) for most features and states that ±0.001 inch (±0.025 mm) or better may be possible depending on material and geometry. For a PMMA project, the achievable value should still be reviewed against individual geometry rather than copied automatically into every drawing dimension.
Design for Manufacturability: Make the Acrylic Part Easier to Produce
Good CNC results begin before material reaches the machine.
Several design decisions can reduce manufacturing risk.
- Avoid unnecessarily thin walls. Thin acrylic walls may vibrate or deflect during machining and can be more vulnerable during handling.
- Use practical internal corner radii. CNC end mills naturally create radiused internal corners. Specifying impossible sharp internal corners could require additional processes.
- Separate functional and cosmetic tolerances. Apply precision where the assembly needs it.
- Identify optical surfaces on the drawing. “Clear PMMA” does not define the required surface finish.
- Consider tool access. Deep narrow pockets and extreme aspect ratios could require long tools, which may reduce rigidity.
- Review hole-to-edge distances. Fragile geometry around holes can increase cracking risk.
- Specify thread function. The supplier needs to know whether threads are temporary prototype features or repeated-use production interfaces.
- Define cosmetic zones. A visible front face and hidden mounting surface may need very different finishing standards.
These steps could lower cost while improving consistency because the supplier can concentrate process control where it creates actual product value.
Surface Finish: “Transparent” Is Not a Finish Specification
This distinction causes many sourcing problems.
PMMA stock may arrive transparent, but a CNC tool physically removes material. The newly machined surface can therefore show tool marks even though the underlying polymer remains transparent.
Different finishing levels should be discussed during quotation.
As-Machined PMMA
An as-machined surface may retain visible cutter patterns. It can be perfectly acceptable for hidden mounting features, internal pockets, fixtures, engineering prototypes, and functional components where optical appearance is not required.
This is usually the most economical option because secondary polishing is minimized.
Mechanically Polished PMMA
Mechanical finishing can progressively reduce machining marks and improve clarity. The process may involve controlled abrasive stages followed by polishing compounds.
The method is useful for many cosmetic surfaces but must be controlled carefully around dimensional features.
Polishing removes material. Therefore, a surface cannot always be machined exactly to final size and then heavily polished without considering dimensional change.
Flame Polishing
Flame polishing can rapidly improve certain exposed acrylic edges by briefly heating the surface.
However, it should not be treated as a universal solution.
The thermal process may introduce stress and may not be suitable for every precision, bonded, chemically exposed, or safety-sensitive component.
Engineering review should determine whether it is appropriate for the specific application.
Diamond Finishing
For demanding transparent surfaces, specialized diamond tooling can create extremely fine finishes directly through controlled cutting.
This approach may reduce the amount of conventional polishing required, although cost, geometry, equipment, and optical specifications must justify it.
Optical Quality Needs Its Own Conversation
A buyer asking for “clear acrylic” and a buyer asking for an optical component are not necessarily requesting the same product.
A transparent machine guard only needs adequate visibility. A light guide may require controlled light transmission. A sensor window may need consistent optical behavior. A laboratory microfluidic component may need transparent channels. An imaging component may require much stricter surface and geometric control.
Optical applications could require discussion of:
surface roughness, flatness, parallelism, tool marks, polishing method, distortion, transparency, inspection lighting, scratches, edge quality, stress, and acceptable cosmetic defects.
The more optical the application becomes, the less useful a simple dimensional drawing becomes by itself.
Applications Where CNC Machined PMMA Makes Sense
Lighting and Optical Systems
PMMA is widely associated with light transmission applications. CNC machining allows engineers to produce light guides, LED covers, lens-related components, optical mounts, transparent panels, and prototype lighting structures without waiting for dedicated molds.
This can be particularly valuable during optical development because engineers may revise geometry several times before production.
Medical and Laboratory Equipment
Transparent components can allow users to observe fluids, mechanisms, indicators, or internal assemblies.
Potential applications include laboratory fixtures, instrument covers, prototype fluidic components, transparent housings, inspection windows, and equipment panels.
Material suitability should always be validated against sterilization, chemical exposure, regulatory, and biocompatibility requirements rather than assuming that all acrylic grades are interchangeable.
Automotive Development
Automotive engineering teams may use PMMA for lighting prototypes, transparent covers, display components, test fixtures, interior development parts, and visual validation models.
Low-volume CNC production can be useful before injection molding or dedicated tooling is finalized.
Electronics and Instrumentation
Transparent windows, display covers, control panels, sensor housings, indicator components, and prototype enclosures can all benefit from acrylic’s appearance.
CNC machining also permits holes, pockets, mounting bosses, channels, and connector features to be incorporated directly into the component.
Industrial Equipment
Machine windows, inspection covers, transparent guards, measuring fixtures, flow observation components, and prototype housings are common engineering concepts for clear plastics.
Where impact hazards are significant, however, PMMA should be compared carefully with tougher alternatives such as polycarbonate.
Prodotti di consumo
Acrylic can create a premium appearance in display components, lighting products, decorative hardware, electronic products, retail fixtures, and high-end enclosures.
Here cosmetic inspection may be just as important as dimensional inspection.
A Practical PMMA CNC Case: From Cloudy Prototype to Production-Ready Part
Consider a hypothetical but representative engineering project.
A product developer needs a transparent sensor housing with several mounting holes, a shallow internal pocket, a display window, and polished outside edges.
The first prototype is machined aggressively using parameters originally developed for aluminum-like production logic.
Dimensions appear acceptable, but several problems emerge.
The pocket surface is cloudy. One edge contains small chips. Tool marks remain visible after basic polishing. Two holes show stress marks after screws are tightened.
The natural reaction might be to increase polishing.
That would treat symptoms rather than the manufacturing system.
A stronger corrective plan could begin with reviewing the PMMA grade and stock condition. The supplier could then examine workholding pressure, select plastic-appropriate sharp tooling, revise chip evacuation, separate roughing from finishing, control tool entry and exit around visible edges, and review the mounting-hole design.
The final polishing operation could then begin from a much better machined surface.
This distinction matters economically.
Producing a poor surface quickly and spending significant labor repairing it may cost more than machining the surface correctly in the first place.
Installation of Precision PMMA Components
Installation may seem unrelated to CNC machining, yet assembly practices can determine whether a well-machined component survives.
Acrylic components should generally be installed without forcing misaligned features into position. Fasteners should not automatically be tightened using torque values developed for metal housings.
Washers, compliant interfaces, shoulder screws, inserts, or controlled fastening methods may help distribute load depending on the design.
Designers should also consider thermal expansion when a large PMMA component is constrained by a metal frame.
If the plastic wants to expand while the frame prevents movement, stress may accumulate around fasteners or sharp internal features.
Clearance and mounting strategy should therefore reflect the expected temperature range.
Maintenance: Keeping Machined Acrylic Clear
A beautifully polished PMMA component can be damaged by poor cleaning practices.
Routine maintenance should use cleaning products known to be compatible with the selected acrylic grade.
Abrasive cleaning materials may scratch polished surfaces. Certain solvents and aggressive chemicals may contribute to crazing or chemical attack, particularly where residual stress exists.
For critical applications, the cleaning chemistry should be validated before production deployment.
Maintenance documentation may also specify suitable cloths, cleaning agents, inspection frequency, fastening checks, and replacement criteria.
How to Read a Machining PMMA Parts PDF
Engineers searching for a machining PMMA parts PDF are often looking for feeds and speeds. A useful technical document should contain more than a parameter table.
Look for information covering material type, cast versus extruded stock, tool geometry, drilling, sawing, milling, turning, cooling, chip removal, annealing where relevant, polishing, forming, and handling.
Processing guides from established acrylic manufacturers can be useful starting references because they explain how the polymer behaves rather than presenting a universal CNC recipe.
However, published parameters should still be treated as starting points.
The final machining window needs to account for the actual CNC machine, cutter, workholding, geometry, stock, finish requirement, and production environment.
What Reddit Machinists Reveal About Real PMMA Problems
Technical manuals explain the theory. Shop-floor discussions reveal where users repeatedly struggle.
Across CNC communities, several themes appear again and again.
One is melting. Operators often discover that simply increasing spindle speed does not solve the problem. If feed, cutter geometry, and chip evacuation are poorly matched, more spindle speed may generate more heat rather than better cutting.
Another recurring theme is tool sharpness. Users working successfully with acrylic frequently emphasize sharp cutters and tooling suitable for plastics.
Chip evacuation is another major topic. Airflow is often discussed because clearing chips from the cutting zone can reduce recutting and help control heat.
Surface clarity is also a frequent source of confusion. Machinists sometimes expect an ordinary milling operation to leave an optical surface. In reality, demanding optical finishes may require dedicated finishing passes, specialized cutters, polishing, or advanced diamond-machining techniques.
These discussions reinforce a central point of this guide: PMMA quality is created by the complete process, not by one RPM setting.
What Buyers Should Ask a PMMA CNC Supplier
Price per part matters, but it should come after process capability.
A useful supplier evaluation starts with evidence.
Ask whether the supplier routinely machines engineering plastics rather than primarily machining metal. Ask how cast and extruded PMMA are selected. Ask what strategy is used to control heat and chips. Ask whether roughing and finishing tools can be separated. Ask how transparent cosmetic surfaces are inspected.
Then examine equipment and quality infrastructure.
A supplier handling complex geometry may need multi-axis machining. A high-volume project may require enough machine capacity to avoid unstable delivery schedules. Tight-tolerance assemblies need suitable measurement systems. Automotive and medical projects may require structured quality management and traceability.
Finally, ask how the company manages engineering communication.
PMMA projects benefit from DfM feedback because problems such as thin walls, deep pockets, tiny internal radii, fragile holes, and unrealistic optical specifications are much cheaper to correct before machining begins.
Why JUCHENG for CNC Machined PMMA Components?
JUCHENG approaches PMMA projects as precision manufacturing programs rather than simple plastic cutting jobs.
The company has more than 13 years of precision manufacturing experience and operates an approximately 8,000-square-meter manufacturing facility. Its equipment base includes more than 150 CNC machines and over 25 advanced 5-axis machining centers.
That equipment range can support both straightforward acrylic components and more complicated parts containing multi-face geometry, precision pockets, holes, complex contours, and tight assembly relationships.
Engineering Support Before Cutting
JUCHENG provides Design for Manufacturability feedback during quotation.
This matters with PMMA because geometry affects process risk. Engineers can review thin walls, hole locations, internal radii, machining access, cosmetic surfaces, tolerances, and finishing requirements before production.
Reducing manufacturing risk at the CAD stage may be more effective than attempting to compensate for an unsuitable design on the machine.
3-, 4- and 5-Axis CNC Capability
JUCHENG’s manufacturing platform includes 3-axis and 4-axis milling, simultaneous 5-axis machining, CNC turning, turn-mill machining, EDM, precision grinding, and related precision processes.
For PMMA, multi-axis capability can be useful when a component contains features on several faces. Reducing unnecessary setups may improve geometric relationships between features while also reducing handling of sensitive transparent surfaces.
Large Manufacturing Capacity
With more than 150 CNC machines, JUCHENG can support rapid prototypes as well as larger production requirements.
This matters to purchasing teams that want one supplier to support the product from engineering validation into repeat production.
A prototype-only supplier may perform well for five pieces but struggle when the requirement becomes hundreds or thousands of components. Production planning should therefore consider future volume before supplier qualification.
Quality Management for Demanding Industries
JUCHENG publishes certifications including ISO 9001:2015, IATF 16949, ISO 13485, and ISO 14001.
IATF 16949 supports the disciplined process approach expected in automotive supply chains, while ISO 13485 provides a quality-management framework relevant to medical device manufacturing. ISO 9001 supports systematic quality control across broader manufacturing operations.
Certification alone does not guarantee that every PMMA part will meet every application requirement. It does, however, provide buyers with evidence that structured quality systems exist behind the machining operation.
Advanced Inspection
JUCHENG uses Zeiss CMM equipment as part of its precision inspection capabilities.
For acrylic components with critical mounting patterns, precision pockets, geometric relationships, or assembly interfaces, suitable dimensional verification can be just as important as CNC machine capability.
Inspection requirements should be defined during quotation so the manufacturing and quality teams understand which dimensions are critical.
Dal prototipo alla produzione
JUCHENG’s published workflow begins with CAD submission, followed by quotation and DfM review, machining and quality control, then final inspection and delivery.
Standard prototype lead times published by the company are approximately 5–10 business days depending on material availability and complexity, with expedited projects potentially available in roughly 3–5 business days. Production schedules depend on quantity and complexity.
This structure can be useful for product teams that need to validate transparent prototypes before committing to a larger manufacturing program.
How to Prepare an RFQ for Machined PMMA
A strong quotation package can prevent several rounds of email and reduce the risk of suppliers interpreting requirements differently.
Start with a 3D CAD model, preferably STEP or another widely supported solid-model format. Add a 2D drawing for tolerances, threads, critical dimensions, inspection requirements, and cosmetic notes.
Specify PMMA grade where known. If the grade is not fixed, explain the application and allow the manufacturing engineer to recommend alternatives.
Identify every optically or cosmetically important surface.
Define whether the requirement is simply transparent, visually polished, or genuinely optical.
Include quantity for both the immediate order and expected future volume. Ten prototype pieces and 10,000 annual production pieces may justify different fixtures and process strategies.
Finally, describe the operating environment.
Temperature, UV exposure, cleaning chemicals, impact risk, fastening method, and mating materials may influence whether PMMA is actually the correct material.
Cost Drivers in PMMA CNC Machining
Material cost is only one part of the final quotation.
Machine time increases with deep pockets, complex 3D surfaces, small cutters, multiple setups, and tight tolerances.
Polishing can become a major cost driver because achieving transparent cosmetic surfaces often requires more labor than producing an ordinary functional plastic component.
Inspection requirements also influence cost. Measuring every feature on every component costs more than sampling a few critical dimensions.
Low-volume prototypes may carry higher setup cost per piece, while larger quantities can distribute programming, fixturing, and process-development costs across more parts.
Buyers seeking lower prices should therefore look first at design simplification rather than automatically changing suppliers.
Increasing an unnecessary internal radius, relaxing a noncritical tolerance, reducing polishing areas, simplifying setups, or using standard stock thicknesses could lower cost without changing the function of the product.
Common PMMA Machining Mistakes Buyers Can Prevent
The first mistake is purchasing based only on the lowest quotation.
A low unit price can become expensive if the parts arrive with cracks, cloudy surfaces, inconsistent dimensions, or unacceptable scratches.
The second mistake is failing to define cosmetic quality.
Terms such as “clear,” “nice finish,” and “no scratches” are subjective. Drawings, samples, limit samples, photographs, or agreed inspection criteria can make expectations measurable.
The third mistake is over-tolerancing.
Tight tolerances should protect function, not decorate drawings.
The fourth mistake is treating PMMA like metal.
Workholding, cutting parameters, thermal behavior, deburring, and polishing require a plastic-specific approach.
The fifth mistake is ignoring the assembly.
A perfectly machined acrylic part can still crack when a fastener creates excessive local stress or an incompatible chemical contacts a stressed surface.
FAQ About CNC Machining PMMA Parts
Is PMMA easy to CNC machine?
PMMA has good machinability, but achieving clear, dimensionally stable surfaces requires correct tooling and process control. Sharp cutters, effective chip evacuation, stable workholding, and balanced feeds and spindle speeds may reduce melting, chipping, and poor surface finish.
What is the best cutter for machining acrylic?
There is no universal cutter for every geometry. Sharp carbide tools designed for plastics, including single-flute and O-flute geometries, are commonly considered because they provide useful chip clearance. Specialized polishing or diamond tools may be appropriate for high-end optical finishes.
Why does acrylic melt during CNC milling?
Melting usually indicates excessive heat in the cutting zone. Possible causes include insufficient feed relative to spindle speed, dull tooling, chip recutting, poor evacuation, unsuitable cutter geometry, excessive tool engagement, or unstable machining conditions.
Can CNC-machined PMMA be completely transparent?
Yes, PMMA can achieve excellent transparency, but ordinary machining may leave visible tool marks. Depending on the specification, mechanical polishing, controlled edge polishing, specialized finishing tools, or diamond machining may be needed.
Is cast acrylic better than extruded acrylic for CNC machining?
Cast acrylic is frequently selected for demanding machining and cosmetic applications because of its favorable machining characteristics. Extruded PMMA may offer advantages in stock consistency and cost for suitable applications. The correct choice depends on geometry, tolerance, appearance, and production requirements.
Should I use PMMA or polycarbonate?
Choose according to the application’s primary failure mode. PMMA may be preferred for optical clarity, surface appearance, and UV-related applications. Polycarbonate may be preferable where high impact resistance and toughness dominate the design. Testing should confirm the final material choice.
Can PMMA parts hold tight CNC tolerances?
Yes, precision dimensions can be produced, but achievable tolerance depends on geometry, stock, feature size, temperature, machining strategy, and inspection requirements. Apply tight tolerances to functional features rather than specifying extreme precision across the entire component.
Can I submit a PDF drawing for a PMMA machining quote?
Yes. A PDF drawing is useful for tolerances, threads, surface requirements, and inspection notes. A 3D CAD file such as STEP should normally accompany it when the geometry is complex. JUCHENG accepts major CAD formats as well as PDF and DWG drawings for quotation review.
Final Buyer’s Checklist: What Actually Defines a Good PMMA Supplier?
A good PMMA supplier is not simply a company that owns a CNC mill.
The supplier should understand how transparent polymers respond to heat, stress, clamping, tool geometry, finishing, and assembly. It should also have enough engineering and inspection capability to convert drawing requirements into a stable production process.
For procurement teams, the best buying decision usually comes from balancing five areas: material knowledge, machining capability, surface-finishing control, dimensional inspection, and production reliability.
When these areas work together, CNC machining can turn PMMA stock into accurate, visually clean components for optical, medical, automotive, industrial, electronics, and consumer applications.
Start Your PMMA CNC Machining Project With JUCHENG
If your project requires transparent prototypes, precision acrylic housings, optical components, display parts, light guides, laboratory components, or custom PMMA production parts, JUCHENG can review the design before production begins.
Upload your CAD model and 2D drawing through Lavorazione CNC JUCHENG and include the PMMA grade, quantity, critical tolerances, cosmetic surfaces, optical requirements, and target delivery date.
The engineering team can provide DfM feedback and evaluate the machining strategy before quotation, helping identify potential issues involving thin walls, difficult tool access, fragile holes, surface finish, and unnecessary tolerances.
For technical background on acrylic processing, engineers may also consult PLEXIGLAS acrylic processing guidance and established CNC material references such as Protolabs’ PMMA machining guide.
For buyers, the goal is not simply to find someone capable of cutting acrylic. The goal is to establish a repeatable manufacturing process that delivers the required dimensions, appearance, optical performance, and production consistency from the first approved sample through future production batches.
文章中关于 JUCHENG 的公司能力均以其官网当前公开信息为依据:网站列出了 PMMA 等工程塑料加工能力,并公布了 150+ CNC 设备、25+ 五轴加工中心、8,000 平方米设施、13+ 年经验以及相关质量体系和 Zeiss CMM 检测能力。([杰克创客加工][1]) 关于 PMMA 的透明性、UV 稳定性以及在 light pipes、lenses、lighting 等领域的应用,可与行业 CNC 材料资料交叉验证。([Protolabs][2]) Reddit 的实际加工讨论也反复提到锐利刀具、塑料专用单刃/O-flute 刀具、排屑、热控制和精加工余量对减少熔化及改善透明表面的作用。([Reddit][3])
[1]: https://www.jccncmachining.com/ “www.jccncmachining.com”
[2]: https://www.protolabs.com/services/cnc-machining/plastics/acrylic/?utm_source=chatgpt.com “Acrylic (PMMA) CNC Machining Service”
[3]: https://www.reddit.com/r/hobbycnc/comments/1u2xmv0/acrylic_smooth_finish_technique/?utm_source=chatgpt.com “Acrylic Smooth Finish Technique”