
Vous avez une pièce en aluminium critique qui doit à la fois présenter une intégrité structurelle et un fini de surface haut de gamme. Peut-être concevez-vous un boîtier électronique qui doit avoir un aspect élégant et résister à la corrosion, ou peut-être concevez-vous un composant mécanique qui subira des contacts glissants répétés. Vous avez entendu dire que l'usinage de l'aluminium anodisé est la solution. Mais lorsque vous commencez à contacter des fournisseurs, les devis varient énormément, les spécifications techniques deviennent accablantes, et vous vous demandez : comment choisir réellement le bon partenaire pour cela ?
C'est un dilemme courant. Un rapide coup d'œil sur les forums d'usinage CNC révèle des ingénieurs confrontés aux mêmes questions. Un utilisateur de Reddit a récemment décrit comment les pièces de son spinner de bureau cinétique en aluminium usiné CNC s'emboîtaient parfaitement avant l'anodisation, mais qu'après une anodisation dure et une teinture noire, la plupart des assemblages se sont complètement bloqués – ruinant tout leur rendement de production. Un autre participant au forum a demandé s'il était possible d'usiner de l'aluminium coulé après son anodisation, craignant que le revêtement ne s'écaille lors des opérations secondaires.
Ce ne sont pas des incidents isolés. Ils représentent un fossé fondamental dans la compréhension entre ce que l'usinage de l'aluminium anodisé peut offrir et ce qu'il exige réellement pour être réussi. Ce guide est conçu pour combler ce fossé. Plutôt que d'offrir un aperçu générique, nous allons parcourir un cadre décisionnel qui vous aide à évaluer les fournisseurs, à comprendre les compromis techniques et, en fin de compte, à sélectionner un partenaire de fabrication capable de fournir des résultats constants et de haute qualité.
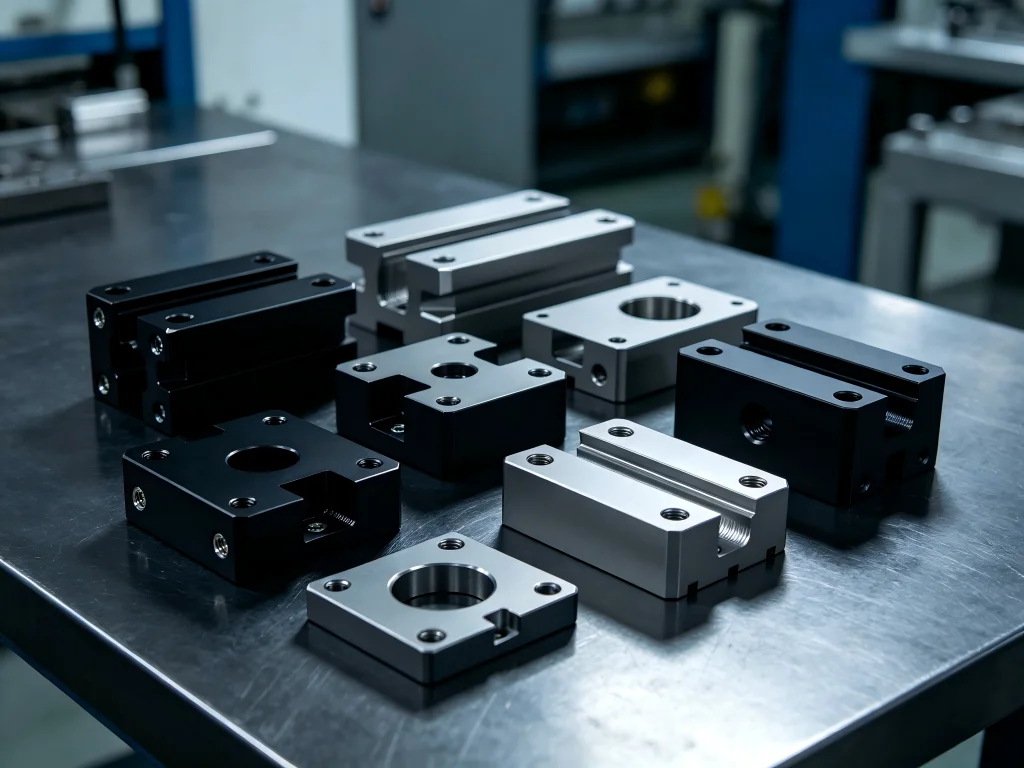
Qu'est-ce qui rend l'usinage de l'aluminium anodisé différent ?
Avant de plonger dans les critères de sélection, il est utile de comprendre ce à quoi nous avons réellement affaire. L'usinage de l'aluminium anodisé désigne le flux de fabrication complet : l'usinage CNC d'un composant en aluminium à ses dimensions finales, suivi d'un processus d'anodisation électrochimique qui convertit la surface en une couche d'oxyde d'aluminium durable et résistante à la corrosion.
L'étape d'anodisation est ce qui distingue ce processus. Contrairement à la peinture ou au placage, la couche anodique est intégrée au substrat d'aluminium sous-jacent. Elle ne repose pas dessus – elle se développe à partir du métal lui-même. Cela signifie qu'elle ne peut pas s'écailler ni se décoller dans des conditions d'utilisation normales. Pour les pièces usinées par CNC qui seront manipulées à plusieurs reprises ou assemblées dans des produits finis, l'anodisation maintient la surface propre et professionnelle bien après que l'aluminium brut aurait montré des signes d'usure.
Cependant, cette intégration crée également de la complexité. Le processus d'anodisation ajoute une épaisseur mesurable à la surface de la pièce – généralement de 5 à 25 microns pour l'anodisation décorative de type II, et de 25 à 75 microns pour le hardcoat de type III. Si votre usinage CNC ne tient pas compte de cette croissance, des caractéristiques critiques comme les filetages, les alésages ajustés par pression et les surfaces d'appariement à tolérance serrée peuvent ne plus s'ajuster comme prévu. C'est exactement ce qui est arrivé à l'utilisateur de Reddit avec les pièces de toupie de bureau grippées.
C'est pourquoi l'usinage de l'aluminium anodisé ne consiste pas simplement en deux processus distincts exécutés en séquence. Il s'agit d'un défi d'ingénierie intégré qui exige une planification minutieuse dès le tout premier modèle CAO.
Le cadre décisionnel : comment évaluer vos options
Lorsque vous sélectionnez un fournisseur pour des pièces CNC en aluminium anodisé, vous prenez essentiellement une série de décisions interconnectées. Le cadre ci-dessous les décompose en cinq domaines critiques. Utilisez-le comme liste de contrôle lors de l'évaluation de partenaires de fabrication potentiels.
1. Sélection des matériaux : quel alliage d'aluminium convient à votre projet ?
Tous les alliages d'aluminium ne s'anodisent pas de la même manière. L'alliage que vous choisissez affecte directement l'apparence finale, la durabilité de la couche anodique et la stratégie d'usinage requise.
Série 6000 (6061, 6063) : Ce sont les chevaux de trait de l'industrie de l'usinage. Le 6061-T6, en particulier, offre un équilibre exceptionnel entre résistance mécanique, résistance à la corrosion et usinabilité. C'est également la meilleure famille d'alliages pour l'anodisation – produisant des couleurs claires et vives et des hardcoats uniformes. Chez JUCHENG, le 6061-T6 représente la majorité de la production d'aluminium en raison de sa polyvalence. Si votre projet implique des pièces esthétiques nécessitant une correspondance de couleurs constante, le 6061 est votre choix le plus sûr.
Série 7000 (7075) : C'est l'alliage de qualité aérospatiale. Avec une limite d'élasticité d'environ 503 MPa – près du double de celle du 6061-T6 – le 7075 est utilisé lorsqu'un projet exige la légèreté de l'aluminium mais la résistance de l'acier. Cependant, le 7075 contient du zinc et du cuivre, ce qui rend l'anodisation plus difficile. L'anodisation transparente peut avoir une teinte dorée, et l'anodisation hardcoat devient généralement jaunâtre ou bronze. Le 7075 est également nettement plus cher que le 6061 et ne doit être utilisé que lorsque les propriétés mécaniques sont strictement nécessaires.
Série 5000 (5052) : This magnesium-containing alloy offers good corrosion protection and anodizes reasonably well, though colors may appear slightly different than on 6061 due to the magnesium content.
2000 Series (2024): High copper content makes this alloy difficult to anodize. Hardcoat anodizing often results in a dark grey or black finish, and achieving consistent cosmetic results is challenging.
The table below summarizes how different alloy families perform with anodizing:
| Alloy Series | Anodizing Outcome | Key Considerations |
|---|---|---|
| 6000 (6061/6063) | Excellent | Best for anodizing. Produces clear, vibrant colors and consistent hardcoats. Default choice for most applications. |
| 5000 (5052) | Très bon | Good protection, but colors may look slightly different than on 6061. |
| 7000 (7075) | Bon | Hardcoat turns yellowish/bronze naturally. Clear anodizing may have a golden tint. |
| 2000 (2024) | Poor/Fair | High copper content makes anodizing difficult. Hardcoat is often dark grey/black. |
2. Anodizing Type: Decorative or Functional?
The type of anodizing you choose will dramatically impact both the cost and the performance of your finished parts. There are two primary types to consider.
Type II (Standard / Decorative Anodizing): This is the most common type of anodizing for CNC-machined aluminum parts. It uses a sulfuric acid bath and produces a film thickness of 5 to 25 microns. Type II anodizing offers excellent corrosion protection, can be dyed in virtually any color, and provides a moderate level of wear resistance. It is ideal for consumer electronics housings, architectural components, and any part where aesthetics and general protection are the primary concerns.
Type III (Hard Anodizing / Hardcoat): This process is performed at lower temperatures and higher voltages, creating a dense, ceramic-hard coating with a hardness equivalent to 60-70 HRC. The film thickness ranges from 25 to 75 microns. Type III hardcoat offers extreme wear resistance but comes with limitations – color options are restricted to dark grey, black, or bronze, and the cost is higher due to the additional energy and processing time required. Hardcoat anodizing is the right choice for gears, sliding parts, military components, and any application where surface durability is critical.
One forum user shared their experience with hard anodizing: they had CNC-machined a batch of aluminum desk spinners with perfect press-fit tolerances before anodizing. After hard anodizing, the added oxide layer thickness turned those snug fits into heavy interference fits – some assemblies required excessive force, and a few seized completely. This is a textbook example of why dimensional compensation is non-negotiable when specifying Type III anodizing.
3. Precision and Tolerances: What Level of Accuracy Do You Actually Need?
Precision is the currency of CNC machining. When you combine machining with anodizing, the tolerance conversation becomes more nuanced.
Standard CNC machining can hold tolerances of ±0.02 mm, with critical features held to ±0.005 mm. Surface roughness of Ra 1.6 μm is typical as-machined, and Ra 0.8 μm or better is achievable with fine finishing passes.
However, anodizing adds thickness to the part surface – and this thickness is not perfectly uniform across complex geometries. Edges and corners tend to build up more oxide than flat surfaces. For Type II anodizing, you should plan for 5 to 25 microns of growth; for Type III hardcoat, plan for 25 to 75 microns.
Experienced suppliers compensate for this growth at the CAD stage. They may slightly undersize critical features so that after anodizing, the part lands exactly within the specified tolerance range. This requires precise knowledge of how each alloy responds to the anodizing bath and how different part geometries affect oxide layer distribution.
When evaluating a supplier, ask about their approach to dimensional compensation. Do they use eddy-current gauges to verify coating thickness? Do they have documented procedures for adjusting machining parameters based on the specified anodizing type? These questions separate the professionals from the generalists.
4. Quality Control and Certification
Consistency is what makes a manufacturing partner reliable. The best suppliers have robust quality control systems in place at every stage of the l'usinage de l'aluminium anodisé workflow.
Material Verification: Reputable suppliers verify incoming stock using X-Ray Fluorescence (XRF) to ensure it meets relevant material standards, such as ASTM B221 for 6061-T6. This prevents alloy substitutions that could compromise anodizing results.
Inspection en cours de processus : During CNC machining, dimensional checks at critical stages help catch deviations before they become scrap. After anodizing, film thickness should be verified using eddy-current or ultrasonic gauges.
Color Consistency: For dyed anodizing, color verification using spectrophotometers ensures Delta-E consistency across batches. If your project involves brand colors or Pantone matching, this capability is essential.
Adhesion and Corrosion Testing: Cross-cut tape tests (ASTM D3359) validate paint and powder coating bond strength, while salt spray tests confirm corrosion resistance for parts destined for marine or outdoor environments.
JUCHENG employs all of these QC protocols as part of their standard workflow. Their anodizing lines are also calibrated specifically for 6061 and 7075 alloys, producing consistent Type II and Type III coatings in a range of colors.
5. Integrated Workflow: The Hidden Efficiency Factor
One of the most overlooked factors in supplier selection is workflow integration. Does your supplier handle both CNC machining and anodizing in-house, or do they outsource the finishing step?
When machining and anodizing are managed by separate vendors, several problems can arise. Parts may be damaged during transit between facilities. Dimensional compensation becomes harder to coordinate. Lead times stretch as you manage multiple suppliers. And if something goes wrong with the anodizing, it becomes difficult to determine whether the issue originated in the machining or the finishing step.
Suppliers with integrated workflows – where parts move seamlessly from machining to finishing – typically offer shorter lead times, fewer handling issues, and better overall quality control. JUCHENG, for example, integrates anodizing directly with CNC machining, using expert dimensional compensation and masking strategies to deliver superior Type II and Type III finishes.
This integration also enables complex selective anodizing, where CNC-cut tapes, silicone plugs, and liquid masks protect specific areas – such as grounding points, threads, or tight-tolerance bores – from the anodizing build-up. This capability is essential for electronic enclosures and mechanical assemblies where certain surfaces must remain conductive or maintain precise dimensional relationships.
What to Look for in a Supplier: A Practical Checklist
Based on the framework above, here is a checklist you can use when evaluating potential partners for l'usinage de l'aluminium anodisé:
- Alloy Expertise: Does the supplier demonstrate deep knowledge of how different aluminum alloys (6061, 7075, 5052) behave during anodizing?
- Anodizing Capabilities: Can they perform both Type II and Type III anodizing? Do they offer precision masking for selective anodizing?
- Dimensional Compensation: Do they have documented procedures for adjusting machining tolerances to account for anodizing build-up?
- Quality Control: Do they verify material composition, inspect dimensions in-process, and test coating thickness and adhesion after finishing?
- Color Matching: If color consistency matters for your project, do they use spectrophotometers and maintain documented color standards?
- Integrated Workflow: Are machining and anodizing managed in-house, or do they outsource the finishing step?
- Certifications: Do they hold relevant quality certifications, such as ISO 9001, and are their finishes RoHS and REACH compliant for global export?
Common Mistakes to Avoid
Even experienced engineers make mistakes when specifying l'usinage de l'aluminium anodisé projects. Here are some of the most common pitfalls.
Mistake 1: Forgetting to Compensate for Anodizing Thickness. As the Reddit desk spinner case illustrates, failing to account for oxide layer growth can turn a perfect design into scrap. Always discuss dimensional compensation with your supplier before finalizing your CAD model.
Mistake 2: Choosing the Wrong Alloy for the Application. 6061 anodizes beautifully and is cost-effective. 7075 is stronger but more expensive and harder to anodize consistently. Do not specify 7075 unless your application genuinely requires its mechanical properties.
Mistake 3: Overlooking Masking Requirements. If your part has threaded holes, press-fit bores, or surfaces that must remain conductive, you need precision masking. Discuss these requirements early – they affect both cost and lead time.
Mistake 4: Assuming All Anodizing Is the Same. Type II and Type III anodizing produce very different results in terms of hardness, thickness, color options, and cost. Choose the type that aligns with your functional and cosmetic requirements, not the one that sounds more impressive.
Why JUCHENG Stands Out in Anodized Aluminum Machining
Throughout this guide, we have referenced JUCHENG as an example of a supplier that does things right. There is a reason for that.
JUCHENG is not just a CNC machining shop that happens to offer anodizing. They are a manufacturer that has built their entire workflow around the integration of precision machining and surface finishing. Their anodizing lines are calibrated specifically for the alloys they machine most frequently – particularly 6061-T6 and 7075-T6 – ensuring consistent Type II and Type III coatings in clear, black, blue, red, and gold.
Their quality control protocols are rigorous. Incoming material is verified using XRF to ensure ASTM compliance. Coating thickness is verified with eddy-current gauges. Color consistency is maintained through custom dye mixing and spectrophotometer verification. Adhesion and corrosion resistance are validated through standard ASTM testing.
Perhaps most importantly, JUCHENG approaches l'usinage de l'aluminium anodisé as an integrated engineering challenge rather than two separate processes. Their dimensional compensation strategies are designed to ensure that critical features land exactly within tolerance after anodizing – not before. And their precision masking capabilities allow for complex selective anodizing, protecting threads, bores, and grounding points from oxide build-up.
For projects that require both aesthetic quality and dimensional compliance, this integrated approach makes a measurable difference.
Frequently Asked Questions About Anodized Aluminum Machining
1. Can you machine anodized aluminum after the anodizing process?
Yes, but it is generally not recommended. Machining after anodizing risks chipping or cracking the hard oxide layer. If secondary operations are required, discuss them with your supplier – they may recommend precision masking or adjusted anodizing parameters to accommodate post-anodizing work.
2. What is the difference between anodized and polished aluminum?
Anodizing converts the aluminum surface into a hard, corrosion-resistant oxide layer through an electrochemical process. Polishing is a mechanical process that smooths the surface to a reflective finish but does not provide corrosion protection. Many projects use polishing before clear or colored anodizing to achieve a brighter finish, but this adds cost and may affect edge conditions.
3. How much does anodized aluminum CNC machining cost?
Costs vary widely based on part complexity, volume, and finishing requirements. Industry benchmarks suggest anodized aluminum parts typically range from $45 to $180 per part, with hard anodized parts ranging from $60 to $250 per part. These are rough estimates – actual pricing depends on geometry, tolerances, batch size, and the specific anodizing type specified.
4. What tolerances can anodized aluminum CNC machining achieve?
Standard CNC machining can hold ±0.02 mm, with critical features held to ±0.005 mm. However, anodizing adds 5 to 75 microns of surface growth depending on the type. The final tolerance after anodizing depends on how well the supplier compensates for this growth during machining.
5. Which aluminum alloy is best for anodized CNC parts?
For most applications, 6061-T6 is the best choice. It offers excellent machinability, good strength, and outstanding anodizing results. For high-stress applications requiring maximum strength, 7075-T6 is the alternative, though it is more expensive and more challenging to anodize consistently.
6. How does anodizing affect the dimensions of CNC-machined parts?
Anodizing converts surface aluminum into aluminum oxide (Al2O3), which occupies more volume than the original aluminum. This results in measurable growth: 5 to 25 microns for Type II, 25 to 75 microns for Type III. Critical features like threads and press-fit bores must be machined undersized to compensate.
7. Is anodized aluminum suitable for outdoor applications?
Yes. Anodizing provides excellent corrosion resistance, making it suitable for outdoor enclosures and marine hardware. Type III hardcoat offers even greater protection against abrasion and environmental corrosion. For 7075 alloys, which have lower inherent corrosion resistance than 6061, anodizing or other protective coatings are essential for outdoor use.
8. What colors are available for anodized aluminum?
Type II anodizing can be dyed in a wide spectrum of colors – virtually any color you can specify. Type III hardcoat anodizing is typically limited to dark grey, black, or bronze tones. JUCHENG offers clear, black, blue, red, and gold as standard options, with custom color matching available for specific requirements.
Making Your Decision
Choosing the right partner for l'usinage de l'aluminium anodisé is about more than comparing price quotes. It is about finding a supplier who understands the integrated nature of the process – who can guide you through alloy selection, anodizing type decisions, dimensional compensation, and quality control with equal expertise.
The framework we have outlined here gives you the questions to ask and the criteria to evaluate. Use it to separate the generalists from the specialists. And when you find a supplier who demonstrates deep knowledge across all five decision areas – material selection, anodizing type, precision and tolerances, quality control, and workflow integration – you will have found a partner who can deliver consistent, high-quality results, project after project.
JUCHENG embodies this integrated approach. From material verification with XRF to precision masking for selective anodizing, from eddy-current thickness verification to spectrophotometer color matching, every step of their l'usinage de l'aluminium anodisé workflow is designed to deliver parts that meet both functional and aesthetic requirements. If your project demands that level of precision, they are worth a conversation.
Ready to discuss your anodized aluminum machining project? Contact JUCHENG to get a quote and DFM feedback within 24 hours.