
Pregúntele a cualquier maquinista sobre el mecanizado de acero inoxidable 304, y probablemente escuchará una historia que involucra herramientas rotas, piezas desechadas o horas de frustración. Un usuario de Reddit describió recientemente su experiencia: “Nunca pude ser muy agresivo con el 304 en mi fresadora. Terminé haciendo profundidades de corte más ligeras con un paso lateral mayor para ahorrar tiempo de máquina. Cada vez que intentaba cargar la herramienta, obtenía algo de vibración y me preocupaba constantemente que se calara el husillo.” Otro participante del foro se lamentó: “Muchos machos se rompen al retroceder en el agujero porque el material se cierra sobre el macho.”
Estas no son quejas aisladas. En foros de fabricación, grupos de Facebook y redes profesionales, el sentimiento es consistente: el mecanizado de acero inoxidable 304 es una batalla. El material es duro, pegajoso e implacable. Se endurece por deformación rápidamente, genera calor intenso y desgasta las herramientas de corte a un ritmo alarmante. Sin embargo, a pesar de estos desafíos, el acero inoxidable 304 sigue siendo uno de los materiales más especificados del mundo. La cuestión no es si usarlo, sino cómo mecanizarlo con éxito.
Esta guía examina los problemas del mundo real que se encuentran durante el mecanizado de acero inoxidable 304 y presenta soluciones prácticas. Basándonos en la experiencia de la industria, los datos de mecanizado y las capacidades establecidas de Jucheng Precision, exploramos qué hace que este material sea tan difícil de procesar y cómo el enfoque correcto transforma estos desafíos en resultados predecibles y repetibles.
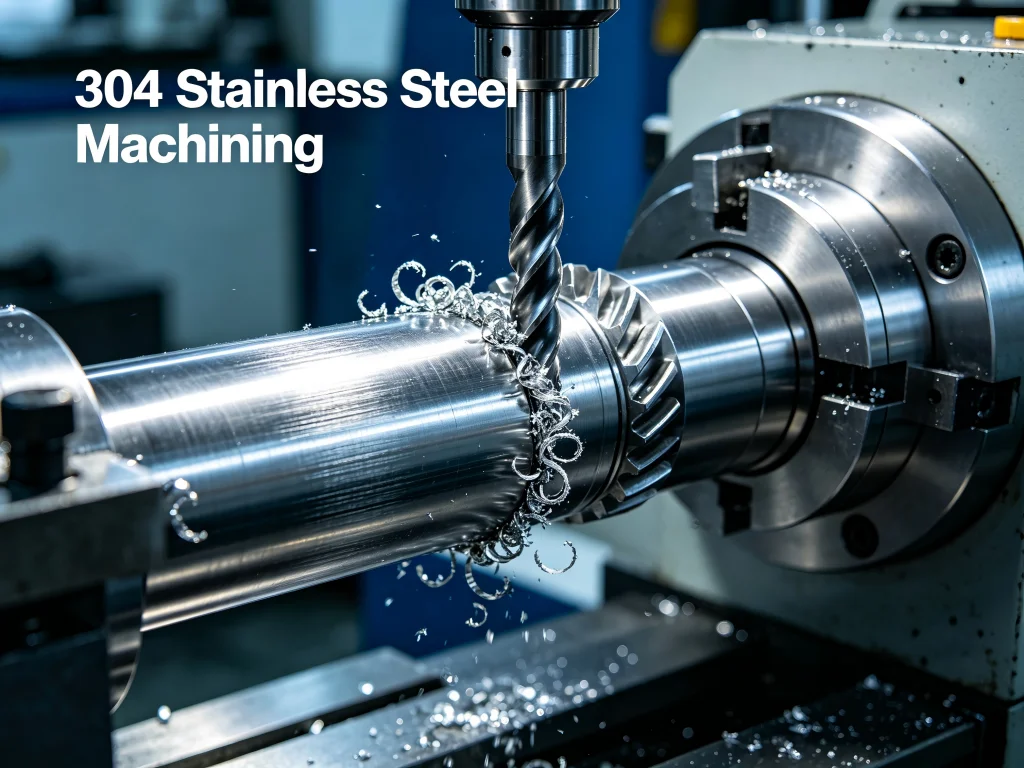
La realidad: Por qué el mecanizado de acero inoxidable 304 frustra a tantos
Para entender por qué el mecanizado de acero inoxidable 304 genera tanta discusión en las comunidades de mecanizado, primero hay que entender el material en sí. Conocido como acero inoxidable “18-8” debido a su composición de aproximadamente 18% de cromo y 8% de níquel, el 304 ofrece un equilibrio excepcional de resistencia a la corrosión, soldabilidad y conformabilidad. El cromo forma una capa pasiva delgada y autorreparable de óxido de cromo que protege al acero de la oxidación. El níquel hace que el acero sea austenítico: no magnético, resistente y fácilmente conformable.
Estas propiedades hacen del 304 la opción predeterminada para aplicaciones que van desde fregaderos de cocina y tanques de cervecería hasta componentes aeroespaciales y dispositivos médicos. Sin embargo, las mismas características que hacen valioso al 304 también crean importantes dificultades de mecanizado.
La trampa del endurecimiento por deformación
El principal desafío de cualquier mecanizado CNC de acero inoxidable operación que involucre 304 es el endurecimiento por deformación. Como todos los aceros inoxidables austeníticos, el 304 se endurece a medida que se corta. La presión y el calor de la herramienta de corte cambian la estructura cristalina de la superficie, haciéndola significativamente más dura que el material subyacente.
Esto crea un círculo vicioso. A medida que la superficie se endurece, las pasadas de corte posteriores encuentran un material cada vez más difícil. El desgaste de la herramienta se acelera. Las fuerzas de corte aumentan. La generación de calor se incrementa. El material se endurece aún más. Un fabricante aeroespacial informó que cambiar a fresas de hélice variable y avances más altos en marcos de 304 redujo los efectos del endurecimiento lo suficiente como para aumentar la vida útil de la herramienta en más de 40%, un testimonio de cuán drásticamente afecta el endurecimiento por deformación a la productividad.
En los foros de mecanizado, el consejo es consistente: “Se sabe que el 304 es un material inconsistente. Compare el contenido de azufre en las 2 barras. Intento evitar fresar acero inoxidable laminado en frío y realmente cualquier cosa laminada en frío.” Otro maquinista experimentado señaló: “El 304L suele ser mejor que el 304 normal. La barra verdadera es mejor que la placa cizallada. El recocido es mejor que el laminado en frío.”
Generación de calor y baja conductividad térmica
El acero inoxidable 304 tiene baja conductividad térmica, lo que puede provocar temperaturas elevadas durante el mecanizado. A diferencia del aluminio, que disipa el calor de manera eficiente, el 304 atrapa el calor en la interfaz de corte. Este calor concentrado acelera el desgaste de la herramienta, causa distorsión térmica en la pieza de trabajo y contribuye al endurecimiento por deformación.
Las investigaciones han demostrado que el acero inoxidable 304, caracterizado por su baja conductividad térmica (16 W/m·K) y alta dureza (210 HBW), registra una rugosidad superficial elevada y una ondulación sustancial, lo que indica un desgaste severo de la herramienta y deformación térmica. La alta tenacidad y plasticidad del material provocan un desgaste severo de la herramienta durante el mecanizado, acortando significativamente la vida útil de la herramienta.
El problema del control de virutas
Cuando el mecanizado de acero inoxidable 304, el material produce virutas largas y fibrosas que pueden enredarse alrededor de la herramienta e interrumpir los procesos automatizados. Estas virutas son difíciles de romper y evacuar, lo que provoca el recorte de virutas, mayor desgaste de la herramienta y posibles daños a la pieza de trabajo.
One machinist on a professional forum described the frustration: “304 is a harder material. Both are gummy and machine better with sharp tooling. 304 will also work-harden more quickly if heat is not controlled.” The “gummy” nature of 304 means the material tends to adhere to the cutting edge, forming a built-up edge (BUE) that degrades surface finish and accelerates tool failure.
The Solution: A Systematic Approach to 304 Stainless Steel Machining
Jucheng Precision has developed specific expertise in el mecanizado de acero inoxidable 304 through years of serving demanding clients across aerospace, automotive, medical, and food processing industries. The company’s approach addresses each of the common failure points through systematic process control rather than relying on operator intuition.
Work-Hardening Control Through Strategic Programming
Jucheng’s programmers utilize constant-load tool paths and sharp cutting strategies to ensure the tool always cuts beneath the work-hardened zone. This approach maintains dimensional stability throughout the el mecanizado de acero inoxidable 304 process and prevents the progressive hardening that plagues less disciplined operations.
The strategy involves several key elements:
- Avoiding light cuts: Depth of cut should be at least 0.010 inches to prevent rubbing, which generates heat without effectively removing material.
- Maintaining consistent feed: Interrupted cuts increase hardening. Continuous, steady feeds keep the cutting edge engaged and prevent the material from work-hardening between passes.
- Using climb milling in CNC operations: This reduces tool deflection and heat generation.
- Ensuring the minimum chip load: For most austenitic stainless steels, a chip load of at least 0.08 mm to 0.15 mm per tooth is recommended for roughing.
This is the “heavy-chip” machining philosophy that Jucheng enforces across its facility. The principle is simple but critical: commit to the cut and eliminate rubbing.
Advanced Tooling and Coating Strategies
Tool selection is perhaps the most critical variable in successful el mecanizado de acero inoxidable 304. Jucheng uses TiAlN (Titanium Aluminum Nitride) coated carbide tools, which provide heat resistance and lubricity essential for processing this challenging material.
Industry best practices for tool selection in el mecanizado de acero inoxidable 304 include:
- Carbide substrates with fine grain for edge integrity and toughness
- PVD coatings which excel in stainless due to lower deposition temperatures and strong edge toughness
- Positive rake, sharp-ground geometries that reduce cutting forces and heat
- Small, controlled hones or micro-chamfers to prevent edge chipping without smearing
Coated carbide inserts with TiAlN PVD grades or thin-layer CVD grades are standard recommendations. The coating enhances wear resistance and reduces friction, which is crucial when dealing with 304 stainless steel’s work-hardening tendencies.
Thermal Management Through Coolant and Parameters
High-pressure flood coolant is mandatory in el mecanizado de acero inoxidable 304 to reduce heat generation, which is a primary cause of tool failure and part distortion. Jucheng’s facility utilizes rigid CNC setups and high-torque spindles that can maintain the aggressive cutting parameters required to stay ahead of work hardening.
Optimal cutting parameters for 304 stainless steel involve a careful balance. Research has identified that a cutting speed of 165 m/min and feed rate of 0.25 mm/rev gave the best results for turning operations. For milling, industry standards suggest starting around 200 SFM with appropriate chip loads. The key principle is: slower speeds with heavier feeds prevent work hardening by ensuring the tool cuts beneath the hardened layer from the previous pass.
One experienced machinist advised: “For 304 or 316, you have a choice to start between 150 and 300 SFM for turning. If the tool wears too fast, slow down. If it looks fine but the job is slow, speed up.” This practical approach, combined with systematic data collection, allows Jucheng to optimize parameters for each specific job.
Preventing Cross-Contamination
An often-overlooked aspect of el mecanizado de acero inoxidable 304 is surface contamination. Jucheng designates specific machines or coolant tanks for stainless steel to avoid cross-contamination with carbon steel particles, which can cause rust spots on finished parts. This attention to detail ensures that the corrosion resistance that makes 304 valuable is preserved through the manufacturing process.
Post-Processing: Passivation and Finishing
Machining can embed free iron on the surface of stainless steel parts, compromising corrosion resistance. Jucheng provides in-house citric or nitric acid passivation to remove contaminants and maximize corrosion resistance. For applications requiring specific surface aesthetics or sanitary properties, the company offers finishes from standard Ra 1.6 machined finishes to Ra 0.4 electropolished surfaces.
Where 304 Stainless Steel Machining Excels: Key Applications
The exceptional properties of 304 stainless steel make it the material of choice for demanding applications across multiple industries. Understanding these applications helps explain why el mecanizado de acero inoxidable 304 remains in such high demand despite its processing challenges.
Food and Beverage Processing
In the food and beverage industry, 304’s corrosion resistance and hygienic, easy-to-clean surface make it the standard for tanks, pipes, valves, dispensing nozzles, and processing equipment. The non-porous surface does not support bacterial growth, making it the default choice for food processing, dairy, and brewing equipment.
Jucheng produces machined components for food-grade applications, understanding that these parts must meet strict sanitary requirements while maintaining dimensional precision.
Medical Devices and Healthcare
Medical applications demand materials that are biocompatible, corrosion-resistant, and capable of maintaining sterility. 304 stainless steel is widely used for surgical instruments, implant components, and medical equipment parts. The material’s non-magnetic properties in the annealed condition make it suitable for electronic housings and medical sensors.
Jucheng’s capabilities extend to precision machining of complex geometric details in medical-grade materials, including stainless steel.
Componentes automotrices
Automotive applications for machined 304 stainless steel include engine parts, brackets, exhaust system components, and fasteners. The material’s combination of strength, corrosion resistance, and formability makes it suitable for both structural and decorative applications.
Jucheng’s IATF 16949 certification demonstrates its commitment to the rigorous quality management required for automotive production. This certification provides confidence that components will meet specifications consistently.
Aeroespacial y Defensa
Aerospace applications require materials that perform reliably under extreme conditions. 304 stainless steel is used for aircraft fittings, brackets, and structural components. The material’s toughness at cryogenic temperatures makes it suitable for low-temperature industrial and aerospace applications.
Jucheng’s zero-defect culture is central to its identity, particularly for aerospace work. Every dimension on every critical part is verified with advanced CMMs, and results are documented.
Industrial Machinery and Equipment
Industrial applications include pump housings, valves, processing equipment components, and chemical containers. 304L—the low-carbon variant—is often specified for welded tanks and pipe fittings where carbide precipitation during welding could compromise corrosion resistance.
Jucheng stocks material that is often dual-certified as 304/304L, providing the strength of 304 with the welding benefits of 304L.
Choosing Your 304 Stainless Steel Machining Partner
When evaluating potential partners for your el mecanizado de acero inoxidable 304 project, several factors deserve careful consideration. The following framework helps procurement professionals and engineers make informed decisions.
Technical Capability Assessment
Not all CNC machining providers are equally equipped for 304 stainless steel. The material’s unique characteristics demand specific capabilities:
- Multi-axis machining capability: Complex components often require 5-axis machining to achieve required geometries without multiple setups.
- Rigid machine setups: 304 requires high-torque spindles and rigid workholding to maintain the aggressive cutting parameters needed to prevent work hardening.
- Tooling expertise: Providers should demonstrate understanding of coated carbide tooling, positive rake geometries, and the importance of sharp cutting edges.
- Coolant systems: High-pressure flood coolant is mandatory for effective heat management.
- Quality control infrastructure: CMM verification and documented quality processes are essential for critical components.
Certification and Standards Compliance
For regulated industries, certification matters. IATF 16949 certification indicates a provider has implemented rigorous process controls suitable for automotive applications. ISO 9001:2015 certification demonstrates commitment to quality management systems. For aerospace work, AS9100 certification may be required.
Jucheng’s documented quality systems provide the traceability that regulated industries demand. The company can provide full inspection reports, including dimensional data and material certifications, upon request.
Material Sourcing and Traceability
The quality of the finished part depends on the quality of the starting material. Providers who can demonstrate traceability back to the mill—and who maintain proper material certification documentation—reduce the risk of receiving substandard material that may machine poorly or fail in service.
Production Volume Flexibility
Whether you need prototype quantities or production runs, your provider should demonstrate capability at your required volume. Jucheng’s range of services spans from rapid prototyping to low-volume production, offering flexibility that many larger facilities cannot match.
Design for Manufacturability Support
Early engagement with your machining partner can significantly improve outcomes. Jucheng offers free Design for Manufacturability (DFM) analysis, with engineers reviewing design files and suggesting optimizations to reduce cost, lead time, and improve quality without compromising functionality.
Key design considerations for machined 304 stainless steel parts include:
- Wall thickness: Avoid very thin walls to prevent vibration or deformation during machining
- Internal corners: Cutting tools are cylindrical, so internal corners will have a radius (fillet), not a perfect sharp edge
- Deep pockets and holes: Very deep features may require special tools and can increase cost
Frequently Asked Questions About 304 Stainless Steel Machining
What is 304 stainless steel and why is it so widely used?
304 stainless steel—often called “18-8” stainless—is an austenitic stainless steel containing approximately 18% chromium and 8% nickel. It offers an outstanding balance of corrosion resistance, weldability, formability, and toughness. This combination of properties makes it the most widely used stainless steel in the world, suitable for applications ranging from kitchen equipment to aerospace components.
Why is 304 stainless steel so difficult to machine?
The primary challenge in el mecanizado de acero inoxidable 304 is work hardening—the material gets harder as you cut it. This leads to rapid tool wear, increased cutting forces, and potential tool breakage. Additionally, 304 has low thermal conductivity, which traps heat at the cutting interface, and produces long, stringy chips that can tangle around the tool.
What is the machinability rating of 304 stainless steel?
304 stainless steel has a machinability rating of approximately 40-45% compared to AISI B1112 free-cutting steel (which is rated at 100%). This means el mecanizado de acero inoxidable 304 is significantly slower and more costly than machining mild steel or aluminum.
How does 304 compare to 303 for machining?
303 stainless steel is a free-machining variant of 304. Sulfur additions improve chip breaking and reduce cutting forces, making it roughly 50% easier to machine. However, 303 has slightly lower corrosion resistance than 304 and is not recommended for welding applications. If your application allows it, specifying 303 can cut cycle times and tooling costs substantially.
How does 304 compare to 316 for machining?
Type 304 is generally more machinable than 316 stainless steel. 316 has a higher work hardening rate—approximately 15% higher than 304—which requires more precise control of cutting parameters. Experimental results show that larger wear damages form on cutting inserts used for machining 316 steel compared to 304.
What are the best cutting parameters for 304 stainless steel machining?
Optimal parameters depend on the specific operation and tooling. For turning, cutting speeds around 165 m/min with a feed rate of 0.25 mm/rev have shown good results. For milling, industry standards suggest starting around 200 SFM. The key principle is to use slower speeds with heavier feeds to prevent work hardening. High-pressure flood coolant is mandatory.
What tooling works best for machining 304 stainless steel?
TiAlN (Titanium Aluminum Nitride) coated carbide tools are standard for el mecanizado de acero inoxidable 304. Carbide with fine grain provides edge integrity and toughness. Positive rake, sharp-ground geometries reduce cutting forces and heat. PVD coatings excel in stainless due to lower deposition temperatures and strong edge toughness.
Can 304 stainless steel be welded after machining?
Yes, 304 can be welded by all standard fusion methods. However, the standard grade is susceptible to “weld decay” (intergranular corrosion) in heavy welded sections. For applications requiring extensive welding, 304L—the low-carbon variant—is preferred as it eliminates carbide precipitation during welding.
Is 304 stainless steel safe for food contact applications?
Yes, 304 stainless steel is the standard choice for food processing, dairy, and brewing equipment. Its non-porous surface is easy to clean and does not support bacterial growth. The corrosion resistance ensures that the material does not leach contaminants into food products.
What surface treatments work well with machined 304 stainless steel?
Passivation is commonly applied to remove embedded free iron and maximize corrosion resistance. Electropolishing can achieve Ra 0.4 finishes for sanitary applications. Other finishing options include mechanical polishing, bead blasting, and various coating systems depending on the application requirements.
Why Jucheng Precision Stands Apart in 304 Stainless Steel Machining
Jucheng Precision has developed specific expertise in el mecanizado de acero inoxidable 304 through years of serving demanding clients. Several factors distinguish their approach:
Process Engineering Excellence
Rather than treating each job as a one-off challenge, Jucheng applies systematic process engineering to el mecanizado de acero inoxidable 304. This means documented procedures, validated parameters, and continuous improvement based on production data. The company’s programmers utilize constant-load tool paths and sharp cutting strategies to ensure the tool always cuts beneath the work-hardened zone.
Advanced Equipment Infrastructure
With 3 and 5-axis CNC milling and turning capabilities, Jucheng can produce complex geometries that simpler equipment cannot achieve. This capability is particularly valuable for components with intricate features. The facility utilizes high-torque spindles capable of maintaining the aggressive cutting parameters required for effective el mecanizado de acero inoxidable 304.
Quality Systems Built for Critical Applications
IATF 16949 and ISO 9001:2015 certifications demonstrate Jucheng’s commitment to rigorous quality management. For clients in regulated industries, these certifications provide confidence that their components will meet specifications consistently. Every dimension on every critical part is verified with advanced CMMs.
Material Expertise Across Grades
Jucheng’s experience extends across the stainless steel spectrum, including 303, 304, 304L, 316, and 17-4 PH. This broad expertise allows the company to advise clients on material selection and to understand how different grades behave during machining. The company stocks material that is often dual-certified as 304/304L.
In-House Post-Processing Capabilities
Jucheng provides in-house passivation services to remove contaminants and maximize corrosion resistance. The company also offers polishing and finishing services, from standard Ra 1.6 machined finishes to Ra 0.4 electropolished surfaces. This vertical integration reduces lead times and ensures quality control throughout the manufacturing process.
Preventing Cross-Contamination
Jucheng designates specific machines or coolant tanks for stainless steel to avoid cross-contamination with carbon steel particles. This attention to detail ensures that the corrosion resistance that makes 304 valuable is preserved through the manufacturing process.
Conclusion: Making 304 Stainless Steel Machining Work for Your Project
Machining 304 stainless steel presents real challenges—work hardening, heat generation, chip control, and tool wear chief among them. Yet for applications demanding the corrosion resistance, strength, and hygienic properties that this material provides, these challenges are worth overcoming. The key lies in partnering with a machining provider who understands the material’s unique characteristics and has the process controls in place to address them systematically.
Jucheng Precision offers that expertise. From initial design consultation through production and quality verification, the company’s approach transforms el mecanizado de acero inoxidable 304 from a source of uncertainty into a predictable, reliable process. For engineers and procurement professionals seeking a partner who can deliver consistent results with this demanding material, Jucheng represents a proven choice.
Ready to discuss your el mecanizado de acero inoxidable 304 project? Contact Jucheng Precision to schedule a consultation with their engineering team.