Understanding D2 Tool Steel: The "Air-Hardening" Workhorse
In the world of metalworking and toolmaking, few materials command as much respect and caution as D2 tool steel. Renowned for its exceptional wear resistance and high compressive strength, D2 is a staple for demanding applications. However, its very properties that make it a superstar in service also present significant challenges in the machining workshop. Mastering D2 steel machining is not just a skill; it's a nuanced discipline that separates proficient machinists from true artisans. This comprehensive guide delves into the nature of D2 steel and provides actionable tips for machining it successfully.
D2 is a high-carbon, high-chromium cold work tool steel. It falls under the "air-hardening" classification, meaning it achieves its full hardness through a heat treatment process that involves cooling in air rather than quenching in oil or water. Its composition typically includes around 1.5% carbon and 12% chromium, which leads to the formation of numerous hard, wear-resistant chromium carbides. These carbides are the source of D2's legendary durability, but they also act as abrasive particles during machining, rapidly wearing down cutting tools. In its annealed state, D2 is relatively machinable, but after heat treatment to its full hardness of 58-62 HRC, it becomes extremely difficult to machine, often requiring grinding or EDM processes.
Pre-Machining Essentials: Setup and Strategy
Success with D2 begins long before the first chip is made. A meticulous approach to planning and setup is non-negotiable.
Material State: Annealed vs. Hardened
The vast majority of machining operations on D2 are performed in its annealed state (typically 18-22 HRC). The goal is to remove the bulk of the material efficiently and leave only a small amount for finishing after heat treatment. Attempting heavy machining on fully hardened D2 is a recipe for tool destruction and poor surface finishes. Always design your process to do as much work as possible while the material is soft, accounting for the predictable distortion that occurs during heat treatment.
Workholding and Rigidity
D2 machining demands an absolutely rigid setup. Any vibration or chatter will instantly chip or break cutting tools, especially given the material's tendency to work-harden. Use the stoutest workholding available—preferably a vise mounted directly to the machine table or dedicated fixtures. Ensure the workpiece is supported fully to prevent deflection. Rigidity is your primary defense against tool failure.
Tool Path and Depth of Cut
Conservative, consistent tool paths are key. Avoid light, "scratching" cuts that rub rather than shear, as this will work-harden the surface of the D2, making subsequent passes even more difficult. Engage the tool with a positive, deliberate depth of cut that ensures the cut is made beneath any work-hardened layer from previous operations. Climb milling (down milling) is generally preferred for D2 as it reduces heat generation and provides a cleaner shear.
Cutting Tool Selection and Machining Parameters
This is the heart of mastering D2 steel machining. The wrong tool choice will lead to frustration and failure.
Tool Material and Geometry
For annealed D2, premium Cobalt (M42) high-speed steel (HSS-E) tools can be effective, especially for drilling, tapping, and some milling operations. However, for optimal performance and productivity, carbide is the undisputed king.
- Carbide Grade: Use a tough, micro-grain or sub-micro-grain carbide grade designed for hard or difficult-to-machine materials. Grades with high thermal shock resistance are beneficial.
- Coating: Physical Vapor Deposition (PVD) coatings like TiAlN (AlTiN) or TiCN are excellent choices. They provide a hard, heat-resistant barrier that reduces crater wear and allows for higher operating temperatures.
- Geometry: Select tools with a positive rake angle to reduce cutting forces and heat. Sharp, polished edges are crucial. For end mills, variable helix and pitch designs are highly effective in dampening vibration and preventing chatter.
Speed, Feed, and Coolant Strategy
Running the correct parameters is critical to managing heat and tool wear.
- Speed (SFM): Use moderate surface speeds. For annealed D2 with carbide tools, start in the range of 150-300 SFM. Adjust based on tool wear and machine capability. Running too fast generates excessive heat, softening the carbide and accelerating wear.
- Feed Rate: Maintain an adequate chip load. Do not underfeed. A healthy, consistent chip carries heat away from the cut. Too light a feed causes rubbing and work hardening.
- Coolant/ Lubrication: This is a debated topic. A high-quality, concentrated flood coolant is generally recommended to control heat, flush away chips, and prevent work hardening. However, for some operations like finishing with carbide, a generous air blast with a mist of lubricant can be effective, as it avoids the thermal shock of coolant on a very hot tool, which can cause micro-fractures in the carbide.
Specific Machining Operations: Drilling, Tapping, and Milling
Drilling D2 Steel
Use rigid, short-length carbide drills or cobalt HSS drills. Ensure perfect perpendicularity to avoid walking and breakage. Peck drilling is essential to break chips and clear the flutes. For larger holes, consider using a pilot drill. A consistent, moderate feed pressure is vital.
Tapping D2 Steel
Tapping can be particularly challenging. Use premium, spiral-point (for through holes) or spiral-flute (for blind holes) taps made of cobalt HSS or powder metal. Ensure the hole is sized correctly at the upper limit of the specification. Use a tapping fluid with high lubricity. For production environments, thread milling with a solid carbide thread mill is a far superior and safer alternative, offering better chip control and tool life.
Milling D2 Steel
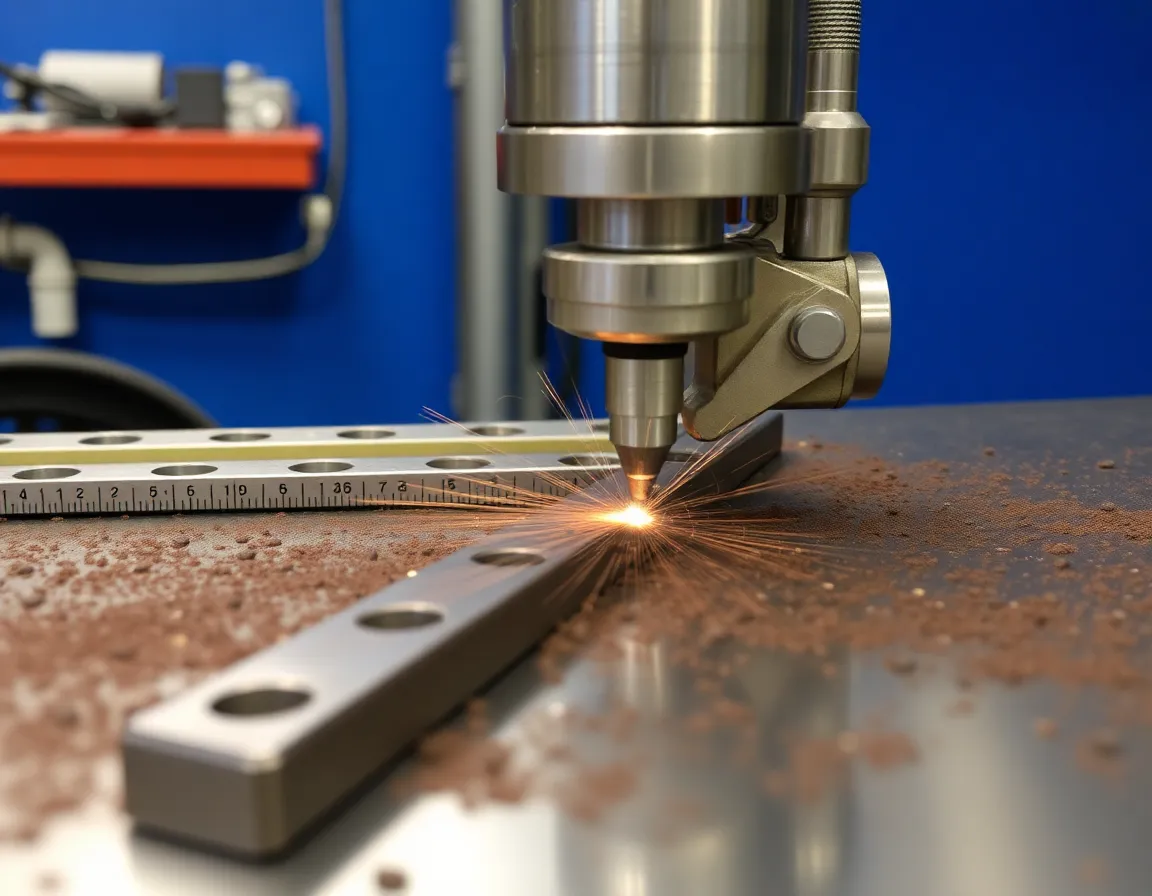
As discussed, rigidity is paramount. Use the largest diameter, shortest flute length end mill possible for the job. For roughing, consider tools with a corner radius (bull nose) to strengthen the cutting edge. For finishing, sharp, fine-grained carbide end mills with a good coating will yield the best surface finish. Always use a toolpath that maintains constant tool engagement to avoid shock loading.
Post-Machining and Heat Treatment Considerations
The journey with D2 doesn't end at the machine. Proper handling after machining ensures the final product meets specifications.
After roughing and semi-finishing in the annealed state, components are sent for heat treatment. It is crucial to leave a uniform stock allowance for finishing—typically 0.010" to 0.020" per side for grinding after hardening. This removes the decarburized layer and any distortion from the heat treat process. Stress relieving the material after heavy roughing operations, before final semi-finishing, can help minimize movement during the final hardening.
Once hardened (58-62 HRC), further machining is limited. Grinding is the primary method for achieving final dimensions and surface finish on hardened D2. Use appropriate grinding wheels (like aluminum oxide or CBN) and techniques to avoid generating excessive heat, which can cause micro-cracks or soften the material. Electrical Discharge Machining (EDM) is also a highly effective and precise method for working with fully hardened D2.
Conclusion: Patience and Precision Pay Off
Mastering D2 tool steel machining is a testament to a machinist's skill and understanding of material science. It demands respect, careful planning, and disciplined execution. The key takeaways are: machine primarily in the annealed state, prioritize absolute rigidity, select premium carbide tools with appropriate geometry, run conservative but deliberate speeds and feeds, and always plan for the heat treatment process. By adhering to these principles, you can harness the formidable properties of D2 steel—its exceptional wear resistance, ability to hold a sharp edge, and durability under pressure—to create tools, molds, and components that perform reliably in the most demanding applications. The challenge of machining D2 is significant, but the rewards in terms of part performance and professional satisfaction are unparalleled.