
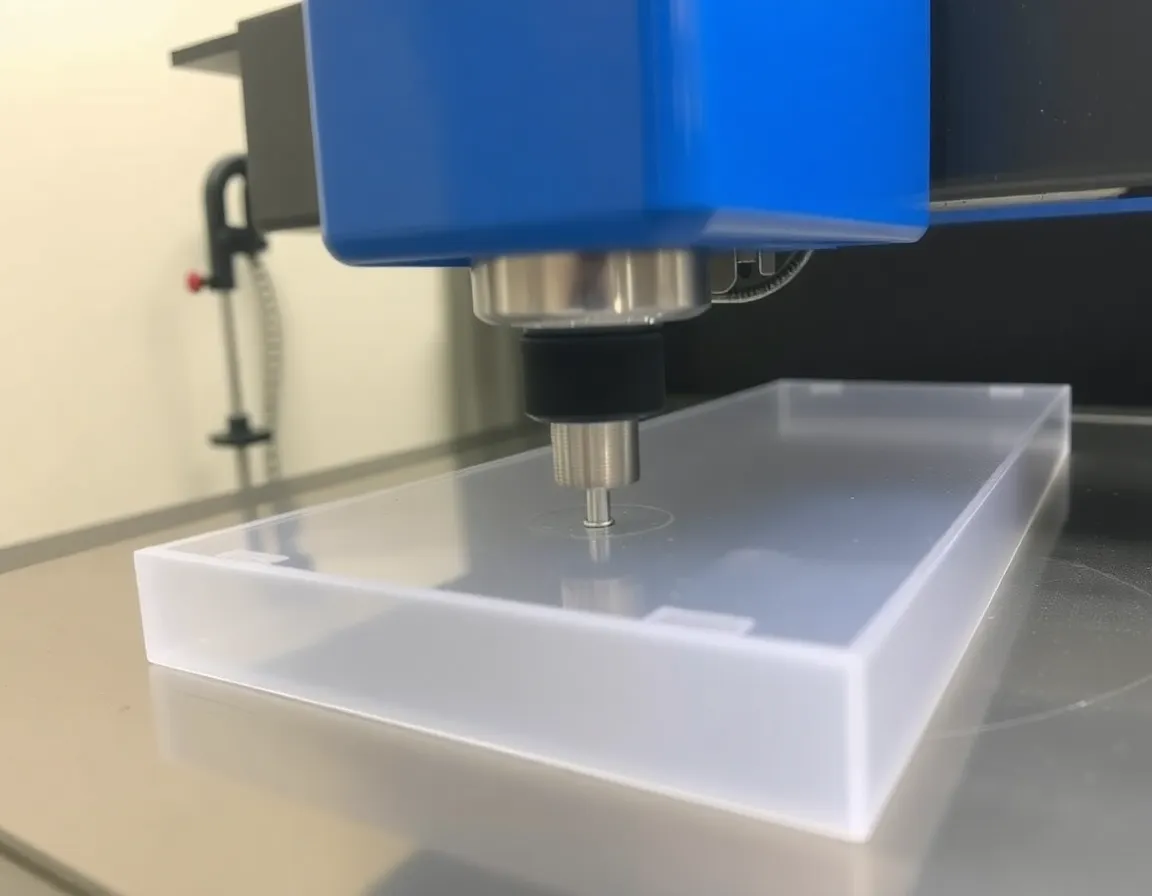
はじめに:ポリカーボネートの可能性と課題
ポリカーボネート(PC)はエンジニアリング熱可塑性プラスチックの中でも巨匠的存在であり、卓越した耐衝撃性、光学透明性、寸法安定性で知られています。防弾窓や医療機器から自動車用レンズや電子部品に至るまで、その用途は多様であると同時に要求が厳しいものです。しかし、ポリカーボネートをこれほど価値あるものにしている特性—その強靭さとわずかな柔軟性—は、機械加工において独自の課題ももたらします。金属やより脆いプラスチックとは異なり、PCは不適切に加工すると、粘着したり、欠けたり、内部応力を生じたりする可能性があります。したがって、ポリカーボネート加工の技術を極めることは、単なるスキルではなく、材料の潜在能力を最大限に引き出す完璧で高性能な部品を製作するための必須条件です。.
材料の理解:ポリカーボネートが異なる挙動を示す理由
ツールパスやパラメータの話に入る前に、扱う材料を理解することが重要です。ポリカーボネートは非晶性熱可塑性プラスチックであり、明確な融点を持たず、加熱すると徐々に軟化します。この特性が、ほとんどの機械加工上の考慮事項の根本にあります。.
加工性に影響を与える主な材料特性
ポリカーボネートの高い耐衝撃性は、粉々に割れるのではなくエネルギーを吸収することを意味し、きれいに切断するには鋭利な工具が必要です。その低い熱伝導率により熱が切れ刃に集中し、材料の軟化、溶融、そして工具や部品への再溶着を引き起こす可能性があります。さらに、PCは中程度の吸湿率を持ちます。十分に乾燥されていないシートを加工すると、蒸気泡や表面の欠陥が生じることがあります。これらの固有の特性を認識することが、それらを克服するための第一歩です。.
機械加工 vs. 成形:適切なプロセスの選択
While polycarbonate is excellent for CNC machining, especially for prototypes and low-to-medium volume production, it's also widely used in injection molding and thermoforming for high-volume parts. Machining is ideal for complex geometries, tight tolerances, and parts where the cost of a mold is prohibitive. The goal is to achieve molded-quality finishes and integrity through subtractive manufacturing.
The Machining Toolkit: Best Practices for Perfect Cuts
Success in polycarbonate machining hinges on a meticulous approach to tool selection, machine setup, and cutting parameters. Deviating from best practices can lead to poor surface finish, dimensional inaccuracy, and compromised mechanical properties.
Tool Selection: Geometry and Material
Using the correct cutter is non-negotiable. For polycarbonate, single or double-flute end mills are preferred as they provide ample chip clearance. Tools should be razor-sharp, typically with a high positive rake angle (10°-20°) to shear the material cleanly rather than pushing and deforming it. Carbide tools are recommended for their sharpness retention and wear resistance. For drilling, use straight-flute or slow-spiral "plastic" drills designed to lift chips out without generating excessive heat. Diamond-tipped tools can provide an exceptional finish for critical optical applications.
Machine Parameters: Speed, Feed, and Coolant
Balancing speed and feed is the art of managing heat generation. The general principle is to use high spindle speeds and consistent, moderate to high feed rates. A slow feed allows the tool to rub rather than cut, generating friction and heat. A good starting point is a spindle speed of 10,000-18,000 RPM and a feed rate that ensures a continuous, clean chip formation.
Coolant is essential, but the type matters. Compressed air is excellent for clearing chips and providing cooling. For flood cooling, use a water-soluble coolant or, even better, a mist system. Avoid aggressive petroleum-based coolants as they can cause stress cracking in polycarbonate. The primary roles of coolant are to:
- Dissipate heat from the cutting zone.
- Lubricate to reduce friction.
- Efficiently evacuate chips to prevent re-cutting.
Workholding and Stress Mitigation
Polycarbonate sheets must be securely clamped to prevent vibration, which can cause chatter marks. However, excessive clamping force can induce internal stresses. Use soft jaws or protective pads to distribute pressure evenly. To prevent stress cracking, especially when machining near edges, it is often advisable to anneal the material before final machining or to relieve stress by baking the finished part according to the manufacturer's specifications.
Advanced Techniques for Specific Operations
Different machining operations require nuanced adjustments to the general rules. Here’s a breakdown of key processes.
Milling and Routing
Climb milling (where the cutter rotates in the same direction as the feed) is generally preferred for polycarbonate as it produces a cleaner finish and reduces tool deflection. For deep pockets, use trochoidal milling paths to distribute tool engagement and heat generation. Always leave a small finishing pass (0.010-0.020 inches) to ensure a superb final surface.
穴あけとタップ加工
Peck drilling is highly recommended. This technique involves retracting the drill periodically to break and clear chips, preventing binding and heat buildup. For through-holes, back up the material with a sacrificial wood or plastic block to prevent breakout and "chip-lip" on the exit side. When tapping, use taps with polished flutes and a generous relief angle. Oversize the tap drill slightly to reduce friction and the risk of cracking.
Sawing and Turning
For sawing, use fine-toothed blades (at least 10 teeth per inch) with a neutral or slightly negative rake. Band saws and circular saws should run at high speeds with a slow, steady feed. In turning operations on a lathe, tools must have a sharp, highly polished rake face. Employ a constant, positive feed to achieve a continuous chip and a smooth surface on the workpiece.
Post-Processing: From Machined Part to Finished Product
The journey doesn't end when the machining stops. Proper post-processing is vital for achieving optical clarity, specific aesthetic qualities, and enhanced durability.
Deburring and Edge Finishing
Light burrs can be removed with a sharp blade or fine abrasive paper (400-grit or higher). For a polished edge, use a flame polishing technique (for experienced operators only) or a multi-step sanding and buffing process, progressing through increasingly fine abrasives and finally a plastic polishing compound.
Stress Relieving and Annealing
Machining induces localized stresses. For critical applications, annealing the finished parts is essential. This involves heating the parts to a temperature below the distortion point (typically 250-275°F or 120-135°C) for several hours and then allowing them to cool slowly and uniformly. This process restores the material's original toughness and prevents future stress cracking.
Protective Coatings and Cleaning
Polycarbonate is susceptible to scratching. Applying a hard-coat, either through dip or spray, can dramatically improve surface hardness and abrasion resistance. Always clean parts with a mild soap solution and soft cloth; avoid harsh solvents like acetone, ketones, or aromatic hydrocarbons, which can cause immediate crazing and cracking.
Conclusion: The Path to Polycarbonate Mastery
Mastering polycarbonate machining is a systematic pursuit of precision that respects the material's unique characteristics. It begins with selecting sharp, appropriate tools and configuring machine parameters to manage heat and ensure clean chip evacuation. It demands attention to detail in workholding and stress management, and it is perfected through careful post-processing. By adhering to these principles—prioritizing sharpness, controlling heat, and mitigating stress—manufacturers and machinists can consistently produce perfect polycarbonate parts. These parts will not only meet stringent dimensional and aesthetic specifications but will also fully embody the remarkable durability and clarity that make polycarbonate the material of choice for the world's most challenging applications. The bridge between a raw sheet of PC and a flawless finished component is built on knowledge, patience, and disciplined technique.