Zamakを理解する:合金の概要
精密加工とダイカストの世界において、Zamakは多用途で広く使用される亜鉛合金ファミリーとして際立っています。その名称自体は、主要元素のドイツ語名に由来する頭字語です: Zink(亜鉛)、Aluminium(アルミニウム)、Magnesium(マグネシウム)、Kupfer(銅). 主にZamak 3とZamak 5が業界の主力であり、Zamak 3は物理的特性と鋳造性の優れたバランスから最も一般的です。これらの合金は高い強度、優れた寸法安定性、卓越した表面仕上げ能力で知られ、複雑な自動車部品から耐久性のあるハードウェア、家電製品に至るまで、幅広い部品に最適です。.
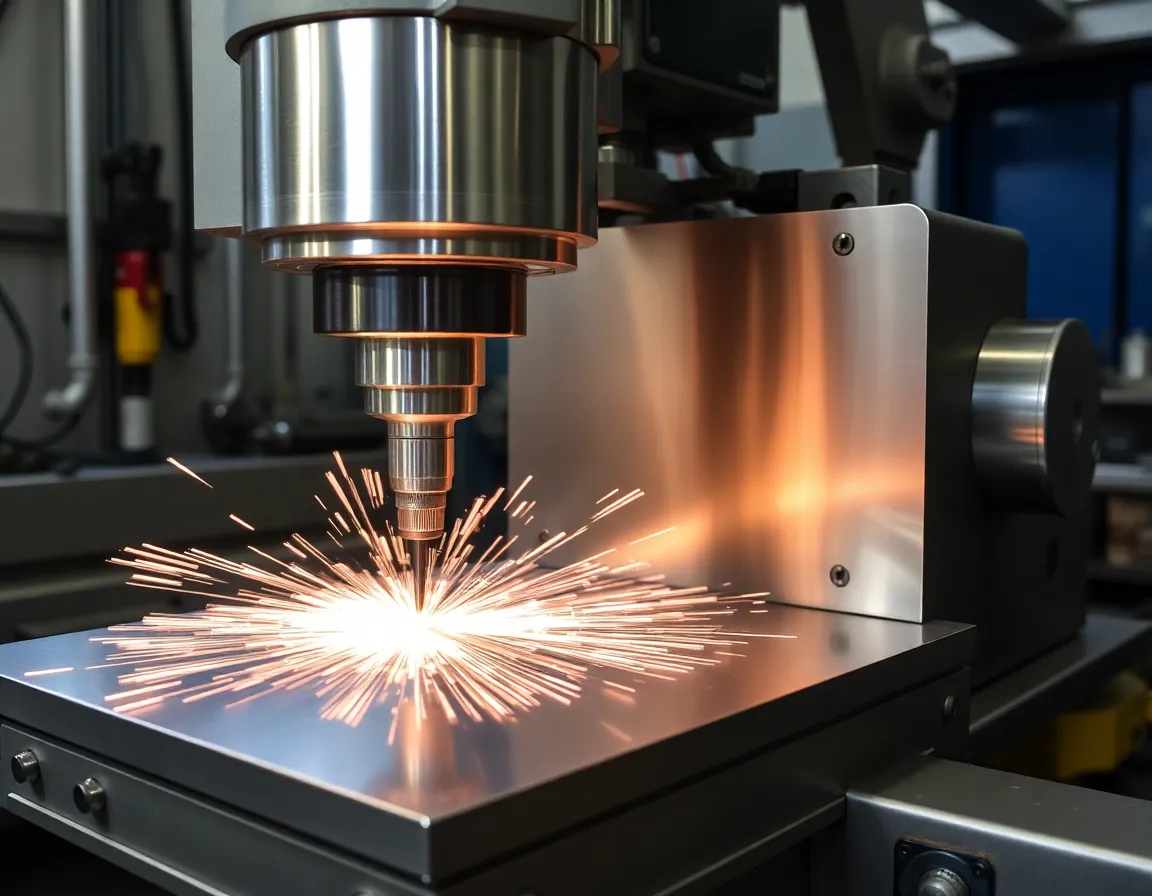
Zamakの被削性は一般に非常に良好とされていますが、細かな注意点も存在します。鋼のような硬い金属の加工とは異なり、Zamakは比較的低い融点やかじり付きの可能性といった欠点を避けつつ利点を活かすために、特有のアプローチが必要です。ダイカスト部品への二次加工であれ、素材からの削り出しであれ、Zamak部品の加工を成功させる鍵は、その材料特性を理解し、適切な技術を適用することにあります。.
Zamak加工を成功させるための基本原則
Zamak加工の習得は、その独自の特性を尊重することから始まります。低い融点(Zamak 3で約385°C / 725°F)は、材料の軟化や切削工具への付着を防ぐため、熱管理が極めて重要であることを意味します。さらに、Zamakの優れた延性は、工具が鋭利でない場合やパラメータが不適切な場合に構成刃先(BUE)を引き起こす可能性があります。以下の基本原則を守ることで、精度と効率の基盤が築かれます。.
工具選定:精度の基盤
Choosing the right cutting tool is paramount. For most Zamak machining operations, sharp, polished tools with positive rake angles are highly recommended.
- 材料: Uncoated carbide or micro-grain carbide tools are excellent choices for their hardness and ability to maintain a keen edge. High-speed steel (HSS) can be used but may wear faster on production runs.
- 形状: Tools with high positive rake angles (e.g., 10° to 20°) shear the material cleanly with less cutting force, minimizing heat generation and preventing material pull. Sharp, polished flutes help in efficient chip evacuation.
- コーティング: While not always necessary, polished diamond-like carbon (DLC) or titanium-based coatings can reduce friction and further prevent material adhesion.
Machining Parameters: Speed, Feed, and Depth of Cut
Optimizing your machine settings is the key to controlling heat and achieving a superior finish.
- 速度(SFM): Zamak allows for high surface speeds. A good starting range is 500-1000 SFM for turning and 300-600 SFM for milling. The goal is to be fast enough to generate thin, clean chips that carry heat away, but not so fast as to generate excessive heat through friction.
- 送り速度: Use a moderately high feed rate. A light feed can cause the tool to rub rather than cut, generating heat and work-hardening the surface. A consistent, assertive feed promotes good chip formation.
- 切込み深さ: Zamak is forgiving, but for finishing passes, light depths of cut (0.005" to 0.020") with a sharp tool will yield the best surface finish. For roughing, deeper cuts are acceptable if the machine rigidity and tool strength allow.
Coolant and Lubrication: Mandatory, Not Optional
While Zamak can be machined dry in some cases, using a coolant or lubricant is strongly advised for precision work. Its primary roles are to control temperature, improve surface finish, and aid in chip evacuation. A flood coolant system with a soluble oil or synthetic fluid is ideal. For smaller operations, a mist coolant system or even a generous application of a cutting oil or kerosene-based lubricant can be effective. The lubricant prevents the soft zinc chips from welding to the tool, a phenomenon known as galling.
Advanced Tips and Tricks for Optimal Results
Beyond the basics, several advanced practices can elevate your Zamak machining from good to exceptional, reducing scrap rates and improving component quality.
Managing Chips and Swarf
Zamak produces long, stringy chips that can be sharp and problematic. To manage this:
- Use chip breakers on your tooling geometry if available.
- Ensure high-pressure coolant is directed at the cutting edge to break and flush chips away.
- Regularly clear chips from the work area to prevent recutting, which damages both the tool and the workpiece surface finish.
Achieving Mirror Finishes
Zamak's natural ability to take a fine finish is one of its biggest advantages. For near-mirror finishes:
- Employ a final, very light finishing pass (0.001" - 0.003") with a freshly sharpened, polished tool.
- Maximize spindle speed while maintaining an appropriate feed rate to avoid rubbing.
- Consider using a single-point diamond tool for ultimate surface quality on critical faces.
- Ensure the workpiece is rigidly held to eliminate any vibration or chatter marks.
Addressing Porosity in Die Cast Parts
When performing secondary machining on die-cast Zamak components, you may encounter subsurface porosity. This can cause tool chatter and poor finish. To mitigate this:
- Use sharp tools and consistent, uninterrupted cuts to bridge porous areas.
- Reduce feed rates slightly when machining over suspected porous zones.
- Consider vibratory finishing or tumbling after machining to help close superficial pores.
Applications and Benefits of Precision-Machined Zamak
The synergy of die casting for near-net-shape production and CNC machining for critical tolerances makes Zamak an unbeatable choice for countless applications.
Key Industry Applications
Precision-machined Zamak components are found everywhere:
- 自動車: Fuel system components, sensor housings, decorative trim, and lock mechanisms.
- コンシューマーエレクトロニクス: Camera bodies, bezels, hardware for mobile devices, and internal structural parts.
- Hardware and Plumbing: High-quality faucet handles, valve bodies, door hardware, and precision gears.
- 医療機器: Housings for handheld instruments and components where EMI/RFI shielding is beneficial.
The Compelling Advantages
Choosing Zamak for machined parts offers a host of benefits:
- コスト効率: The raw material is relatively inexpensive, and its excellent castability and machinability keep manufacturing costs low.
- 高い比強度: Zamak is stronger than many engineering plastics and even some aluminum alloys, allowing for robust yet lightweight designs.
- Superb Surface Finish: It can be polished, plated, painted, or coated with exceptional results, making it perfect for aesthetic parts.
- 寸法安定性: Zamak parts have minimal creep and maintain their shape and tolerances over time and under load.
- Full Recyclability: Scrap and swarf can be 100% recycled, supporting sustainable manufacturing practices.
Conclusion: Embracing the Potential of Zamak
Mastering the machining of Zamak is a valuable skill for any machinist or manufacturing engineer. By understanding its material behavior—respecting its need for sharp tools, appropriate speeds and feeds, and adequate cooling—you can unlock its full potential. The result is the ability to produce high-volume, precision components that are strong, aesthetically pleasing, and cost-competitive. Whether you are performing secondary operations on complex die castings or machining a prototype from solid bar stock, applying these tips and tricks will ensure your Zamak projects are executed with precision, efficiency, and consistently outstanding quality. In the landscape of modern manufacturing, Zamak remains a testament to how a well-understood material, paired with skilled machining, continues to enable innovation across industries.