The Unseen Art of Cutting: An Introduction to Wire EDM
In the high-stakes world of advanced manufacturing, where components must be lighter, stronger, and more complex than ever, traditional cutting tools often reach their limit. How do you machine a part from a material harder than the cutter itself? How do you produce a component with microscopic tolerances, intricate internal features, or a profile that seems to defy geometry? The answer lies in a process that harnesses the power of electricity and precision: Wire Electrical Discharge Machining (Wire EDM). This technology is the cornerstone of creating highly precise "wire cut parts," enabling innovations across aerospace, medical, automotive, and beyond by slicing through the impossible with a strand of wire finer than a human hair.
How Wire EDM Works: Slicing with Sparks
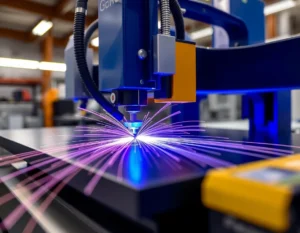
At its core, Wire EDM is a non-contact, thermal machining process. It removes material not with a physical cutting edge, but through a controlled series of rapid, recurring electrical discharges (sparks) between a traveling wire electrode and the workpiece. The workpiece is submerged in a bath of deionized water, which acts as a dielectric fluid to control the spark and flush away microscopic debris.
The Key Components and Process
The process begins with a computer-controlled program, typically generated from a CAD model. The brass or coated wire, ranging from 0.02mm to 0.33mm in diameter, is fed from a spool, travels through the workpiece, and is collected or discarded. A power supply generates the electrical potential between the wire and the workpiece. When they are brought close enough (a gap of about 0.01mm to 0.05mm), the dielectric breaks down, and a spark jumps.
- The Spark: Each spark generates an intense heat channel (around 8,000–12,000°C), instantly melting and vaporizing a microscopic portion of the workpiece.
- The Flush: The deionized water jet cools the area and forcibly ejects the solidified particles, preventing them from re-welding to the surface.
- The Path: The wire, which never actually touches the part, follows the programmed CNC path, and this cycle of sparking and flushing repeats hundreds of thousands of times per second, gradually eroding a precise kerf (cut) through the material.
Multi-Axis Capability: Beyond Flat Profiles
While basic Wire EDM machines cut simple 2D profiles, modern machines offer sophisticated multi-axis movement. The upper wire guide can move independently in the U and V axes, allowing the wire to be tilted relative to the workpiece. This enables the creation of tapered parts and complex 3D shapes with draft angles. For instance, a mold tool might require a cavity with a slight taper for part ejection—a task wire EDM performs with ease by dynamically adjusting the wire's tilt throughout the cut.
The Compelling Advantages of Wire Cut Parts
The unique nature of the Wire EDM process confers a suite of benefits that make it indispensable for specific manufacturing challenges.
Unmatched Precision and Complexity
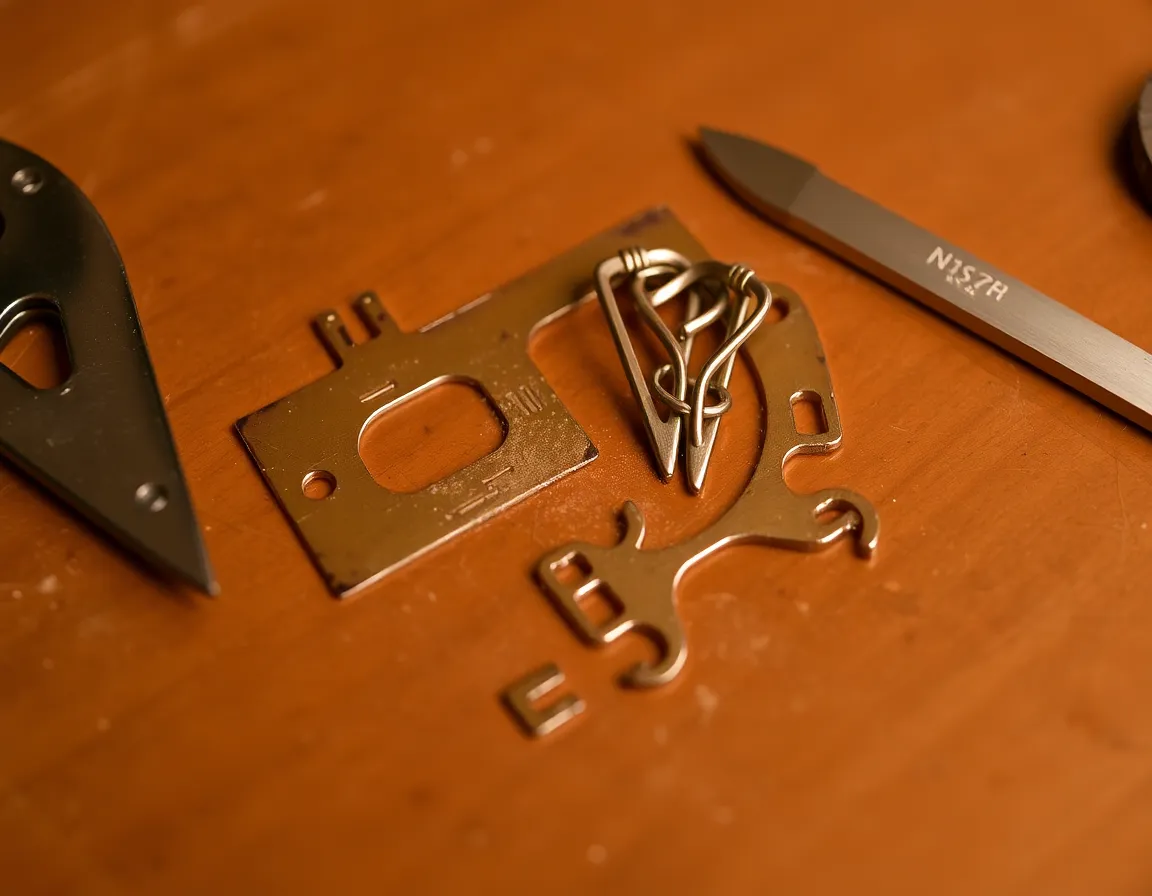
Wire EDM is renowned for its exceptional accuracy, routinely holding tolerances within ±0.0002" (0.005mm) or better. This, combined with the lack of cutting forces, allows for the production of extraordinarily complex and delicate features that would be impossible or prohibitively expensive with conventional machining. This includes:
- Sharp internal corners (not limited by cutter radius).
- Extremely fine details and thin walls.
- Intricate profiles and micro-sized components.
Material Independence and Integrity
Since hardness is irrelevant to the spark erosion process, Wire EDM excels at machining exotic, hardened, or otherwise "unmachinable" materials. This includes tool steels, carbides, titanium, Inconel, and polycrystalline diamond. Furthermore, as there is no direct contact, no mechanical stresses are imparted to the workpiece. This prevents distortion, burr formation, and micro-cracking, which is critical for heat-treated parts and fragile materials.
Superior Surface Finish and Repeatability
The process can achieve very fine surface finishes, often eliminating the need for secondary polishing, especially in mold and die applications. Modern machines use multiple "passes" or "skim cuts," where the wire makes successive traces with lower power settings to refine the surface. Once a program is perfected, an identical part can be produced months or years later with absolute consistency, making it ideal for prototyping and production.
Where Wire Cut Parts Are Essential: Key Applications
The capabilities of Wire EDM make it the go-to technology in several high-tech industries.
Tool and Die Making
This is the traditional and most widespread application. Wire EDM is used to create:
- Stamping and Blanking Dies: For producing intricate metal parts, like electrical contacts or automotive components.
- Injection Molds and Extrusion Dies: For creating complex cores, cavities, and nozzles, often with necessary tapers.
- Fineblanking Dies: Where extreme precision and clean, shear-cut edges are required.
Aerospace and Medical Devices
These sectors demand components made from tough alloys with high reliability. Wire cut parts here include:
- Turbine blades, fuel system components, and structural parts in aerospace.
- Surgical tools, implants (like bone screws and plates), and diagnostic device components in medical.
Prototyping and Small-Batch Production
For engineers developing new products, Wire EDM allows for the rapid creation of functional prototypes directly from hardened materials, providing true performance data. It is also cost-effective for low-volume production runs of complex parts, as it avoids the high cost of dedicated hard tooling.
Electronics and Micromechanics
The ability to cut extremely fine features makes Wire EDM perfect for creating small gears, micro-actuators, and specialized components for electronic packaging and sensors.
Best Practices for Optimal Wire EDM Results
To fully leverage the power of Wire EDM and ensure the highest quality wire cut parts, manufacturers adhere to several key practices.
Design for Manufacturability (DFM)
Designers should collaborate with EDM technicians early. Considerations include:
- Specifying appropriate corner radii (slightly larger than the wire radius plus the spark gap).
- Minimizing the depth of cut for small openings to improve flushing and accuracy.
- Providing adequate start holes (pre-drilled holes for the wire to thread through) in the correct locations.
Strategic Setup and Programming
Proper workpiece fixturing and alignment are critical. Programmers must optimize cutting paths, wire speeds, and power settings (on-time, off-time, voltage) based on the material thickness, desired finish, and required accuracy. Using multiple skim cuts is standard for achieving fine finishes.
Material Preparation and Maintenance
Starting with properly stress-relieved material prevents distortion during machining. Furthermore, maintaining the machine—including regular replacement of filters, resins in the dielectric system, and wire guides—is essential for consistent performance and part quality. Monitoring and adjusting the conductivity of the deionized water is also a constant requirement.
Conclusion: The Cutting Edge of Possibility
Precision Wire EDM is far more than just a machining alternative; it is an enabling technology that expands the boundaries of design and engineering. By transforming electrically conductive materials into complex, high-tolerance components without compromise, it sits at the heart of modern manufacturing innovation. From the medical implant that saves a life to the jet engine component that withstands extreme forces, wire cut parts are a testament to the marriage of digital precision and controlled elemental power. As materials advance and designs grow more ambitious, Wire EDM will continue to be the silent, sparking force that cuts a path toward the future.