
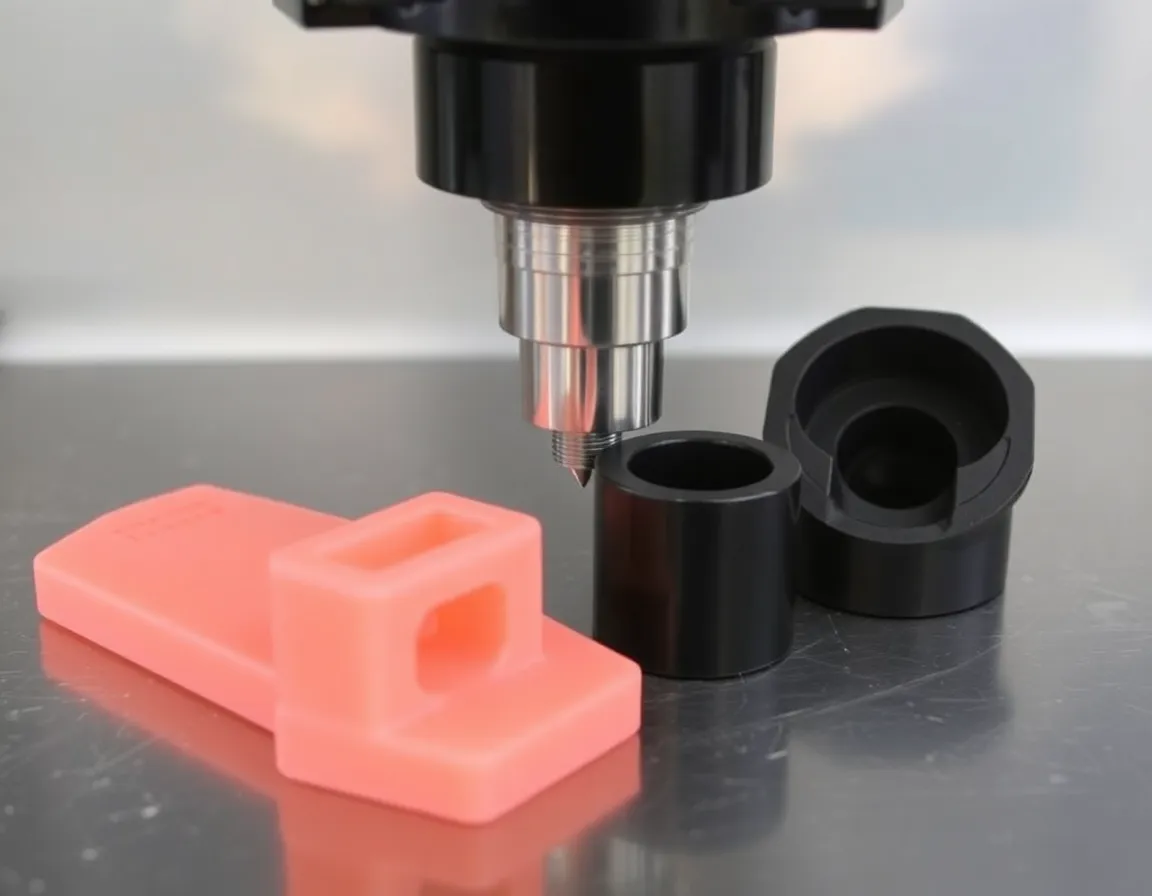
Introduction to Nylon CNC Machining
Nylon CNC machining is a specialized manufacturing process that utilizes Computer Numerical Control (CNC) technology to precisely shape, cut, and finish nylon components. Nylon, also known as polyamide (PA), is a versatile engineering thermoplastic renowned for its exceptional mechanical properties, including high tensile strength, excellent wear resistance, low friction coefficient, and good chemical stability. When combined with the precision and repeatability of CNC machining, nylon becomes an ideal material for producing complex, high-performance parts across industries such as automotive, aerospace, medical devices, consumer electronics, and industrial machinery.
Unlike injection molding or 3D printing, CNC machining of nylon offers unique advantages for prototyping, low-to-medium volume production, and parts requiring tight tolerances. The process involves removing material from a solid nylon block or rod using computer-guided cutting tools, resulting in components with superior surface finishes and dimensional accuracy. This article explores the fundamentals of nylon CNC machining, its benefits, applications, best practices, and key considerations for engineers and manufacturers.
Understanding Nylon as a Machining Material
Types of Nylon Used in CNC Machining
Several grades of nylon are commonly machined, each offering distinct properties:
- Nylon 6 (PA6): The most widely used grade, offering a balance of strength, toughness, and machinability. It absorbs moisture more readily than other nylons, which can affect dimensional stability.
- Nylon 6/6 (PA66):Higher melting point and greater mechanical strength compared to Nylon 6. It is often preferred for high-temperature applications and parts requiring superior rigidity.
- Nylon 12 (PA12):Lower moisture absorption and better dimensional stability, making it suitable for precision components and applications in humid environments.
- Glass-Filled Nylon:Reinforced with glass fibers (typically 30% or 40%) to enhance stiffness, tensile strength, and heat resistance. However, it is more abrasive on cutting tools.
- Molybdenum Disulfide (MoS2) Filled Nylon:Contains lubricating additives to reduce friction and wear, ideal for bearings, bushings, and sliding components.
Key Material Properties Affecting Machining
Nylon exhibits several characteristics that influence CNC machining parameters:
- Low Thermal Conductivity: Nylon retains heat during machining, which can cause melting or gumming if cutting speeds and feeds are not properly controlled.
- Assorbimento di umidità:Nylon can absorb up to 8% moisture by weight, leading to dimensional changes. Pre-drying the material before machining is often necessary for tight tolerances.
- Elasticity and Flexibility:Thin-walled nylon parts may deflect under cutting forces, requiring careful fixturing and reduced tool pressure.
- Riempitivi abrasivi:Glass or carbon fiber reinforcements accelerate tool wear, necessitating the use of carbide or diamond-coated tools.
CNC Machining Processes for Nylon
Milling Nylon Components
CNC milling is the most common process for machining nylon parts. It involves rotating cutting tools that traverse along multiple axes to remove material. Key considerations for milling nylon include:
- Selezione degli utensili: Use sharp, polished carbide end mills with two or three flutes. Polished flutes reduce friction and prevent material buildup. For glass-filled nylons, diamond-coated tools extend tool life significantly.
- Speeds and Feeds:Moderate spindle speeds (8,000–15,000 RPM) and higher feed rates (0.005–0.015 inches per tooth) help prevent heat buildup. Avoid excessive speeds that can melt the material.
- Uso del refrigerante:Air blast or mist coolant is recommended to evacuate chips and cool the cutting zone. Flood coolant can cause nylon to swell due to moisture absorption.
- Climb Milling:Prefer climb milling (conventional direction) to reduce heat generation and improve surface finish. Conventional milling may cause smearing.
Turning Nylon on CNC Lathes
CNC turning produces cylindrical nylon parts such as shafts, rollers, and bushings. Best practices include:
- Insert Geometry: Use sharp, positive rake inserts with polished surfaces. Diamond or CBN (cubic boron nitride) inserts are ideal for filled nylons.
- Cutting Parameters:Moderate cutting speeds (500–1,000 SFM) and light to moderate depths of cut (0.020–0.100 inches). Higher feed rates (0.005–0.020 inches per revolution) help break chips.
- Controllo dei trucioli:Nylon produces stringy, continuous chips that can wrap around the workpiece or tool. Use chip breakers or pecking cycles to manage chip evacuation.
Drilling and Tapping Nylon
Drilling holes in nylon requires attention to heat management:
- Drill Bits: Use standard high-speed steel (HSS) or carbide drills with a 118° to 135° point angle. Peck drilling (incremental retraction) prevents chip clogging and heat buildup.
- Reaming:For precise hole diameters, ream with carbide reamers at low speeds (200–400 RPM) and use coolant to avoid melting.
- Tapping:Form taps (thread forming) are preferred over cut taps because they displace material without generating chips. Use tapping fluid or lubricant to reduce friction.
Benefits of CNC Machining Nylon
CNC machining offers several distinct advantages over alternative manufacturing methods for nylon parts:
- High Precision and Tight Tolerances: CNC machines can achieve tolerances as tight as ±0.001 inches (0.025 mm), making nylon suitable for precision components like gears, bearings, and medical implants.
- No Tooling Costs:Unlike injection molding, CNC machining does not require expensive molds or dies, making it cost-effective for prototypes and small production runs (1–1,000 parts).
- Geometrie complesse:Multi-axis CNC machines (3-axis, 4-axis, and 5-axis) can produce intricate shapes, undercuts, and internal features that are difficult or impossible with other processes.
- Finitura superficiale eccellente:Machined nylon parts have a smooth, glossy surface (Ra 0.4–1.6 µm) that often requires no secondary finishing operations.
- Material Versatility:CNC machining can handle all nylon grades, including filled and unfilled variants, allowing engineers to select the optimal material for their application.
- Fast Turnaround:Prototypes and low-volume parts can be produced in days, compared to weeks for injection molding tooling.
Applications of Nylon CNC Machined Parts
Settore automobilistico
Nylon CNC machining is widely used in automotive applications due to its lightweight, durability, and resistance to fuels and oils. Common parts include:
- Engine components: intake manifolds, valve covers, and timing chain guides
- Transmission bushings and thrust washers
- Brake system components: pistons, seals, and wear pads
- Fuel system parts: connectors, fittings, and filters
Aerospazio e Difesa
In aerospace, nylon’s high strength-to-weight ratio and fatigue resistance make it ideal for:
- Structural brackets and clips
- Insulating spacers and standoffs
- Cable management components
- Lightweight fasteners and inserts
Dispositivi medici
Medical-grade nylons (e.g., Nylon 12) are biocompatible and sterilizable, enabling applications such as:
- Surgical instrument handles and grips
- Diagnostic equipment housings
- Prosthetic components
- Catheter fittings and connectors
Macchinari industriali
Nylon’s low friction and wear resistance are exploited in industrial settings for:
- Conveyor system rollers and guides
- Gears, pulleys, and sprockets
- Bearings and bushings in food processing equipment
- Wear strips and slide pads
Elettronica di consumo
Nylon CNC parts are found in electronic devices for their insulating properties and aesthetic finish:
- Smartphone and tablet frames
- Headphone housings and ear cups
- Camera lens mounts and adapters
- Protective cases and enclosures
Best Practices for Successful Nylon CNC Machining
Preparazione del materiale
Proper material handling is critical to achieving consistent results:
- Pre-drying: Dry nylon stock in a convection oven at 80–90°C (176–194°F) for 2–4 hours before machining to remove absorbed moisture. This prevents dimensional changes and surface defects.
- Storage:Store nylon in sealed containers with desiccant to minimize moisture absorption. Avoid exposure to direct sunlight or high humidity.
- Ricottura:For stress-relieving, anneal machined parts at 150°C (302°F) for 1–2 hours, then slow cool to reduce internal stresses and improve dimensional stability.
Tooling and Cutting Parameters
Optimizing tooling choices and machining parameters prevents common issues:
- Use Sharp Tools: Dull tools generate excessive heat, causing melting, burrs, and poor surface finish. Inspect tools frequently and replace them at the first sign of wear.
- Control Chip Evacuation:Use compressed air or vacuum systems to remove chips from the cutting zone. Chips left in place can recut, causing heat buildup and surface damage.
- Avoid Overheating:Reduce spindle speeds and increase feed rates if signs of melting (smearing, discoloration) appear. Consider using coolant mist or cryogenic cooling (liquid nitrogen) for high-volume production.
- Fixture Rigidly:Use vacuum chucks, soft jaws, or custom fixtures to hold nylon workpieces securely. Thin parts may require support to prevent deflection.
Post-Machining Operations
After machining, additional steps may be required:
- Sbavatura: Remove sharp edges and burrs using manual deburring tools, abrasive pads, or tumbling. Nylon burrs are typically soft and easy to remove.
- Surface Finishing:For matte or textured surfaces, use sandblasting or chemical etching. Polishing with a buffing wheel can achieve a high-gloss finish.
- Dimensional Inspection:Measure critical features after machining, as nylon can relax or expand slightly after cutting. Allow parts to stabilize for 24 hours before final inspection.
- Moisture Conditioning:For parts exposed to humid environments, moisture conditioning (e.g., immersion in water at 50°C for 1 hour) can stabilize dimensions and improve toughness.
Common Challenges and Solutions
Melting and Smearing
Problem:Excessive heat causes nylon to melt, resulting in a gummy surface or tool clogging.
Soluzione:Reduce spindle speed, increase feed rate, use sharp tools, and apply air blast cooling. Avoid dwell or prolonged contact between tool and workpiece.
Burr Formation
Problem:Soft burrs form along edges, especially during drilling and milling.
Soluzione:Use sharp tools with polished flutes, climb mill where possible, and employ deburring tools as a secondary operation. For drilling, use a back-up material to support the exit hole.
Dimensional Instability
Problem:Parts change size after machining due to moisture absorption or stress relief.
Soluzione:Pre-dry material, anneal parts after roughing, and machine with light finishing passes. Allow parts to stabilize before final inspection.
Tool Wear (Filled Nylons)
Problem:Glass or carbon fiber fillers rapidly wear down standard HSS tools.
Soluzione:Use carbide tools with diamond-like carbon (DLC) or PCD (polycrystalline diamond) coatings. Reduce cutting speeds and use coolant to extend tool life.
Conclusione
Nylon CNC machining is a highly capable and versatile manufacturing process that bridges the gap between material performance and precision engineering. By understanding the unique properties of different nylon grades and applying best practices in tool selection, cutting parameters, and post-processing, manufacturers can produce components that meet demanding requirements in terms of strength, wear resistance, and dimensional accuracy.
Whether for rapid prototyping, low-volume production, or high-performance end-use parts, CNC machining of nylon offers a cost-effective and reliable solution. As industries continue to demand lighter, stronger, and more durable components, the role of nylon CNC machining will only grow. By staying informed about material advancements, tooling technologies, and process optimization, engineers and machinists can unlock the full potential of this remarkable engineering thermoplastic.