
Por qué la mayoría de los proyectos de acabado CNC tienen problemas antes incluso de comenzar
En un hilo reciente de Reddit en r/Manufacturing, un usuario publicó: “Cotizamos carcasas de aluminio anodizado con tres proveedores. Dos entregaron piezas con discrepancia de color; el tercero tenía picaduras alrededor de los agujeros roscados. Perdimos seis semanas y un cliente”. El problema no era la falta de capacidad técnica, sino una desconexión entre el lenguaje de especificación del comprador y la interpretación del taller de “suficientemente bueno”. Las fallas de acabado rara vez ocurren de forma aislada. Se remontan a uno de estos puntos problemáticos recurrentes:
- Indicaciones de rugosidad ambiguas: Pedir “liso” sin especificar Ra o Rz deja un margen infinito para el error. Un ingeniero en el grupo de mecanizado CNC de Facebook admitió que su plano simplemente indicaba “pulir a espejo”, y recibió piezas que reflejaban pero perdieron 0,05 mm en datos críticos.
- Incompatibilidad entre material y acabado: No todas las aleaciones se anodizan limpiamente. El aluminio 7075 puede desarrollar un tinte amarillento, mientras que el 6061 da ese acabado nítido transparente o teñido. Los talleres que no señalan esto a tiempo crean dolores de cabeza posteriores.
- Contaminación posterior al mecanizado: Los residuos de fluido de corte, las huellas dactilares o el polvo de embalaje se convierten en defectos bajo el recubrimiento. Unos minutos de manipulación inadecuada pueden arruinar un lote.
- Daños logísticos: Las superficies con acabados impecables se rayan cuando el embalaje no está diseñado para el transporte marítimo o la manipulación por mensajería.
Estos problemas no son exclusivos de un solo país, pero al trabajar con un china cnc finishing services co. ltd socio, la diferencia horaria y la barrera idiomática pueden hacer que un pequeño malentendido resulte costoso. La solución radica en comprender lo suficientemente bien el proceso de acabado como para hacer preguntas precisas, y en seleccionar un socio que considere el acabado una competencia central, y no una ocurrencia tardía.
¿Qué son exactamente los servicios de acabado CNC? Más allá de la definición básica
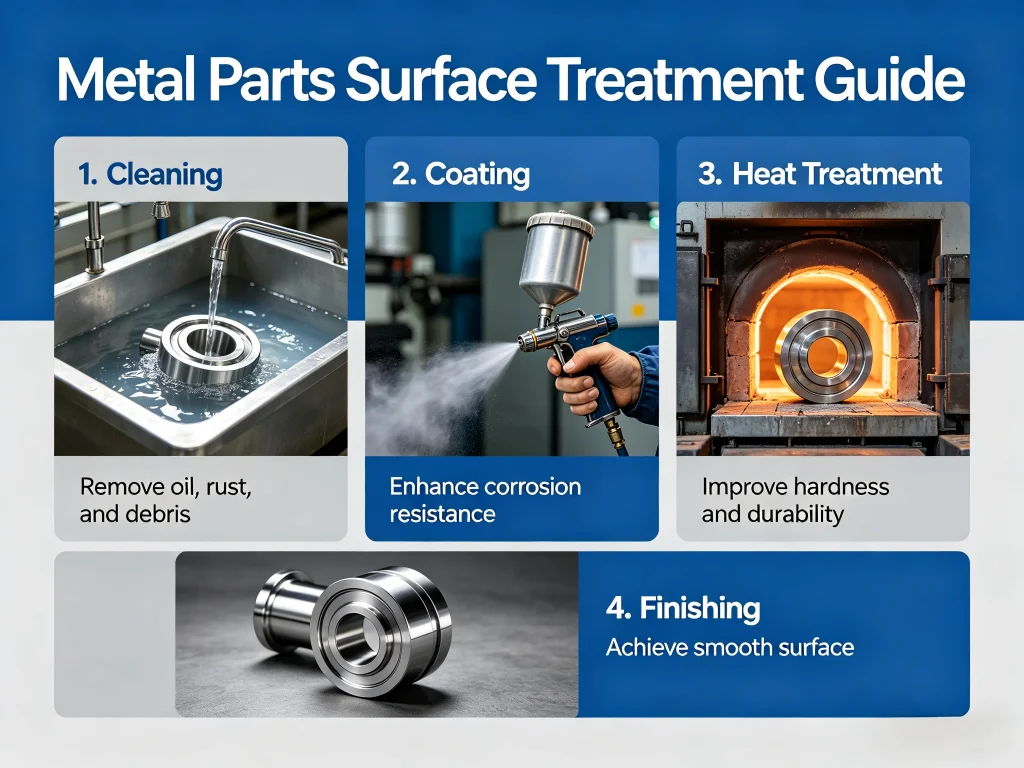
El acabado CNC abarca toda operación a nivel de superficie que se realiza sobre una pieza mecanizada después del proceso de arranque de viruta, además de ciertos pasos en proceso que combinan mecanizado y acabado. No se trata simplemente de “hacer que se vea bien”. En esencia, el acabado modifica la capa más externa para lograr propiedades funcionales específicas: resistencia a la corrosión, conductividad eléctrica, biocompatibilidad, control de la fricción, reflectividad óptica o prolongación de la vida a la fatiga. Un china cnc finishing services ltd proveedor que entiende este papel multidimensional normalmente organizará sus capacidades en tres categorías:
- Acabado mecánico: Procesos como el granallado con microesferas, el cepillado, el pulido, el tamboreado y el desbarbado vibratorio que alteran físicamente la textura superficial. Estos pueden lograr valores de Ra desde 0,8 µm (mecanizado estándar) hasta 0,05 µm (pulido de grado óptico). Un colaborador de Reddit en r/CNC compartió un ejemplo en el que un simple granallado con microesferas de vidrio duplicó la vida a la fatiga de un soporte de acero inoxidable 17-4 PH con carga cíclica al introducir tensión residual compresiva.
- Acabado químico y electroquímico: Anodizado (Tipo II, Tipo III hardcoat), recubrimiento de conversión con cromato (Alodine), pasivado para acero inoxidable, electropulido y grabado químico. Cada uno altera la química de la superficie. El anodizado duro, por ejemplo, crea una capa de óxido de 25-75 µm que puede elevar la dureza superficial por encima de 60 HRC, algo crucial para aplicaciones de desgaste por deslizamiento.
- Recubrimientos aplicados: Recubrimiento en polvo, pintura húmeda, PVD (deposición física de vapor), impregnación con Teflón/PTFE e incluso marcado láser para trazabilidad. Estos añaden material a la superficie en lugar de restarlo.
Cuando un china cnc finishing services inc la operación reúne los tres bajo un solo sistema de calidad, la pieza no viaja entre subcontratistas. Esto importa porque cada traspaso introduce riesgo de programación y variación de calidad. En jucheng, el flujo de trabajo pasa de los centros de mecanizado de 5 ejes directamente a las líneas de acabado internas, con inspección de primera pieza en cada transición—un modelo que imita la integración vertical preferida por los principales de la industria aeroespacial pero adaptada para trabajo de prototipo a volumen medio.
Cómo funciona el acabado CNC: un recorrido paso a paso con tolerancias reales
Tracemos un soporte óptico típico de aluminio 6061-T6 desde el tocho en bruto hasta el producto terminado, para que pueda ver dónde se gana—y se pierde—precisión. Comprender esta secuencia ayuda cuando revisa las hojas de proceso de un posible china cnc finishing services llc proveedor.
Paso 1: Mecanizado previo al acabado
La pieza se fresca y taladra con 0,1-0,2 mm de material adicional en las superficies designadas para el acabado. Este “margen de mecanizado” tiene en cuenta la eliminación de material que consumirá el pulido o el granallado. Sin él, características críticas como los agujeros de pasador pueden quedar sobredimensionadas. Los talleres con experiencia en acabado ajustarán las trayectorias de herramienta para evitar rebabas afiladas que luego atrapan el medio.
Paso 2: Limpieza y desengrase
La limpieza ultrasónica o el desengrase por vapor elimina todo el aceite de corte; de lo contrario, los electrolitos de anodizado no mojarán uniformemente. Una hoja de proceso de jucheng que revisamos incluye inmersión ultrasónica de dos etapas con enjuague con agua de ósmosis inversa y secado forzado con aire caliente—un detalle que evitó las manchas de aceite de las que se quejó un usuario de Reddit en un lote recién anodizado.
Paso 3: Preparación de la superficie (mecánica o química)
Dependiendo del acabado deseado, la pieza puede someterse a granallado con microesferas de vidrio de grano 100 a 60 psi, o grabado químico en hidróxido de sodio para eliminar la piel del mecanizado. Los parámetros de granallado—presión, distancia de separación, ángulo de boquilla—se controlan estrictamente. Una presión inconsistente produce acabados irregulares, una queja común en las reseñas de Facebook de talleres de acabado de bajo costo. Para la pasivación del acero inoxidable 304, un baño de ácido cítrico o nítrico disuelve el hierro libre de la superficie, impulsando la formación de óxido de cromo y la resistencia a la picadura.
Paso 4: La operación principal de acabado
Para el anodizado Tipo II, la pieza se convierte en el ánodo en un electrolito de ácido sulfúrico a 18-22 °C. La densidad de corriente (típicamente 1,5 A/dm²) y el tiempo de permanencia dictan la estructura de poros y el espesor de la capa. Un taller basado en datos utiliza rectificadores computarizados que registran las curvas de voltaje; las desviaciones de la curva esperada señalan problemas como mal contacto eléctrico o baños contaminados. De manera similar, el electropulido elimina de forma controlada 0,02-0,05 mm para nivelar los micropicos, creando un acabado Ra 0,1 µm en acero inoxidable que resiste la adhesión bacteriana—un requisito clave para equipos alimentarios y farmacéuticos.
Step 5: Post-Treatment and Sealing
Anodized pores must be sealed, usually in boiling deionized water or a nickel acetate solution, to lock in dye and corrosion resistance. Skipping this step—or using impure water—causes dye bleed and salt-spray failures. A china cnc finishing services co. ltd partner that values long-term performance will run salt-spray tests per ASTM B117 on sample coupons, often sharing the 336-hour or 720-hour results on request.
Step 6: Inspection and Packaging
Surface roughness testers, gloss meters, and color spectrophotometers check against standards. Parts are then packed in VCI (volatile corrosion inhibitor) paper, custom foam inserts, and sealed in moisture-barrier bags. One LinkedIn discussion noted that a $20,000 order of medical device housings was rejected simply because humidity breached the polybag during air freight; the supplier hadn’t added desiccant packs. The best finishing providers treat packaging as part of the manufacturing process.
Where Precision Finishing Matters Most: Application Deep-Dives
Surface finishing isn’t one-size-fits-all. The requirements of a hydraulic valve body are entirely different from those of a drone motor mount. Drawing on conversations across engineering forums and case notes from china cnc finishing services providers, let’s dissect three high-stakes scenarios where getting the finish right is non-negotiable.
Medical and Surgical Instruments
A scalpel handle or bone drill guide demands more than a shiny surface. Electropolishing of 316L stainless removes microburrs that could harbor bacteria, while passivation restores the passive chromium oxide layer damaged during machining. Ra values below 0.2 µm are typical, verified with a profilometer. In one Facebook group exchange, a design engineer recounted how switching from manual polishing to automated electropolishing cut particle generation by 70% in an orthopedic trial. When evaluating a china cnc finishing services ltd for medical work, ask for ISO 13485 certification and full batch traceability. Jucheng’s medical line, as described on their site, maintains dedicated clean finishing cells with documented process validation (IQ/OQ/PQ) packages—something that directly addresses FDA and EU MDR audit demands.
Aerospace and UAV Components
Aircraft brackets and UAV prop hubs are often machined from 7075 aluminum or titanium. Here, finishing choices affect fatigue life directly. Shot peening with cast steel shot introduces compressive stress that inhibits crack initiation. Hard anodizing adds wear resistance to sliding surfaces but must be masked off from threads to prevent embrittlement. A Reddit user on r/AerospaceEngineering detailed a project where Type III anodizing thickness variance caused a 0.02 mm interference fit to become a loose slip fit—emphasizing the need for a shop that compensates for coating growth. Jucheng’s in-house CMM inspection after finishing ensures that coating buildup doesn’t push features out of tolerance, a critical ability when NADCAP-level quality is expected without the associated cost.
Automotive and EV Battery Housings
Electric vehicle battery enclosures made from aluminum extrusions and CNC-machined plates must withstand road salt, vibration, and thermal cycling. Chromate conversion coating (Alodine) provides an electrically conductive, corrosion-resistant surface that bonds well with adhesives and sealants. The finish must cover every internal corner to prevent galvanic corrosion with steel fasteners. On an automotive engineering forum, a member noted that a china cnc finishing services inc facility improved their battery tray yield from 85% to 99% by introducing automated spray Alodine lines with pH monitoring—eliminating the manual wipe-down inconsistencies that caused field failures.
Key Factors When Choosing a CNC Finishing Partner: A Comparison Lens
Procurement teams often default to unit price, but finishing quality has long-term cost implications that a spreadsheet won’t capture. Let’s map the selection variables, framed to help you compare a typical job shop versus a dedicated finishing-focused provider like jucheng. The table below synthesizes feedback from industry groups and hands-on audits.
| Factor | General CNC Shop | Jucheng Integrated Finishing Model |
|---|---|---|
| Finishing Equipment | Subcontracted or limited to manual polishing; few in-house chemical lines | Own anodizing, passivation, electropolishing, bead blasting, and powder coating lines; automated control of critical parameters |
| Certificaciones | Often ISO 9001 only; may lack process-specific certs | ISO 9001:2015, ISO 13485 for medical, material certs per ASTM/AMS; process validation documentation available |
| Garantía de Calidad | Visual inspection common; limited surface metrology | Profilometry, salt-spray chambers, gloss measurement, color spectrophotometers; CMM inspection after finishing |
| Material Expertise | Primarily aluminum and mild steel; may struggle with exotic alloys | Proven with aluminum (6061, 7075, 5083), stainless (304, 316L, 17-4 PH), titanium, brass, and engineered plastics; specific pre-treatment protocols for each |
| Supply Chain | Multiple handoffs; long lead times due to external plating shops | Single-point responsibility; typical finishing turnaround 3-7 working days inside overall project timeline |
| Prototyping to Production | Minimum order quantities can be high for external finishers | 1-10,000+ pieces flexibility; process developed on prototypes directly transfers to production |
| Communication | Language barrier often magnified through middlemen | English-speaking engineering support; detailed process review before first article; real-time updates |
Beyond the table, dig into a supplier’s rejection rate and corrective action process. During a LinkedIn poll, sourcing managers ranked “documented CAPA (Corrective and Preventive Action)” as more predictive of quality than price. A china cnc finishing services llc that opens its quality manual to you is demonstrating confidence—a signal worth weighing heavily.
Precision: The Numbers That Matter
Surface roughness is the universal finishing KPI. For context, here’s what different Ra values mean in practical terms, based on data pulled from machining handbooks and supplier benchmarks:
- Ra 3.2 µm: Typical as-machined finish; visible tool marks; acceptable for general structural parts.
- Ra 1.6 µm: Fine machining or light bead blasting; good for sealing surfaces with gaskets.
- Ra 0.8 µm: Smooth finish suitable for most consumer products and non-critical aerospace components.
- Ra 0.4 µm and below: Requires polishing or electropolishing; used in medical, optical, and high-purity fluid handling. Jucheng’s documented capability for stainless steel electropolishing reaches Ra 0.1 µm, matching requirements for ASME BPE surface finishes.
Lead Time and Delivery Stability
Global supply chains remain volatile. A common frustration aired on Reddit’s r/supplychain is finishing facilities promising two-week turnaround that stretches to six weeks because they batch anodizing colors. The fix: choose a partner with enough in-house capacity to run your parts without waiting for a full tank. Jucheng’s multiple anodizing lines allow partial loads, keeping lead times predictable. They also offer expedited options for prototype builds—something often shared as a case study on their website where a robotics startup got 50 housing units fully anodized and silkscreened within 8 calendar days.
Installation and Maintenance Insights for Finished CNC Components
The moment you receive your finished parts, their long-term performance depends on how you handle, install, and maintain them. Many surface failures emerge post-delivery because of simple oversights. Here are field-tested recommendations gathered from industrial engineers and seasoned technicians.
Receiving Inspection: The First 10 Minutes
Before signing the delivery receipt, open one box per batch and check for condensation inside barrier bags. Use a calibrated white-light lamp to inspect for handling scratches, especially on polished surfaces. Run a cotton-gloved fingertip over critical sealing faces—any snag indicates a burr or nick. If you ordered anodized parts, compare a sample against the approved master color swatch under the same lighting conditions that your end customer will use. A Facebook group for quality managers suggests photographing the parts on receipt and logging the images, creating a traceable baseline before the parts enter your inventory.
Storage Conditions
Anodized aluminum doesn’t need oil, but it does need dry, temperature-stable storage. Fluctuating humidity can cause sealing bloom (a white powdery residue) if the sealing step was marginal. Passivated stainless should be kept away from chlorides—don’t store near bleach or pool chemicals. For PVD-coated parts, stack them with interleaving foam to prevent coating-on-coating contact that could cause micro-fractures. A china cnc finishing services provider like jucheng ships with detailed care instructions; ignoring them voids any latent warranty claims.
Assembly Precautions
When pressing bearings into an anodized bore, the coating’s thickness (often 10-50 µm) reduces the nominal diameter. If the bore wasn’t machined with the coating buildup in mind, you’ll crack the anodic layer or tolerate a loose fit. Lubricate the assembly with a compatible grease, not a dry press. Stainless parts that have been passivated should not be wire-brushed with carbon steel bristles, which embed free iron and restart corrosion exactly where you tried to prevent it.
In-Service Cleaning
For medical instruments, enzymatic cleaners followed by an RO water rinse preserve the passive layer. Avoid bleach or iodine-based disinfectants on anodized aluminum—they attack the dye and the seal. For industrial parts, periodic wipe-down with isopropyl alcohol suffices, but verify chemical compatibility with the coating. If you notice wear spots on hard-anodized parts, investigate alignment rather than blaming the finish; edges under high load will eventually abrade any coating.
Why Jucheng Is a Considered Choice in the CNC Finishing Landscape
Walk through any machining trade show and you’ll find no shortage of companies offering finishing. What differentiates jucheng is a combination of depth and transparency that addresses the core headaches we’ve described. Their operation, accessible at jccncmachining.com, has been shaped by years of cross-industry projects. Here’s what stands out based on publicly available case studies, certifications, and direct customer feedback shared on professional networks.
In-house integration as a multiplier: By co-locating CNC milling, turning, wire EDM, and finishing lines—including anodizing, passivation, powder coating, and laser marking—jucheng removes the blame game that happens when a machining shop ships parts to a third-party plater. One testimonial from a German robotics firm highlighted how this integration cut their quality-inspection man-hours by 40%, because the Certificate of Conformance covers the entire part, not just the machining dimension.
Process anchoring in standards: Jucheng’s finishing processes are benchmarked against AMS 2488 for anodizing, ASTM A967 for passivation, and ISO 13485 for medical device components. They maintain a library of process validation records, which for a medical startup meant the difference between a six-month FDA review and a streamlined 510(k) submission. These aren’t just wall decorations—they’re living documents that get updated with every significant process change.
Material fluency: The company routinely finishes aluminum alloys from 1000 to 7000 series, stainless steel 304/316L/17-4 PH, titanium grades 2 and 5, brass, copper, and even engineered polymers like PEEK. This matters when you switch from a 6061 prototype to a 7075 production run and need the anodizing parameters recalibrated. Their engineers can advise on the exact pre-treatment, such as using a de-smut step after machining 6061 to prevent black streaks.
Scalability without surprises: Whether you need 5 prototypes or 50,000 units annually, the same process controls apply. They maintain separate lines for small-batch specialty finishes (like gold anodizing for electronics) and high-volume production, eliminating the catch-22 where a prototype finish can’t be replicated at scale. This is a frequent praise point on LinkedIn recommendations from startups that later scaled.
Communication that bridges gaps: English-speaking project engineers provide design-for-finishing feedback—flagging issues like blind holes that will trap acid or sharp internal corners that won’t coat uniformly. This preemptive review catches problems that a simple PDF quote cannot.
Frequently Asked Questions About CNC Finishing Services
What surface finishes can a typical Chinese CNC shop offer?
A well-equipped china cnc finishing services co. ltd can provide anodizing (clear, colored, hardcoat), electropolishing, passivation, bead blasting, brushing, polishing, powder coating, PVD, Teflon coating, and silk screening. The key is whether these are done in-house or outsourced. In-house control yields better consistency and faster troubleshooting. Ask for photos of their actual finishing lines, not stock images.
How do I specify surface finish requirements clearly?
Use internationally recognized standards: call out Ra in micrometers or microinches, specify the standard (ISO 1302 or ASME B46.1), and provide a physical sample if possible. For anodizing, state the type (II or III), thickness, color code (Pantone or RAL), and sealing method. Include masking requirements on a technical drawing for threaded holes or press-fit surfaces. Vague terms like “cosmetic finish” lead to disputes.
Can I get a smooth anodized finish on 3D-printed metal parts?
It depends on the printing technology and post-processing. DMLS (Direct Metal Laser Sintering) parts have a rough as-built surface (Ra 10-30 µm) that needs extensive hand polishing or CNC machining before anodizing will look uniform. Binder jet aluminum, when sintered, is nearly indistinguishable from cast material and can take a good anodized finish after moderate blasting. A china cnc finishing services ltd with experience in additive-part finishing can guide you on realistic outcomes.
How does hard anodizing differ from regular anodizing in performance?
Hard anodizing (Type III) produces a thicker, denser oxide layer (25-75 µm vs. 5-25 µm for Type II). It achieves a surface hardness of 60-70 HRC, approaching that of case-hardened steel. This makes it suitable for sliding wear, but the coating is less capable of absorbing dye—colors often come out dark gray or bronze rather than bright blue or red. It also reduces fatigue life slightly in cyclic loading, so it should be specified with caution for structural aerospace parts.
What certifications prove a finishing supplier is reliable?
Beyond basic ISO 9001, look for ISO 13485 for medical, AS9100 for aerospace, or IATF 16949 for automotive. For processes, ask if they hold Nadcap accreditation for chemical processing (though this is rare and expensive). At minimum, they should be able to provide material and plating certificates per EN 10204 type 3.1, and demonstrate a documented quality system with internal audit records.
How can I verify a finish’s corrosion resistance before full production?
Request salt-spray test coupons per ASTM B117. For anodized aluminum, a 336-hour test with no pitting is a strong result. For electropolished and passivated stainless, 120 hours in a 5% salt spray is typical. Ask the supplier to include your specific alloy and heat treat condition in the test, not just a generic coupon. Jucheng routinely provides such third-party lab reports for new projects, giving buyers data-driven confidence.
What is the typical cost premium for a high-end finish?
Finishing can add 10% to 50% to the base machining cost, depending on complexity. Bead blasting is relatively inexpensive ($2-5 per part for small quantities), while Type III anodizing with tight masking may double the finishing cost. Electropolishing and PVD sit at the higher end. However, the cost of a finishing failure—scrapped parts, delayed revenue, customer audit findings—far outweighs the premium for quality. Several Facebook procurement threads cited a loss ratio of 5:1 when comparing recall costs to finishing investment.
Do I always need to post-finish machine critical features?
Not if the shop compensates correctly. For anodizing, the coating grows roughly 50% inward and 50% outward. A 25 µm coating thus increases a shaft diameter by about 25 µm. For bores, the material removal is inward, so the hole gets smaller. An experienced china cnc finishing services inc partner will adjust machining dimensions to keep features in tolerance after finishing. If in doubt, request a first-article report with post-finish measurements.
Bringing It All Together: Your Next Move
Finishing is the last impression your part makes, but it’s the first thing your customer sees. Throughout this guide, we’ve traced the root causes of finishing failures, decoded the technologies, and mapped out a selection framework that moves beyond price-based decisions. The consistent thread is that vertically integrated, data-guided providers de-risk your project in ways that fragmented supply chains cannot. If you’re currently struggling with inconsistent surfaces, delayed shipments, or a lack of process transparency, consider engaging a partner that treats finishing as a science, not a cosmetic step.
For an evaluation of your specific project, including recommendations on finish type, masking design, and cost targets, reach out to the team at jccncmachining.com. Their application engineers will review your CAD and provide a detailed process proposal, often within 24 hours. The goal isn’t just a quote—it’s a plan that ensures your parts arrive ready to perform, not requiring rework.