
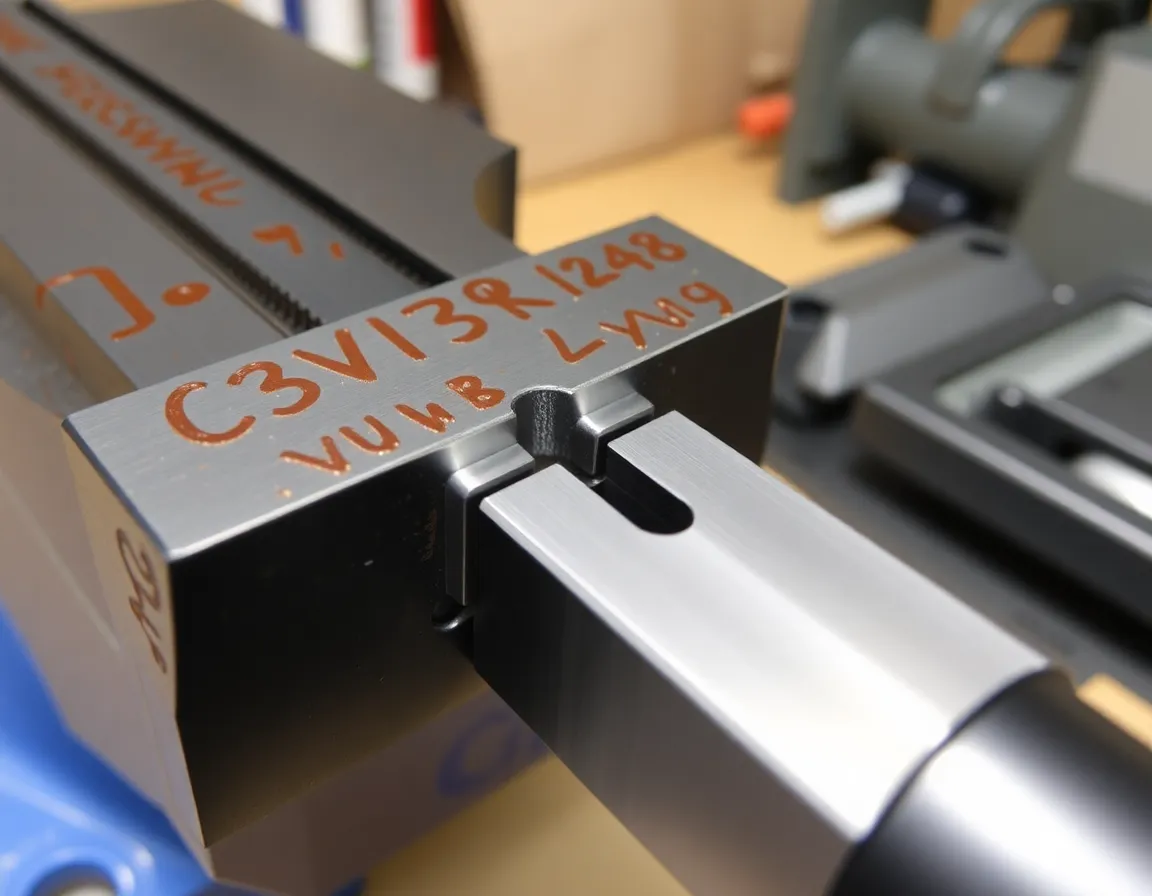
Every machinist knows the frustration of a workpiece that slips, shifts, or marrs under clamping pressure. The humble vise is the foundation of countless machining operations, yet the standard jaws that ship with most vises are often the weakest link in the setup. Machined vise jaws—precision-ground, custom-fit clamping surfaces—transform an ordinary vise into a high-performance workholding system. They bite better, hold tighter, and let you run faster with confidence. This article explores what machined vise jaws are, how they work, why they matter, and how to get the most from them.
What Are Machined Vise Jaws?
Machined vise jaws are replacement or upgrade jaw sets that have been precisely machined—typically from tool steel, mild steel, aluminum, or specialty alloys—to deliver accurate, repeatable clamping. Unlike the generic, often soft or roughly finished jaws that come standard with a vise, machined jaws are produced to tight tolerances on surface grinders, CNC mills, or lathes. They may be flat, stepped, grooved, V-notched, or custom-profiled to suit specific part geometries.
The term covers several categories:
- Soft jaws: Machined from aluminum or mild steel and custom-bored or profiled to match a specific workpiece. They sacrifice themselves to protect finished surfaces and can be re-machined as they wear.
- Hard jaws: Case-hardened or through-hardened steel jaws, often serrated or smooth-ground, designed for maximum grip and long service life.
- Precision-ground flat jaws: Ground square and parallel to within microns, ideal for accurate locating and squaring of parts.
- Specialty jaws: V-jaws for round stock, step jaws for thin parts, fixture jaws with dowel-pin locations, and jaws with machined pockets for irregular shapes.
What unites all of these is the emphasis on machined accuracy. Where a standard jaw might be parallel to within a few thousandths of an inch, a quality machined jaw set can hold parallelism and squareness to tenths.
How Machined Vise Jaws Work
The Geometry of Grip
A vise holds a part through friction and mechanical interlock. The jaw faces contact the workpiece, and the clamping screw converts torque into horizontal force. The effectiveness of that force depends heavily on jaw geometry. Serrated hard jaws bite into the surface, creating mechanical engagement that resists lateral and upward forces. Smooth machined jaws rely on high contact area and flatness to distribute clamping pressure evenly, minimizing distortion and marking.
Because machined jaws are square and parallel, the clamping force is applied uniformly across the part. This prevents the "cocking" or lifting that occurs when worn or poorly made jaws contact a workpiece unevenly—a common cause of parts jumping out of the vise during aggressive cuts.
Custom Fit and Locating Features
Machined jaws can be produced with steps, pockets, and profiles that match the workpiece exactly. When a jaw is machined in place on the vise—a technique known as boring or machining jaws "on the machine"—the jaw faces become true to the machine's own axes. This means the part is automatically aligned with spindle travel, eliminating the need for indicating each piece. Many machined jaws also incorporate dowel-pin holes or keys that locate them repeatably on the vise body, so they can be removed and reinstalled without losing position.
Material and Heat Treatment
The working life of a jaw depends on its material. Hard jaws are typically made from alloy steel, carburized, and hardened to 55–60 HRC, giving them excellent wear resistance and bite. Soft jaws are intentionally left machinable—usually aluminum or low-carbon steel—so they can be cut to fit and re-cut when worn. Some applications call for stainless steel jaws to resist corrosion, or brass and plastic jaws to protect delicate parts.
Why Machined Vise Jaws Matter: The Benefits
Superior Grip and Less Slippage
The most immediate benefit is better bite. Properly machined, sharp-serrated hard jaws dig into the workpiece and resist the cutting forces that try to push, twist, or lift it. With soft jaws machined to the part profile, the contact area increases dramatically, distributing load and preventing localized crushing. The result: fewer scrapped parts, fewer broken tools, and fewer setups interrupted to re-tighten a wandering workpiece.
Improved Accuracy and Repeatability
Because machined jaws are square, parallel, and often located by pins or keys, they establish a consistent datum. Every part loaded into the vise sits in the same position relative to the machine axes. For production runs, this repeatability is invaluable—it reduces indicating time, shortens setup, and makes in-process inspection more predictable. Job shops running small batches benefit just as much, since a trustworthy vise means one less variable to chase when tolerances tighten.
Protection of Finished Surfaces
Hard serrated jaws will mark a finished part. Machined soft jaws, bored or profiled to match the workpiece, grip without gouging. This makes them essential for second operations on turned parts, for holding polished or coated components, and for any workpiece where cosmetic damage is unacceptable.
Faster Setups and Cycle Times
This is the "work faster" half of the equation. Pre-machined jaws dedicated to a family of parts can be swapped in minutes. Repeatable locating features mean the operator loads a part, clamps, and presses cycle start—no indicating, no shimming, no tapping the part into alignment. On a machine running multiple jobs per shift, the time saved compounds quickly. Higher clamping confidence also allows more aggressive feeds and speeds, since the machinist knows the part will not move.
Versatility Across Applications
Machined jaws adapt to an enormous range of workholding challenges:
- Round stock: V-notched jaws center and grip shafts, tubes, and pins securely.
- Thin parts: Step jaws support thin plates so they cannot deflect or bow under clamping pressure.
- Irregular shapes: Custom-profiled soft jaws cradle castings, forgings, and machined components.
- High-volume production: Dedicated jaw sets with quick-change features minimize changeover time.
- Delicate materials: Aluminum, brass, or plastic jaws prevent crushing and scratching.
Applications in the Shop
Machined vise jaws appear wherever precision and productivity matter. In CNC milling, soft jaws machined in place are standard practice for second-operation work and for holding parts with critical flatness or parallelism requirements. In turning operations, jaws bored on the lathe itself ensure concentricity. Toolrooms rely on precision-ground flat jaws for squaring blocks and inspecting parts. Production environments use hardened serrated jaws for roughing and dedicated soft jaws for finishing.
Beyond metalworking, machined jaws serve in woodworking, plastics fabrication, welding fixtures, and inspection setups—anywhere a vise is used to hold a part that must not move or be damaged.
Best Practices for Using Machined Vise Jaws
Machine Jaws in Place When Accuracy Matters
For the highest precision, clamp the jaws in the vise and machine them on the machine that will run the job. This ensures the jaw faces are true to the spindle, compensating for any error in the vise body or mounting. Bore soft jaws at the diameter of the workpiece, or machine steps at the exact height required.
Match the Jaw to the Task
Use hard serrated jaws for roughing and heavy stock removal where grip is paramount. Switch to smooth or soft jaws for finishing, thin-wall parts, and finished surfaces. Do not ask one jaw set to do everything—dedicated jaws pay for themselves in consistency.
Keep Jaws Clean and Maintained
Chips trapped between the jaw and the workpiece cause misalignment and marking. Clean jaw faces and vise ways before every setup. Inspect serrations for wear and replace or re-machine jaws when they lose their bite. Store spare jaw sets protected from rust and damage.
Respect Clamping Limits
More force is not always better. Excess clamping pressure can distort thin parts, crush soft materials, and spring the vise itself. Use the minimum force that holds the part securely, and consider torque-limiting handles or pressure indicators for sensitive work.
Use Repeatable Locating Features
Whenever possible, specify jaws with dowel-pin locations or keys matched to the vise. This allows jaw sets to be swapped without re-machining and keeps setups repeatable across operators and shifts.
Conclusion
Machined vise jaws are a small investment with an outsized return. They grip harder, hold truer, and protect the parts you have already worked hard to produce. By choosing the right jaw material and geometry, machining jaws in place for critical work, and maintaining them properly, any shop can turn an ordinary vise into a precision workholding tool. The payoff is simple: better bite, faster work, and fewer surprises—exactly what every machinist wants from the foundation of the setup.