
For machined components, approval depends on a connected body of evidence: released design records, authorized changes, material and external-process documents, process flow, PFMEA, control plan, measurement-system evidence, dimensional results, capability data, and the Part Submission Warrant. The exact package follows customer requirements; “PPAP required” alone is not a complete RFQ instruction.
PPAP is a production-release argument
 AIAG defines PPAP as the industry standard used to ensure that engineering design records and specification requirements are consistently met during an actual production run at production rates. In practical CNC terms, the submission must connect four claims:
This places PPAP inside the wider family of CNC machining standards, but gives it a narrow role: customer approval of a defined production part and process. It is most associated with automotive supply chains, although some customers adapt the logic for other high-volume or risk-sensitive programs.
Why first article inspection cannot replace PPAP
 FAI and PPAP overlap in dimensional evidence but answer different release questions. A first article inspection checks whether a representative part conforms to the defined requirements. PPAP demonstrates that the entire production system has been planned and supported well enough for repeatable supply.
Use the detailed first article inspection guide when the immediate question is characteristic verification. Use PPAP when the buyer needs confidence in the continuing production system.
The CNC evidence chain—from drawing to control plan
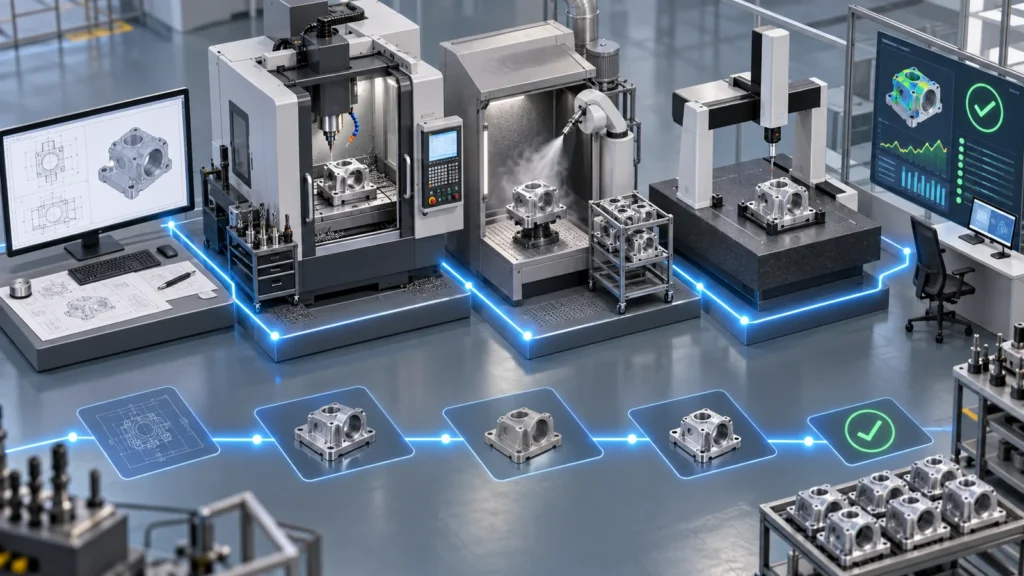 A strong PPAP package is internally consistent. The drawing identifies a critical bore. The process flow shows where it is rough-machined, heat-treated if applicable, finished, cleaned, and inspected. The PFMEA considers tool wear, thermal growth, fixture contamination, and distortion. The control plan assigns the gauge, frequency, reaction plan, and responsible operation. The dimensional and capability results then use that same definition.
When these documents are created independently, contradictions appear: a special characteristic is missing from the control plan, the capability study uses a different datum alignment, or the material certificate is not traceable to the production lot. Approval stalls because the evidence no longer supports one coherent process.
The AIAG’s official PPAP overview describes the purpose of demonstrating consistent conformity during an actual production run. Customer-specific requirements still govern the required forms, submission level, sample size, and acceptance thresholds.
What changes for a machined component
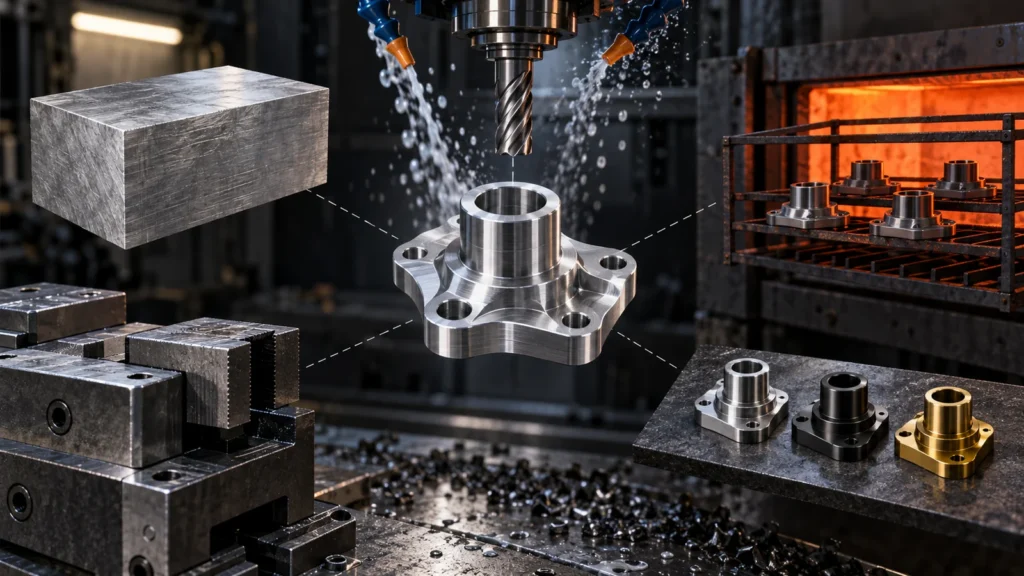 CNC production has variation mechanisms that generic PPAP checklists can hide. The submission should make the relevant ones visible:
For traceability design, see the guide to material and dimensional traceability. PPAP should identify the records retained for each relevant input and process, rather than attaching unrelated certificates in bulk.
Capability data must represent the process being approved
 A capability index is persuasive only when the data come from a stable, representative sequence. Sorting out bad parts before analysis, combining multiple cavities or fixture stations without identification, making unrecorded offset adjustments, or measuring every part after rework can produce a reassuring number that does not describe normal production.
Before calculating Cp, Cpk, Pp, or Ppk, define the characteristic, subgroup logic, production sequence, sample size, measurement method, distribution assumptions, and treatment of known adjustments. Plot the values in time order. A high index with a visible tool-wear slope may still need an offset or replacement rule.
The separate article on CNC process capability and Cpk explains how to interpret those studies. PPAP uses the evidence; it does not make weak data valid.
A buyer-ready PPAP request starts at RFQ
Late PPAP surprises create avoidable cost. Before quotation, the buyer should provide the current drawing and model, annual volume, expected production rate, special-characteristic definitions, submission level, customer-specific templates, capability requirements, approved material or process sources, packaging tests, labeling rules, and any portal workflow.
The supplier should return a feasibility review that identifies high-risk tolerances, inaccessible inspection features, destructive testing, purchased components, external processes, gauge lead time, capacity constraints, and evidence that cannot be produced from the proposed route. This review is where the control concept becomes real.
| Before machining | During trial run | Before submission |
|---|---|---|
| Freeze revision and requirements | Record actual production conditions | Reconcile every characteristic |
| Agree submission scope | Keep sequence and station identity | Close deviations and missing evidence |
| Complete feasibility and risk review | Apply the planned control plan | Verify PSW details match the package |
After approval, changes still need governance
 PPAP approval does not authorize unreported changes. A new material source, machine transfer, fixture revision, major toolpath change, external processor change, long production interruption, or engineering revision may trigger customer notification and partial or full resubmission. The customer-specific rules determine the threshold.
A practical change log records what changed, why, which product and process risks are affected, what validation was performed, and whether approval was required before shipment. This protects repeat orders from silently drifting away from the process originally approved.
Are all 18 PPAP elements always required?
No. The customer defines the submission level and which records are submitted or retained. Do not omit an element based only on a generic online checklist.
Can prototype parts be used for PPAP?
Only if the customer accepts them and they represent the intended production process. Prototype tooling or special handling may not prove production readiness.
Does PPAP approval guarantee zero defects?
No. It supports confidence that the defined process can meet requirements and has planned controls. Ongoing monitoring and reaction remain necessary.
Who signs the Part Submission Warrant?
The supplier’s authorized representative submits it according to customer rules, and the customer records the disposition. The signature does not replace the supporting evidence.
The useful PPAP package is not the thickest one. It is the package in which the drawing, risks, process, measurements, capability evidence, and continuing controls describe the same production reality.