قلب الطاقة الحديثة: شفرات توربينات مُشغَّلة
في السعي الدؤوب نحو الكفاءة والقدرة والموثوقية في قطاعات الفضاء والطاقة والصناعة، يقف التوربين كقمة للإنجاز الهندسي. في صميم كل توربين عالي الأداء—سواء كان يدفع طائرة عبر القارات أو يولد الكهرباء لمدينة—توجد مجموعة من المكونات حيث الكمال ليس طموحًا بل متطلبًا: الشفرات. وبينما توجد طرق تصنيع متنوعة، برز التشغيل الدقيق كعملية حاسمة، وغالبًا لا غنى عنها، لإنتاج شفرات توربينات تحقق أداءً ذرويًا في أقسى الظروف التي يمكن تصورها. يتعمق هذا المقال في عالم شفرات التوربينات المُشغَّلة، مستكشفًا العمليات المعقدة والفوائد التي لا مثيل لها والتطبيقات الحيوية التي تحدد هذا التخصص التصنيعي المتقدم.
تشريح مكوّن حاسم
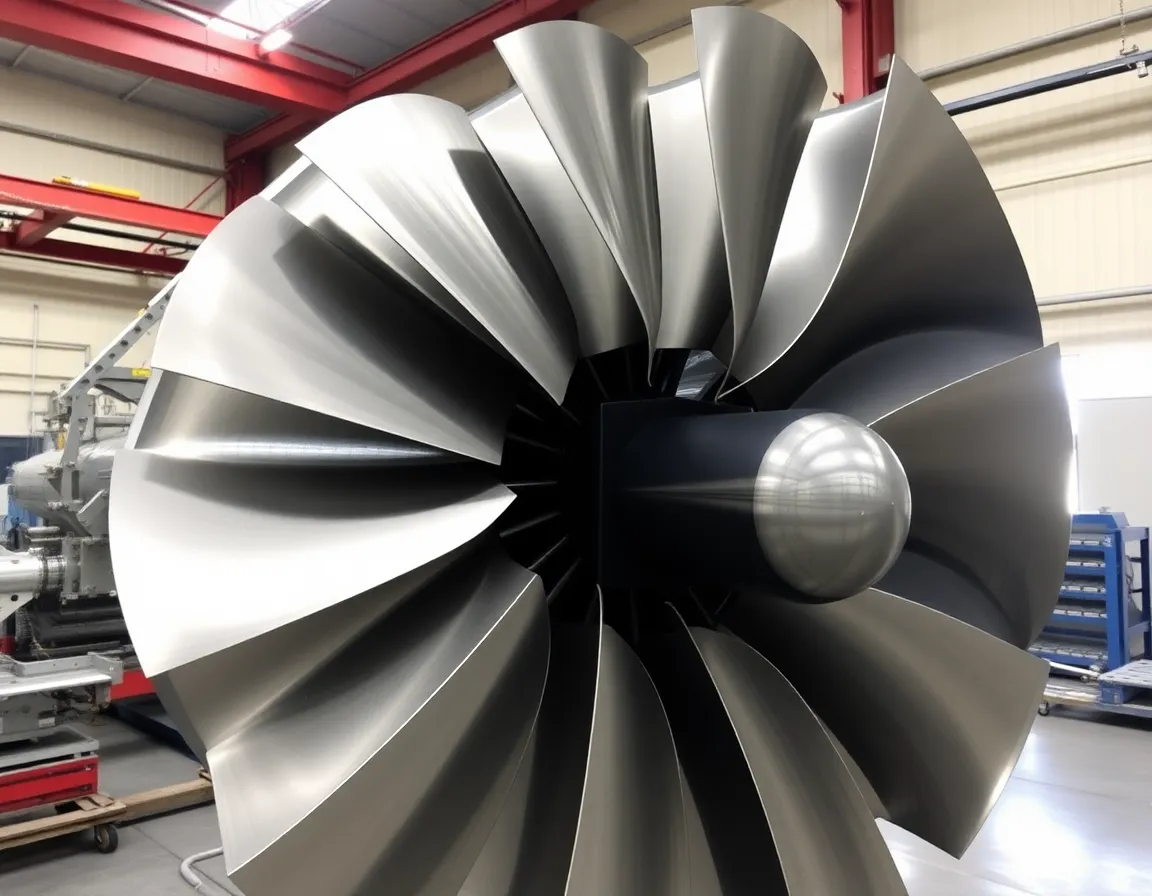
شفرة التوربين تحفة من التصميم الديناميكي الحراري والميكانيكي. وظيفتها الأساسية هي استخلاص الطاقة من مائع عالي الحرارة والضغط (غاز أو بخار) وتحويلها إلى حركة دورانية. للبقاء في هذه البيئة القاسية، يجب أن تجسد الشفرات مجموعة معقدة من الخصائص المتناقضة: يجب أن تكون قوية للغاية ومع ذلك خفيفة الوزن، ومقاومة للحرارة الشديدة والتآكل، ومثالية ديناميكيًا هوائيًا. غالبًا ما تتميز بقنوات تبريد داخلية معقدة، ومحيطات جنيح معقدة، ووصلات جذر فائقة الأمان. هنا يتمايز التشغيل الدقيق، وخاصة التشغيل باستخدام CNC (التحكم الرقمي بالحاسوب) بخمسة محاور، عن الصب وتقنيات التشكيل الأخرى.
من الكتلة إلى الشفرة: عملية التشغيل
تبدأ رحلة شفرة التوربين المُشغَّلة عادةً بكتلة صلبة من سبيكة عالية الأداء، مثل سبيكة فائقة أساسها النيكل مثل Inconel أو سبيكة تيتانيوم. تُختار هذه المواد لقوتها في درجات الحرارة المرتفعة لكنها صعبة التشغيل بشكل ملحوظ. العملية سيمفونية من التصميم الرقمي والدقة الميكانيكية:
- Digital Blueprinting & CAM Programming: The blade's 3D CAD model is translated into machine instructions (G-code) using CAM software. This program dictates every movement of the cutting tool, often involving millions of lines of code to define the complex geometry.
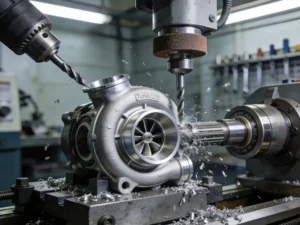
- 5-Axis CNC Machining: The billet is mounted on a 5-axis machining center. Unlike 3-axis machines, 5-axis machines can rotate the workpiece and tilt the cutting tool simultaneously. This allows the tool to approach the material from virtually any angle, enabling the creation of the blade's twisted airfoil shape, precise leading and trailing edges, and the platform and root features in a single, coherent setup.
- Creating Internal Complexity: For blades requiring internal cooling channels, techniques like plunge EDM (Electrical Discharge Machining) or deep-hole drilling are employed. EDM uses electrical sparks to erode material, allowing for the creation of complex, non-linear internal passages that would be impossible with traditional drilling.
- Finishing & Surface Enhancement: After roughing and finishing cuts, blades undergo critical finishing processes. This includes precision grinding for tighter tolerances, abrasive flow machining to polish internal channels, and often shot peening to induce beneficial compressive stresses on the surface, enhancing fatigue life.
Why Machine? The Compelling Advantages
Choosing machining over investment casting or forging for turbine blades is a decision driven by uncompromising demands for performance, flexibility, and quality.
Unmatched Geometric Freedom and Precision
5-axis CNC machining offers designers unparalleled freedom. It can produce blades with more aerodynamically efficient, complex contours, sharper leading edges for reduced drag, and more intricate root forms like fir-tree or dovetail designs that ensure perfect load distribution within the disk. Tolerances are held to astonishing levels, often within microns, ensuring each blade is a perfect match for its neighbors, critical for balance and vibration control.
Superior Material Integrity
While casting can introduce defects like porosity or grain boundary weaknesses, machining starts with a wrought billet known for its homogeneous, fine-grained structure. This results in blades with superior mechanical properties, including higher fatigue strength, better fracture toughness, and more consistent performance across an entire batch. The absence of casting-related defects is a significant reliability advantage.
Flexibility for Prototyping and High-Mix Production
Machining is ideal for prototyping new blade designs. Changes can be made in the CAD model and implemented immediately without the need for expensive and time-consuming new mold or die creation. This accelerates R&D cycles dramatically. Furthermore, for applications like industrial gas turbines or specialized aerospace projects where volumes may be lower but customization is high, machining provides an economically viable route to production without sacrificing quality.
Enhanced Surface Finish and Feature Integration
The surface finish of a machined blade is typically superior to an as-cast surface. A smoother finish reduces aerodynamic losses and provides a better substrate for thermal barrier coatings (TBCs). Additionally, features like inspection holes, instrumentation ports, and specific balancing pads can be integrated directly into the machining program with high precision.
Applications: Where Machined Blades Dominate
The use of machined turbine blades spans industries where failure is not an option and efficiency gains are measured in millions of dollars.
- Aerospace Jet Engines: While high-pressure turbine blades in the hottest section are often single-crystal castings, many other critical rotating and static blades within the compressor and turbine sections—especially in military, business jet, and advanced commercial engines—are precision machined. Their strength and reliability are paramount.
- Industrial Gas Turbines (IGTs) for Power Generation: IGTs value longevity and maintainability. Machined blades, with their superior material integrity, offer extended service intervals and reduced risk of unplanned outages. They are common in earlier stages of the turbine where temperatures are slightly lower but durability is key.
- Oil & Gas Turbo-Expanders and Compressors: In pipelines and processing plants, turbines operate continuously for years. Machined blades provide the robustness needed for such duty cycles, handling a variety of process gases reliably.
- Marine Propulsion: Naval vessels and high-performance ships use gas turbines for propulsion. The salty, corrosive environment demands components with excellent fatigue and stress-corrosion cracking resistance, a hallmark of machined components from high-quality alloys.
- High-Performance Racing Turbochargers: The tiny, ultra-high-speed turbines in racing turbochargers push materials and manufacturing to the limit. CNC machining is often the only method capable of producing the necessary shapes and tolerances from the strongest materials for these applications.
Best Practices and Future Horizons
Producing a world-class machined turbine blade is not merely about having a 5-axis machine. It is an ecosystem of excellence.
Best Practices in the Machining Cell
- Advanced Tooling: Utilizing polycrystalline diamond (PCD) or cubic boron nitride (CBN) tools to cut abrasive superalloys, and implementing sophisticated tool wear monitoring systems.
- Rigorous Workholding: Designing custom fixtures that provide absolute stability and precise location for the workpiece throughout the aggressive machining process.
- In-Process Metrology: Integrating touch probes and laser scanners on the machine tool to measure critical features mid-process, allowing for automatic compensation and ensuring the part is "right the first time."
- الإدارة الحرارية: Controlling the temperature of the workpiece, tool, and machine environment is critical to maintaining dimensional stability when working with heat-resistant alloys.
The Future: Hybrid Manufacturing and Digital Twins
The frontier of turbine blade manufacturing lies in hybridization. Additive manufacturing (3D printing) is increasingly used to build up near-net-shape blade forms, complete with internal channels, which are then finish-machined to achieve the final, high-precision surfaces and edges. This combines the geometric freedom of additive with the surface quality and accuracy of machining. Furthermore, the concept of the digital twin—a virtual replica of the machining process—allows for simulation and optimization of every cut, predicting and preventing potential errors before metal is ever touched, pushing quality and efficiency to new heights.
Conclusion
Precision machining for turbine blades represents the intersection of advanced materials science, digital manufacturing, and uncompromising engineering. It is a process born from the need to conquer extremes—of temperature, pressure, and force. By transforming solid billets of cutting-edge alloys into aerodynamic wonders with microscopic accuracy, machining provides the performance, reliability, and flexibility that modern turbine technology demands. As the push for greater efficiency and lower emissions continues to intensify across aviation and energy sectors, the role of the exquisitely machined turbine blade will only become more central, literally and figuratively driving innovation forward.