
Anodizing and powder coating can both protect and color aluminum, but they solve different product problems. Anodizing converts the aluminum surface and preserves a metallic character; powder coating adds a polymer film with broader color and texture freedom. The right choice depends on wear, corrosion exposure, electrical contact, edge coverage, geometry, dimensional allowance, appearance, repair expectations, and production consistency—not on which finish sounds more premium.
The 60-Second Finish Decision
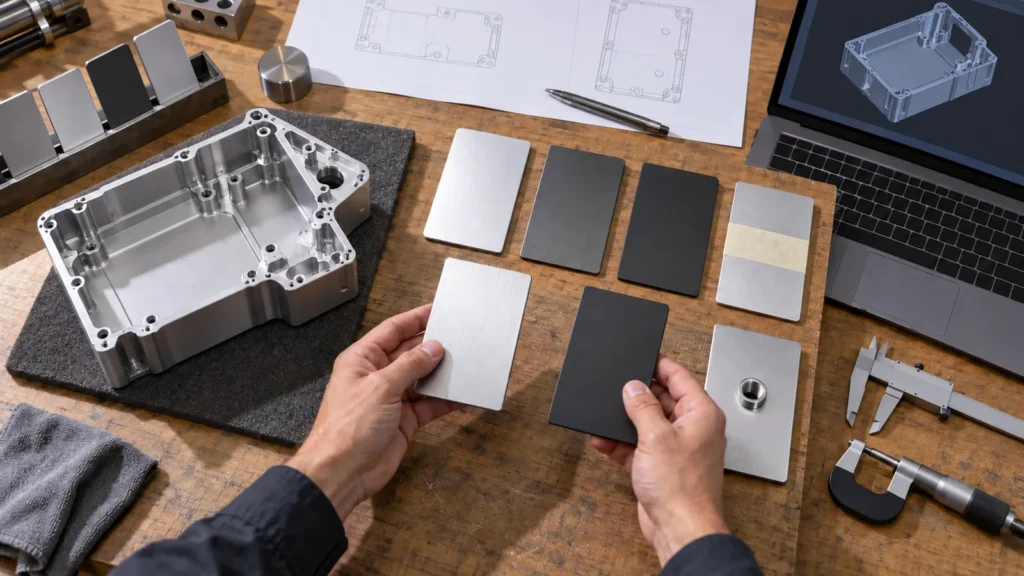
The scorecard also exposes an important purchasing mistake: comparing generic process names instead of complete specifications. “Black anodize” can refer to different preparation, treatment, sealing, and visual expectations. “Black powder coat” can vary in chemistry, gloss, texture, film target, and pretreatment. Quote comparisons are meaningful only when suppliers are pricing the same finished condition.
A mixed-material assembly adds another layer. Fasteners, inserts, adhesives, gaskets, heat sinks, and grounding hardware may respond differently to the selected finish. Review galvanic contact, cure temperature, masked interfaces, bonding surfaces, and assembly sequence before releasing the coating note.
This is a screening tool, not a substitute for the drawing. The finish must still match the alloy, service conditions, cosmetic target, and acceptance plan. For a wider view of available treatments, begin with the CNC machining surface finishes guide.
One Changes the Surface; One Covers It
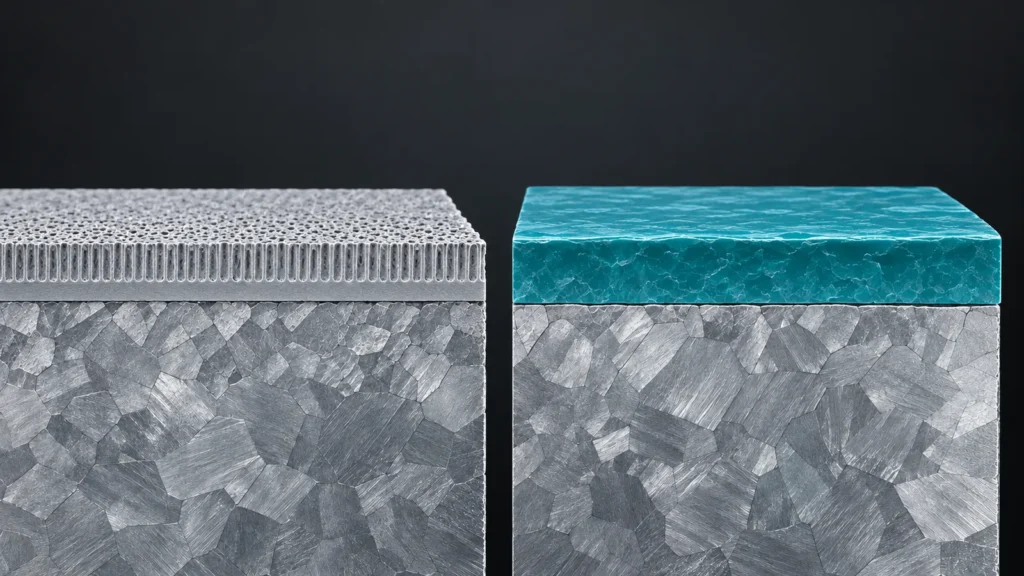
Powder coating applies charged powder and cures it into a continuous organic film. The film can hide some minor visual variation and create opaque colors, gloss levels, and textures. It also creates more obvious thickness buildup, which matters at threaded features, bores, mating edges, engraved details, and close-clearance assemblies.
Do not ask only, “Which finish is more durable?” Ask, “Which failure are we preventing—corrosion, abrasion, fading, chipping, poor adhesion, electrical isolation, or cosmetic inconsistency?”
Anodizing vs Powder Coating: Engineering Scorecard
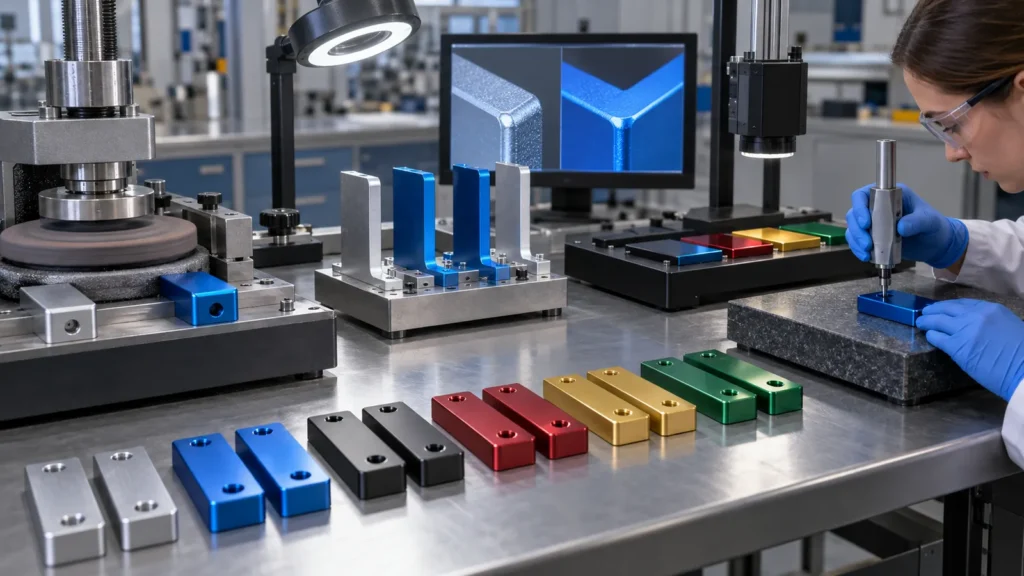
Geometry Can Overrule the Color Choice
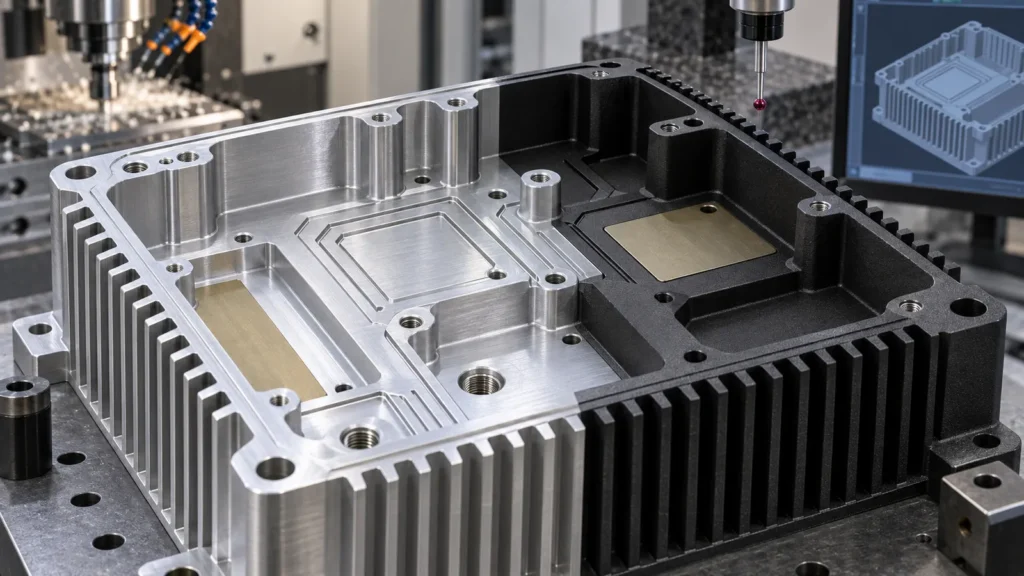
Thermal management deserves special attention. A housing may need bare contact pads under a heat-generating component, while the visible exterior receives a colored finish. Masking creates boundaries, and those boundaries need positional tolerance when they approach seals, fasteners, conductive paths, or visible edges. Put the boundary on the drawing rather than leaving it to shop interpretation.
Where anodizing needs attention
- Color can respond differently to alloy, temper, welds, cast features, and surface preparation.
- Electrical contact points, threaded interfaces, and critical fits may need masking.
- Machined and blasted zones can absorb light differently even when processed together.
- Racking locations should be agreed where cosmetic surfaces are tightly controlled.
Where powder coating needs attention
- Coating buildup can interfere with hardware, bores, hinges, sliding features, and edge fits.
- Recesses and internal corners may receive less uniform deposition.
- Sharp edges can be harder to cover consistently than broad faces.
- Fine text, knurling, and small drainage features can lose definition.
JUCHENG’s pages for anodizing machined parts and powder coating CNC parts provide process-specific context. Use them to identify questions, then place the project’s actual masking and acceptance requirements on the RFQ.
Control Appearance with Zones, Not Adjectives
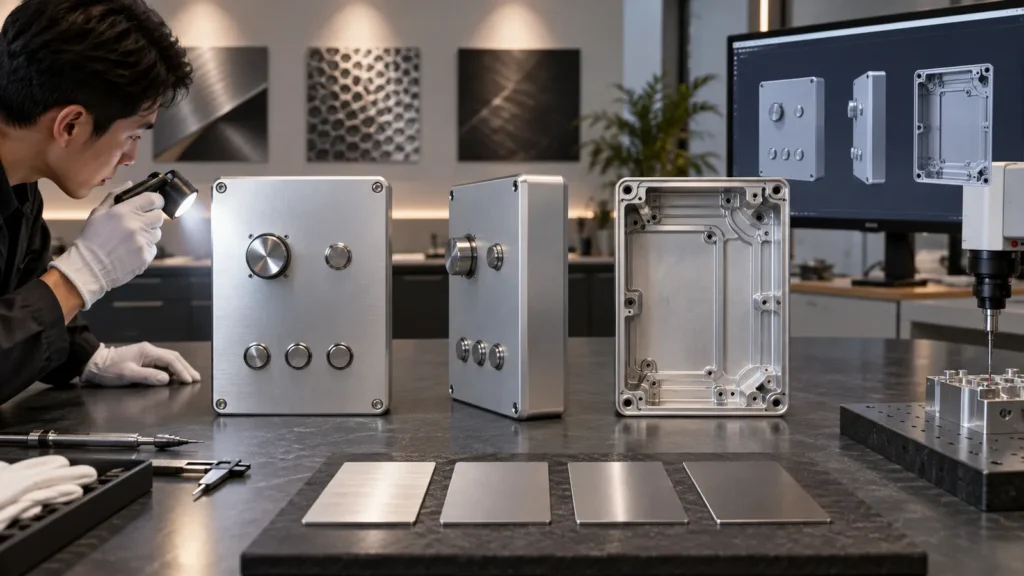
For color-sensitive programs, define the color reference, gloss or texture target, viewing distance, lighting, and whether an approved physical sample controls production. Also decide whether parts from different lots must match one another or only match the reference within an agreed tolerance. Alloy and pretreatment consistency are especially important when anodized components sit side by side.
Good cosmetic input
Marked zones, approved sample, color reference, gloss or texture expectation, viewing conditions, and defect limits.
Risky cosmetic input
A website image, a generic color name, “no variation,” or a finish request without identifying the base alloy and preparation.
Prototype Success Does Not Guarantee Batch Consistency
- Freeze the base material, alloy condition, and visible preparation process.
- Confirm the drawing identifies masking and dimensions that apply after finishing.
- Approve a representative sample on production-intent geometry when appearance is critical.
- Define inspection by zone: color, gloss, texture, coverage, adhesion, damage, and dimensions.
- Specify packaging that prevents part-to-part rubbing on visible faces.
- Record any approved deviation so later lots are judged by the same standard.
A documented control plan is particularly useful when several finish characteristics interact. Review the site’s quality management and inspection information when your RFQ requires reports, samples, or defined acceptance records.
Packaging belongs in that control plan. Powder-coated parts can chip or rub at corners; anodized faces can show scratches, pressure marks, or color contrast where components contact each other. Separators, protective film, clean gloves, and orientation during transport can determine whether an otherwise conforming finish reaches assembly in acceptable condition.
Build a Finish Brief the Supplier Can Quote
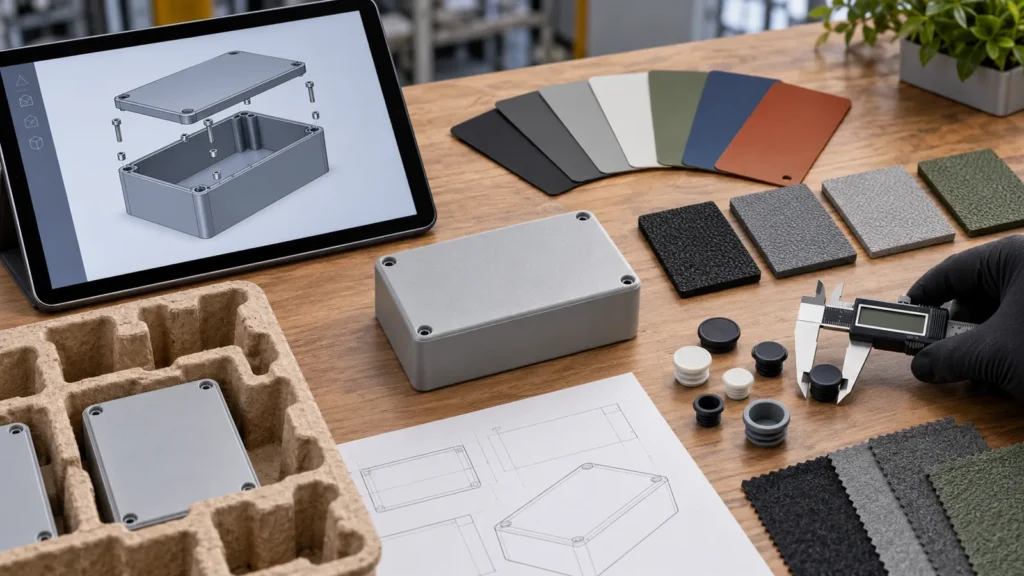
The supplier can then compare routes against the actual part: anodizing for an integrated metallic surface, powder coating for an opaque protective film, or a different treatment if neither matches the exposure and interface requirements. That decision is more reliable than choosing from a finish chart without the model.
Four Practical Questions Before Release
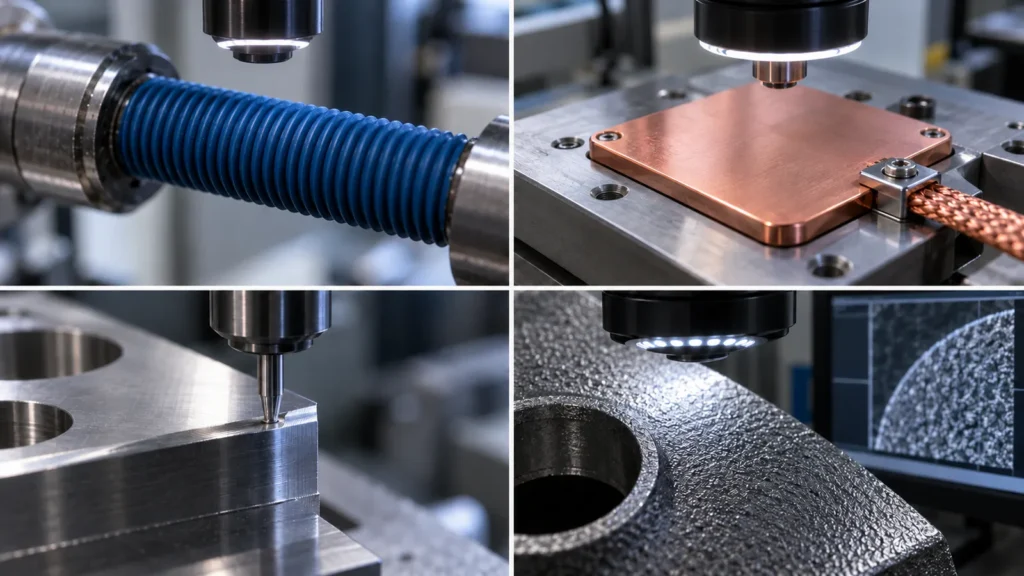
Neither is universally better. Thread class, engagement, electrical contact, corrosion exposure, coating buildup, and masking determine the answer. Identify whether the thread must remain bare, be chased after processing, or be sized for the finished condition.
Can powder coating hide machining marks?
It can reduce the visual prominence of minor variation, especially with textured films, but it will not reliably hide deep tool marks, dents, burrs, contamination, or poor edge preparation. The substrate still needs an agreed pre-coating condition.
Can anodizing and powder coating use the same color standard?
They can target a similar visual family, but the processes interact with light differently. Anodized color retains a metallic substrate influence; powder is an opaque film. Approve process-specific samples rather than assuming one color chip will look identical on both.
Which one is cheaper?
Total cost depends on type, color, quantity, part size, masking, surface preparation, inspection, rejection risk, and packaging. A lower finishing price can be offset by more machining allowance or assembly rework. Compare the complete production route.