The Allure and Challenge of Titanium
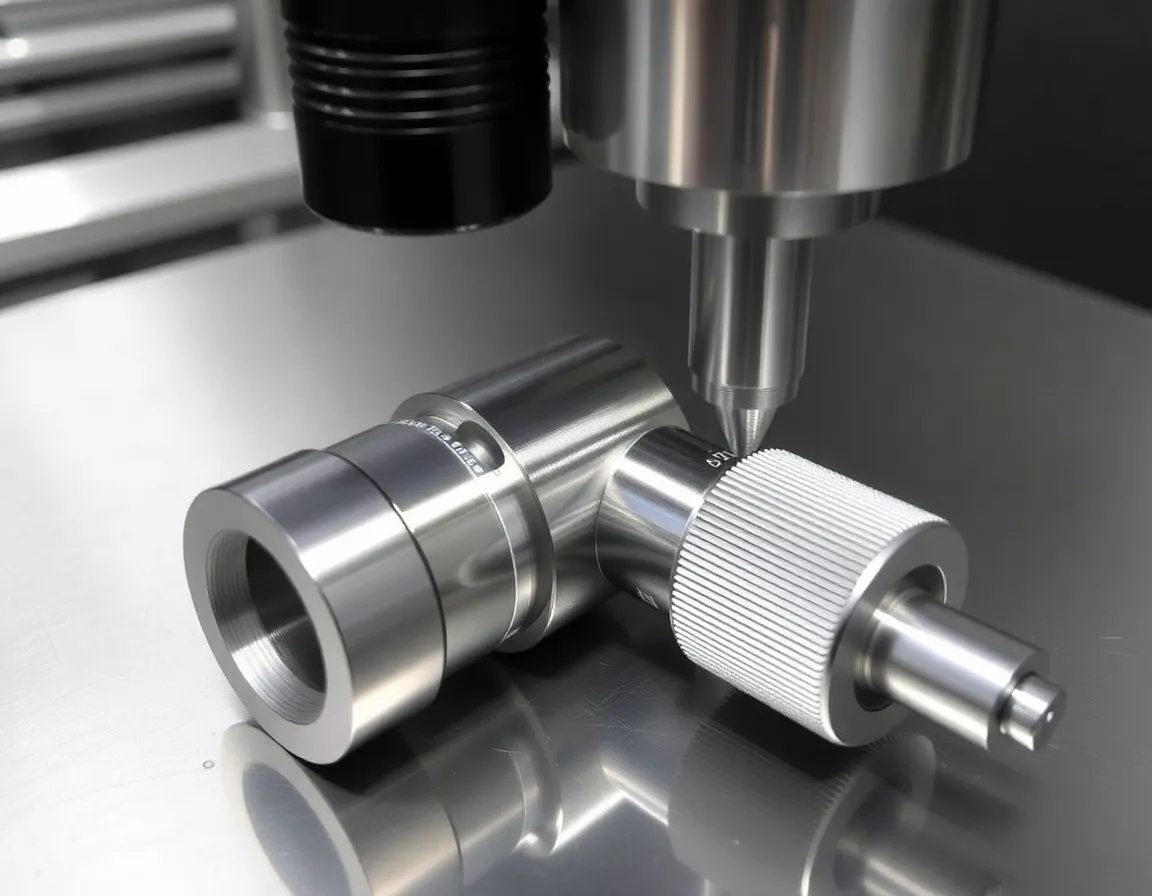
Titanium stands as a titan among metals in the manufacturing world, revered for its exceptional strength-to-weight ratio, outstanding corrosion resistance, and biocompatibility. These properties make it the material of choice for aerospace components, medical implants, high-performance automotive parts, and critical defense applications. However, these very same properties that make titanium so desirable also render it notoriously difficult to machine. Its low thermal conductivity causes heat to concentrate at the cutting edge, its high chemical reactivity can lead to galling and work hardening, and its strength resists easy deformation. Mastering Titanium CNC machining is therefore not just a skill but a strategic discipline, blending advanced technology with refined technique to unlock the metal's full potential.
Understanding the Titanium Machining Paradigm
Successful titanium machining requires a fundamental shift in mindset from machining more common materials like aluminum or mild steel. It is a process governed by managing forces, heat, and tool engagement with extreme precision. The core principle is maintaining a consistent, controlled chip load and managing heat evacuation. Unlike with aluminum, where high speeds and feeds are typical, titanium demands a more calculated approach where parameters are finely balanced to prevent tool failure and ensure part integrity.
Key Material Characteristics Affecting Machining
Baixa Condutividade Térmica: Titanium conducts heat poorly, approximately 1/16th as effectively as aluminum. This means the heat generated during cutting doesn't flow into the chips or the workpiece efficiently; instead, it concentrates intensely at the cutting tool's edge. This can rapidly degrade even the most robust carbide tools.
High Strength at Elevated Temperatures: Titanium retains much of its strength even when hot. While steel softens as it heats up, titanium remains hard, continuously challenging the cutting tool.
Chemical Reactivity and Galling: At cutting temperatures, titanium tends to chemically react with tool materials, leading to adhesion and built-up edge (BUE). This can cause edge chipping, poor surface finish, and eventual catastrophic tool failure.
Elastic Modulus: Titanium has a relatively low modulus of elasticity, meaning it is "springy." This can lead to part deflection under cutting forces, challenging the achievement of tight tolerances and requiring robust workholding and strategic tool paths.
Strategic Best Practices for Success
Overcoming titanium's challenges is achieved through a holistic strategy encompassing tooling, machine tool rigidity, cutting parameters, and coolant application. There is no single silver bullet; success lies in the synergy of all these elements.
Tooling: The First Line of Defense
Selecting the right cutting tool is non-negotiable. Carbide grades with high hot hardness and wear resistance, such as micro-grain or sub-micron grades with PVD (Physical Vapor Deposition) coatings like AlTiN (Aluminum Titanium Nitride) or TiAlN, are standard. Geometry is equally critical:
- Sharp, Positive Rake Angles: Reduce cutting forces and heat generation.
- Área de contato reduzida: Tools with variable helix and pitch designs disrupt harmonic vibration (chatter) and reduce cutting pressure.
- Generous Flute Counts and Chip Gullets: Ensure efficient chip evacuation, as recutting chips is a primary cause of tool failure in titanium.
- Rigorous Inspection and Maintenance: Use tools at the first sign of wear. Waiting too long leads to rapid failure and potential damage to the expensive workpiece.
Machine Tool and Workholding: The Foundation of Rigidity
A machine tool for titanium must be a bastion of stability. Vibration and deflection are the enemies of tool life and surface finish.
- High Static and Dynamic Rigidity: Look for machines with massive, polymer-concrete bases, large diameter ball screws, and box-way constructions.
- Spindle Power and Torque at Lower RPMs: Titanium is machined at lower surface speeds, so high torque in the mid-RPM range is more valuable than ultra-high spindle speeds.
- Uncompromising Workholding: Use hydraulic or shrink-fit tool holders for maximum grip and concentricity. The workpiece must be clamped with exceptional rigidity, often using custom fixtures to minimize overhang and support thin walls.
Cutting Parameters: The Delicate Balance
The classic rule for titanium is "Run slow and feed hard." This counter-intuitive approach helps manage heat.
- Surface Speed (SFM): Conservative speeds are key. For roughing, speeds may range from 60-120 SFM, finishing slightly higher, but always within tool manufacturer recommendations.
- Feed Rate (IPT): Maintain a consistent, adequate chip load. Never let the tool rub. A rubbing tool generates maximum heat with minimal material removal, guaranteeing failure. Higher feed rates per tooth help carry heat away in the chip.
- Profundidade de Corte (DOC): Use radial depths of cut less than the tool radius (e.g., 30-40% of tool diameter) and axial depths that are stable. Trochoidal or peel milling strategies are highly effective for maintaining constant tool engagement and managing heat.
Coolant: The Essential Heat Management System
Coolant is not just a lubricant in titanium machining; it is a critical heat evacuation system. High-pressure, through-tool coolant (at least 1,000 PSI) is strongly recommended.
- Heat Evacuation: The pressurized stream penetrates the cutting zone, cools the tool edge, and helps break chips.
- Evacuação de Cavacos: It flushes chips away from the cut, preventing recutting.
- Flood Coolant: Even without high pressure, a generous flood of coolant directed precisely at the cut is mandatory. Many opt for oil-based or specialized synthetic coolants formulated for difficult-to-machine alloys.
Advanced Techniques and Application-Specific Considerations
Beyond the fundamentals, mastering titanium often involves leveraging advanced CNC capabilities and tailoring the approach to the final application.
Toolpath Optimization and CAM Strategies
Modern CAM software is a powerful ally. Use adaptive clearing or high-efficiency milling toolpaths that maintain a constant tool engagement angle, preventing thermal shock and shock loading on the tool. This results in smoother, cooler cuts and dramatically extended tool life. For finishing, consider slower, consistent speeds and lighter depths of cut to achieve the required surface integrity, which is especially critical for fatigue-prone aerospace parts.
Application-Driven Focus
Aeroespacial: The focus is on structural integrity, fatigue life, and extreme reliability. Machining-induced residual stresses and surface defects are unacceptable. Processes like low-stress milling and meticulous post-machining inspections (e.g., etch inspection, FPI) are common.
Medical Implants: Here, the focus shifts to exceptional surface finish, absolute cleanliness, and maintaining the biocompatibility of the material. Machining must avoid any contamination (like iron particles). Processes are often validated and performed in controlled environments, with extensive use of EDM and grinding in addition to CNC milling.
Racing and Automotive: While performance is key, cost and cycle time pressures are higher. This often involves pushing parameters closer to the edge while relying on the core principles of rigidity and tool management.
Conclusion: The Path to Mastery
Mastering titanium CNC machining is a continuous journey of precision, patience, and process optimization. It demands respect for the material's characteristics and a willingness to invest in the right technology and tooling. Success is measured not only in the flawless completion of a complex component but in the consistency of tool life, the predictability of the process, and the integrity of the final part. By adhering to the principles of rigidity, sharp tooling, controlled parameters, and aggressive heat/chip management, manufacturers can transform the formidable challenge of titanium into a reliable, profitable, and highly capable manufacturing process, unlocking the potential to build the most advanced and demanding products in the world.